
1. Product Overview
Guar Gum Food Grade is a natural, plant-derived hydrocolloid obtained from guar beans and widely used as an effective thickening, stabilizing, emulsifying, and viscosity-control agent. It is primarily used across food and beverage manufacturing to improve texture, consistency, moisture retention, and product stability. Its high functionality at relatively low usage levels provides manufacturers with an efficient solution for formulation optimization and process control. As a versatile food-grade ingredient with broad industrial applicability, guar gum remains strategically important for large-scale food processing and ingredient sourcing.
2. Key Specifications & Technical Characteristics
- Product: Guar Gum Food Grade
- Origin: Derived from guar bean endosperm
- Composition: Predominantly galactomannan polysaccharides
- Grade: Food Grade
- Function: Thickener, stabilizer, binder, emulsifier, and viscosity modifier
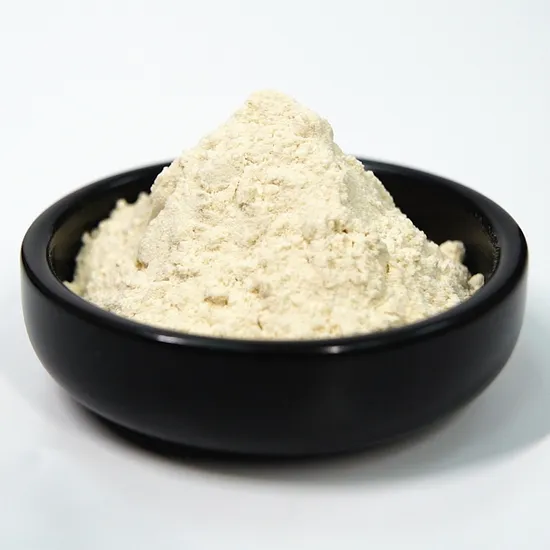
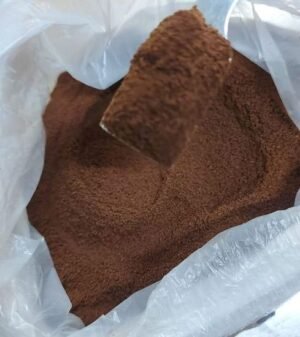
- Physical Form: Fine powder
- Appearance: White to off-white or cream-colored powder
- Solubility: Disperses and hydrates in water to provide viscosity
- Purity: Food-grade specification suitable for commercial food processing
- Particle Size: Available according to buyer or application requirements
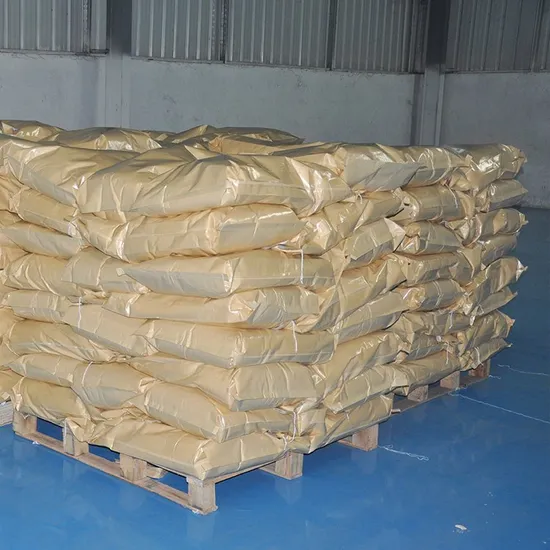
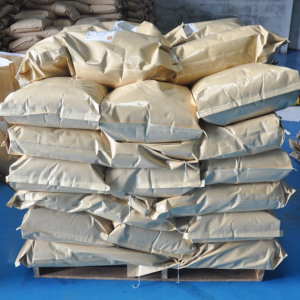
- Packaging: Standard 25kg bags; bulk packaging may be available upon request
- Shelf Life: Typically up to 24 months when stored in sealed packaging under cool, dry conditions
- Storage: Protect from moisture, direct sunlight, heat, and contamination
3. Core Industrial Applications
Guar Gum Food Grade is widely used in food and beverage manufacturing, including sauces, dressings, dairy products, ice cream, bakery products, beverages, processed foods, and gluten-free formulations. It helps increase viscosity, improve mouthfeel, stabilize emulsions and suspensions, control moisture migration, and maintain consistent product texture during processing and storage. In bakery applications, it can support dough structure and moisture retention, while in dairy and frozen products it helps improve body and stability. Its strong thickening performance at low concentrations can support formulation efficiency and help manufacturers achieve consistent product quality.
4. Competitive Advantages
- Consistent Quality: Suitable for standardized industrial formulations requiring reliable viscosity and functional performance.
- High Functional Efficiency: Provides effective thickening and stabilization at relatively low application levels.
- Supply Reliability: Available in commercial 25kg packaging with bulk procurement options for larger industrial requirements.
- Logistics Capability: Packaging and bulk supply formats support international B2B distribution and containerized shipments.
- Price Competitiveness: Efficient functionality can contribute to cost-effective formulation and production.
- Natural Origin: Plant-derived hydrocolloid suitable for manufacturers seeking naturally sourced functional ingredients.
- Technical Documentation: Product specifications, quality documentation, and relevant compliance information can be provided according to buyer requirements.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Approximately 20–22 MT per 20ft container, subject to packaging configuration, container payload limits, and destination requirements
- Standard Packaging: 25kg bags
- Supply Format: Bulk B2B commercial supply
- Shipping: International export and containerized logistics available
Reviews
There are no reviews yet.