
1. Product Overview
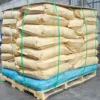
Lactose Monohydrate Food Grade is a high-purity crystalline carbohydrate derived from milk, supplied in convenient 25kg bags for food and industrial processing applications. It is widely used as a functional ingredient, carrier, bulking agent, and processing aid across food, beverage, confectionery, and pharmaceutical manufacturing. Its consistent quality, excellent solubility, and reliable handling characteristics support efficient formulation and large-scale production. As a globally traded food ingredient, it provides manufacturers with a dependable solution for formulation consistency and cost-effective bulk sourcing.
2. Key Specifications & Technical Characteristics
- Chemical Composition: Lactose monohydrate, C₁₂H₂₂O₁₁·H₂O
- Grade: Food Grade
- Purity: High-purity lactose suitable for food-processing applications; specification subject to supplier Certificate of Analysis (COA)
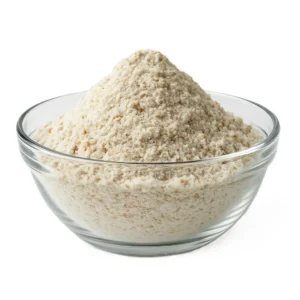
- Physical Form: Fine crystalline powder
- Color: White to off-white
- Taste/Odor: Mildly sweet, characteristic, and free from objectionable odors
- Solubility: Soluble in water, with performance dependent on temperature and particle characteristics
- Moisture: Controlled to food-grade specification
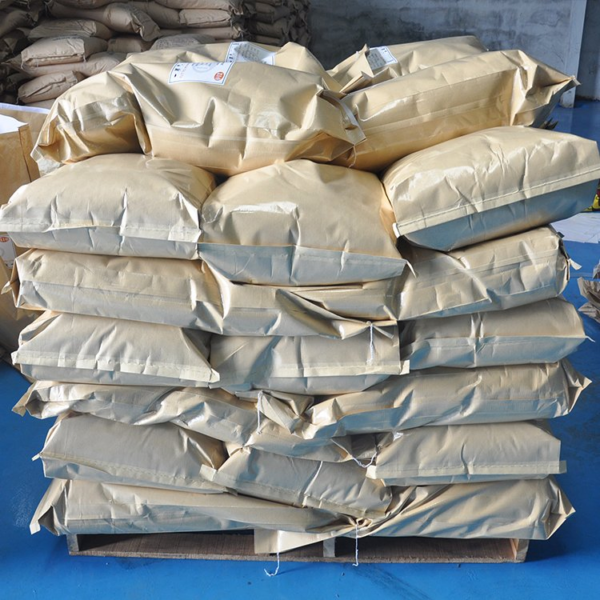
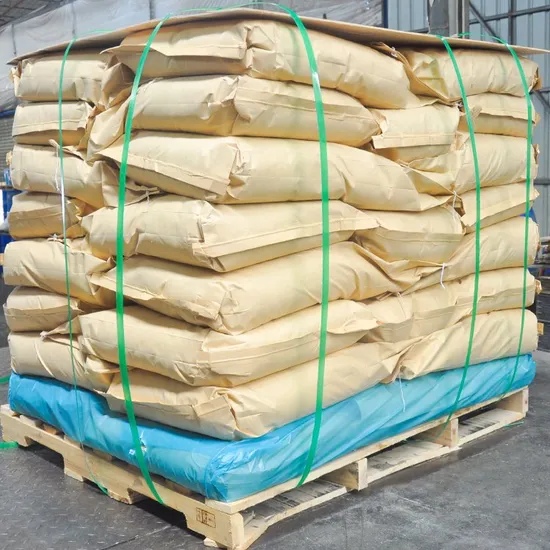
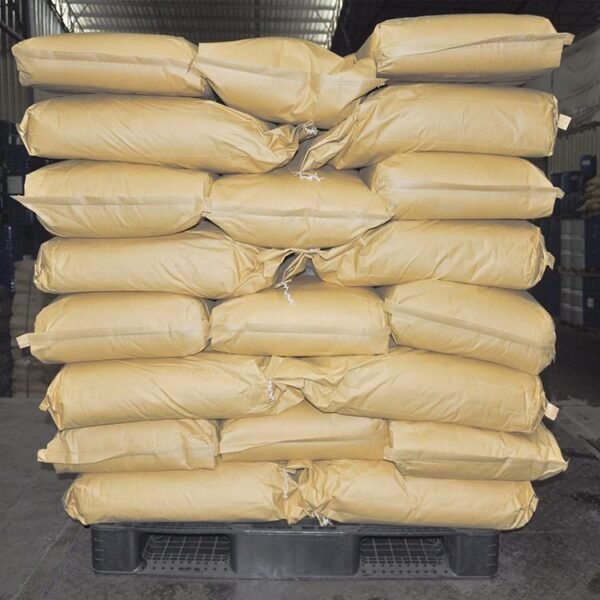
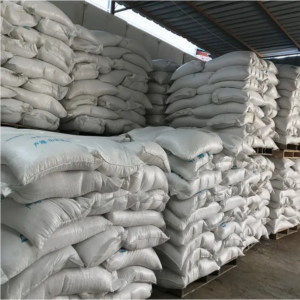
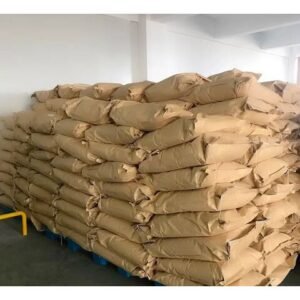
- Packaging: 25kg food-grade bags; bulk packaging available subject to commercial requirements
- Shelf Life: Typically 24 months when stored in a cool, dry environment in sealed original packaging, subject to manufacturer specification
- Storage: Protect from moisture, heat, contamination, and direct sunlight
3. Core Industrial Applications
- Food & Beverage Manufacturing: Used as a carbohydrate source, bulking agent, carrier, and formulation ingredient in processed foods and beverages.
- Confectionery: Supports controlled sweetness, texture, solids content, and formulation consistency.
- Bakery & Dairy Products: Used in selected formulations to improve solids balance, texture, and processing performance.
- Pharmaceutical Manufacturing: Used as an excipient and carrier in tablet and powder formulations where suitable pharmaceutical specifications are required.
- Nutritional Products: Applied in selected nutritional and powdered formulations as a carbohydrate and functional ingredient.
- Industrial Processing: Its consistent crystalline structure and predictable handling characteristics support efficient dosing, blending, and large-scale production.
4. Competitive Advantages
- Quality Consistency: Controlled food-grade quality supports repeatable formulation and production performance.
- Supply Reliability: Suitable for structured B2B procurement programs and recurring bulk requirements.
- Logistics Capability: 25kg bag packaging facilitates handling, warehousing, palletization, and international shipment.
- Price Competitiveness: Bulk procurement options support cost-efficient sourcing for commercial-scale manufacturers.
- Sustainability: Milk-derived lactose provides an established value-added route for utilization of dairy-processing streams.
- Technical Documentation: Product specifications, Certificates of Analysis, and relevant quality documentation can be provided subject to supplier availability.
- Strategic Sourcing: Combines dependable quality, practical packaging, scalable supply, and competitive bulk procurement for international buyers.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Packaging: 25kg bags
- Loading Capacity: Typically 20–24 MT per container, subject to packaging configuration, palletization, and shipping requirements
- Supply: Available for bulk B2B and international procurement subject to confirmed order specifications and destination requirements
Reviews
There are no reviews yet.