
1. Product Overview
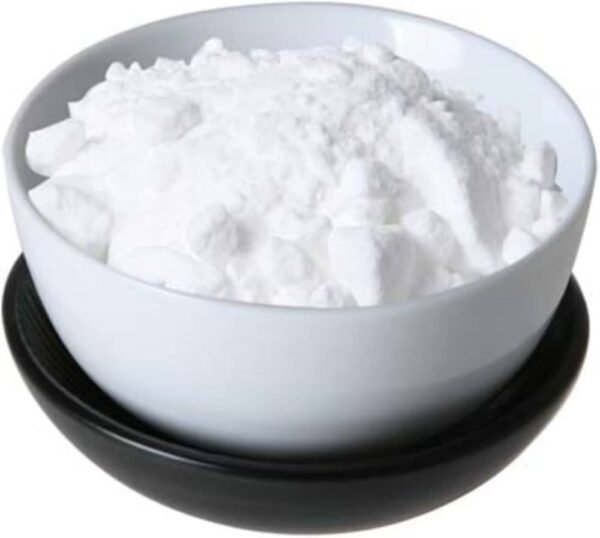
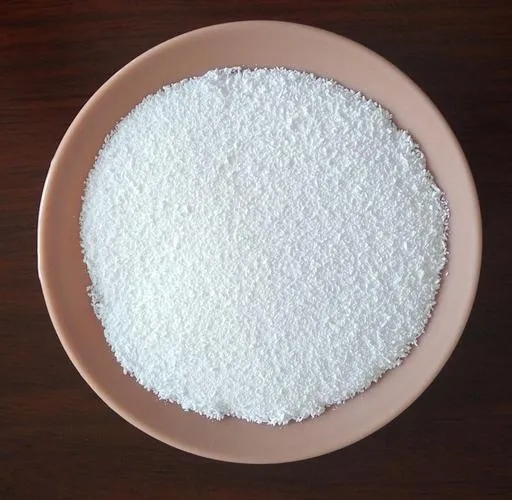
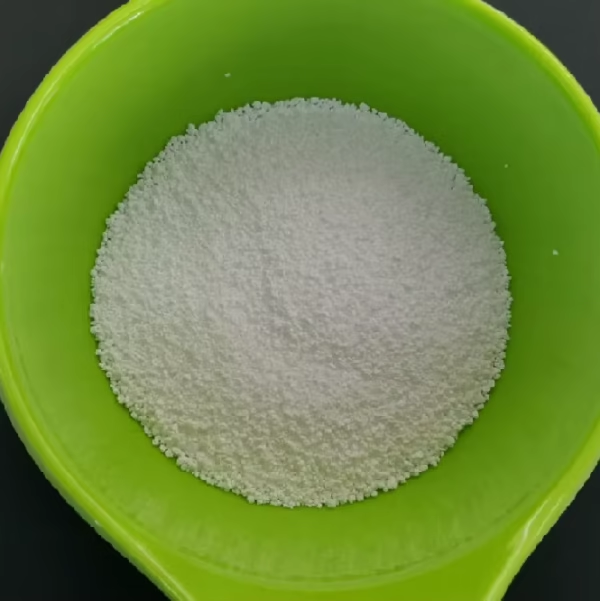
Potassium Bicarbonate Food Grade is a high-purity, food-grade alkaline compound (KHCO₃) supplied as a fine white crystalline powder for food processing and industrial applications. It is primarily used as a leavening agent, acidity regulator, buffering agent, and potassium source in formulated food products. Its reliable performance, clean functionality, and suitability for controlled food-processing environments make it a valuable alternative to sodium-based bicarbonates where reduced sodium content is required. The 25kg bag format supports efficient handling, storage, and bulk procurement for commercial food manufacturers and ingredient distributors.
2. Key Specifications & Technical Characteristics
- Chemical Composition: Potassium Bicarbonate (KHCO₃)
- Grade: Food Grade
- Purity: High purity; specification-controlled for food-processing applications
- Physical Form: Fine crystalline powder
- Colour: White
- Solubility: Soluble in water
- Functionality: Leavening agent, acidity regulator, buffering agent, and potassium source
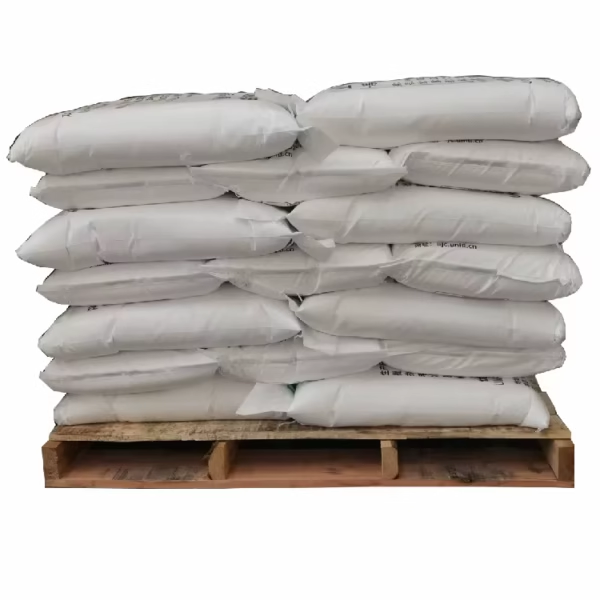
- Packaging: 25kg industrial-grade bag
- Shelf Life: Typically 24 months when stored correctly in sealed, dry conditions
- Storage: Store in a cool, dry, well-ventilated area away from moisture and incompatible materials
- Origin: Available according to supplier production and sourcing requirements
- Documentation: Product specification and quality documentation available upon request
3. Core Industrial Applications
- Food & Beverage Manufacturing: Used as a leavening and acidity-regulating ingredient in formulated foods and beverages.
- Bakery Products: Supports controlled rising and pH adjustment in selected bakery formulations.
- Low-Sodium Food Formulations: Provides potassium functionality where manufacturers seek to reduce reliance on sodium bicarbonate.
- Food Processing: Used as a buffering and processing aid in applications requiring controlled alkalinity.
- Ingredient Manufacturing: Suitable for incorporation into commercial premixes and formulated food ingredients.
- Industrial Advantage: Consistent chemical performance enables controlled formulation, efficient processing, and dependable batch-to-batch results.
4. Competitive Advantages
- Quality Consistency: High-purity food-grade material designed for dependable formulation performance.
- Supply Reliability: Suitable for recurring commercial procurement and large-volume sourcing programs.
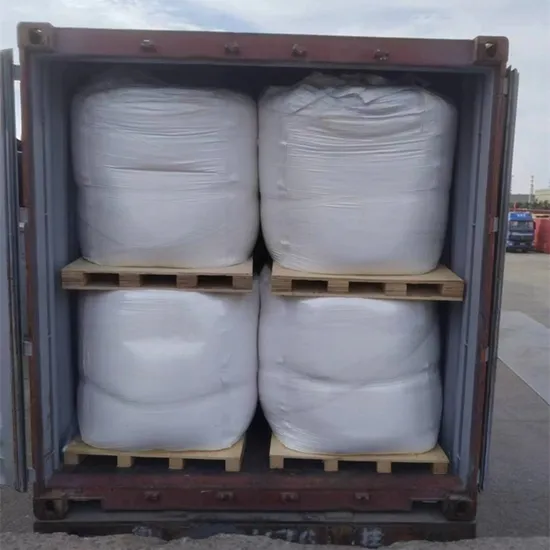
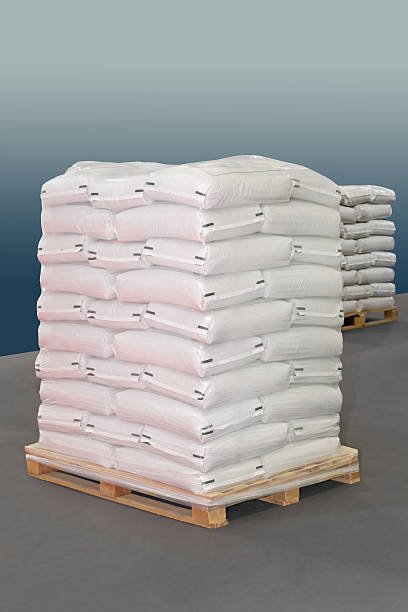
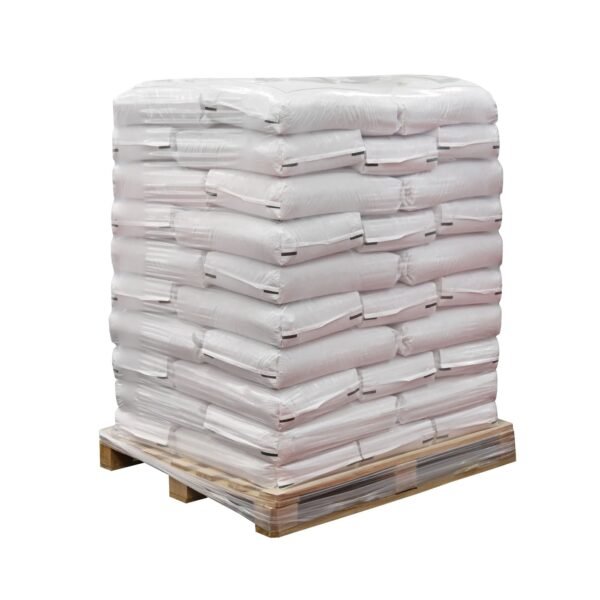
- Logistics Capability: Standard 25kg bags facilitate warehouse handling, palletisation, container loading, and international distribution.
- Price Competitiveness: Bulk sourcing options support commercially efficient procurement for manufacturers and distributors.
- Sustainability: Potassium-based formulation can support product development strategies focused on sodium reduction.
- Technical Documentation: Product specifications and relevant quality documentation can be provided to support purchasing and quality-control requirements.
- Strategic Sourcing Value: Combines food-grade quality, scalable supply, practical packaging, and reliable commercial fulfilment for international B2B buyers.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Subject to container type, packaging configuration, and applicable shipping requirements
- Packaging: 25kg bags
- Supply: Bulk and recurring contract supply available

Reviews
There are no reviews yet.