
1. Product Overview
Milkshake Powder Food Grade is a formulated dry powder blend designed for efficient preparation of consistent, creamy milkshake beverages in commercial and industrial food-service applications. It is primarily used by beverage manufacturers, cafés, restaurants, dessert producers, catering operations, and institutional food-service providers. The powder offers convenient handling, rapid preparation, consistent flavor and texture, and simplified inventory management compared with sourcing and blending multiple individual ingredients. Its bulk format supports scalable beverage production and efficient B2B procurement.
2. Key Specifications & Technical Characteristics
- Product: Milkshake Powder Food Grade
- Grade: Food Grade
- Composition: Typically formulated from dairy and/or non-dairy milk solids, sugar, permitted food ingredients, stabilizers, emulsifiers, flavoring agents, and other formulation-specific components
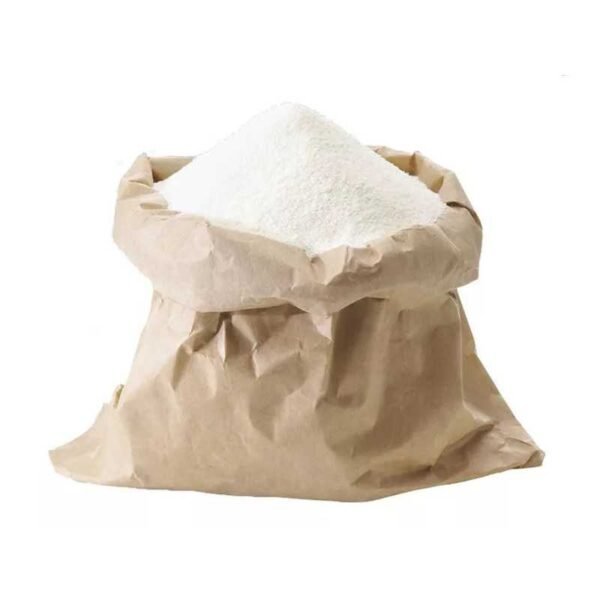
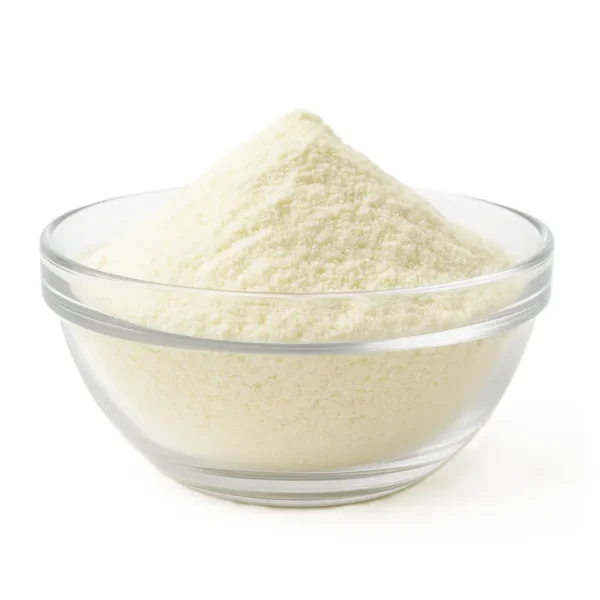
- Physical Form: Free-flowing dry powder
- Appearance: Typically white to cream-colored, depending on formulation and flavor
- Texture: Fine, homogeneous powder designed for rapid dispersion
- Flavor: Milkshake-compatible flavor profile; formulation may be customized according to commercial requirements
- Purity & Compliance: Manufactured for food-use applications and supplied according to applicable food-grade specifications
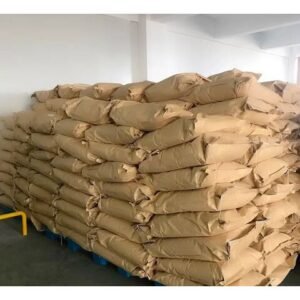
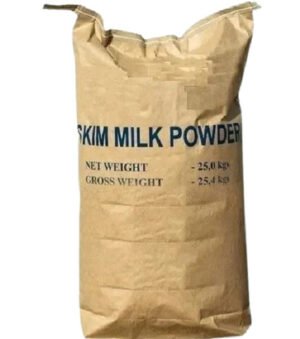
- Packaging: 25kg industrial bags
- Shelf Life: Typically 12–24 months when stored unopened under recommended conditions; exact shelf life should be confirmed against the product specification
- Storage: Store in a cool, dry, clean environment, protected from moisture, direct sunlight, contamination, and excessive heat
3. Core Industrial Applications
- Beverage Manufacturing: Used as a base ingredient for large-scale production of ready-to-mix or prepared milkshake beverages.
- Food-Service & Hospitality: Suitable for cafés, restaurants, hotels, dessert shops, catering companies, and institutional kitchens requiring consistent beverage preparation.
- Dairy & Dessert Processing: Used in milkshake, flavored dairy beverage, dessert, and specialty beverage formulations.
- Commercial Beverage Dispensing: Supports standardized preparation through dispensing and mixing systems, helping operators maintain consistent taste and texture.
- Industrial Advantages: Dry powder format reduces handling complexity, supports longer storage than many liquid ingredients, and enables controlled portioning and repeatable formulations.
4. Competitive Advantages
- Quality Consistency: Uniform dry formulation supports repeatable flavor, texture, and beverage performance across production batches.
- Supply Reliability: Bulk commercial packaging supports planned procurement and continuous production requirements.
- Logistics Capability: 25kg bags are practical for palletized storage, containerized transportation, and international B2B distribution.
- Price Competitiveness: Bulk sourcing can reduce per-unit procurement and handling costs for commercial-scale buyers.
- Operational Efficiency: Easy storage, measured dosing, and rapid preparation can simplify beverage production and reduce formulation complexity.
- Sustainability: Dry powder formats can reduce the transportation of water compared with equivalent liquid formulations, potentially improving freight efficiency.
- Technical Documentation: Product specifications, certificates, ingredient information, and applicable food-safety documentation can be provided subject to supplier and market requirements.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Approximately 20–24 MT per 20ft container, subject to packaging configuration, palletization, product density, and applicable container weight limits
- Packaging: 25kg bags
Reviews
There are no reviews yet.