
1. Product Overview
Xanthan Gum is a high-performance microbial polysaccharide widely used as a rheology modifier, thickener, stabilizer, and suspension agent across food, pharmaceutical, personal care, and industrial formulations. It delivers excellent viscosity control at low concentrations while maintaining stability across a broad range of temperatures, pH conditions, and processing environments. Its reliable functional performance makes it a strategically important ingredient for manufacturers seeking formulation consistency, processing efficiency, and dependable product quality.
2. Key Specifications & Technical Characteristics
- Chemical composition: High-molecular-weight polysaccharide produced through microbial fermentation
- Primary function: Thickener, stabilizer, suspending agent, emulsification aid, and rheology modifier
- Grade: Food, industrial, pharmaceutical, or technical grade available according to specification
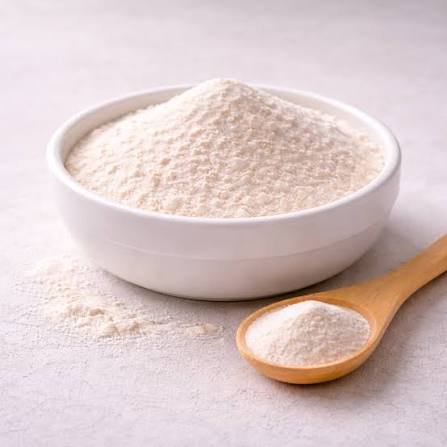
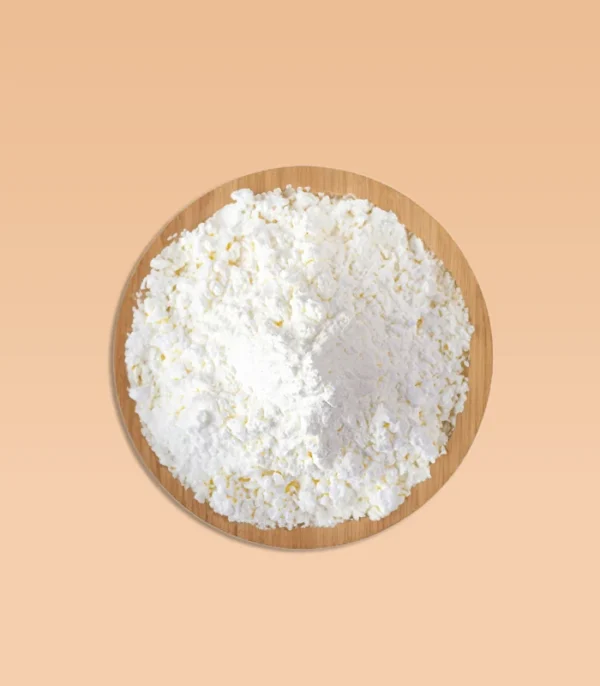
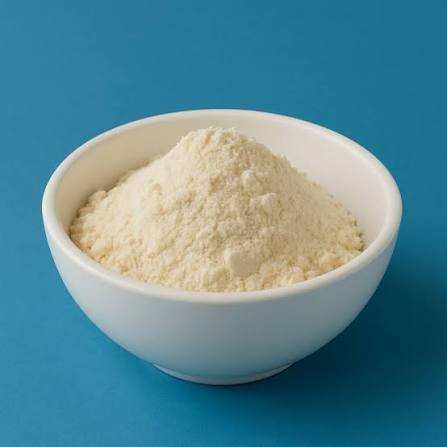
- Appearance: Fine, free-flowing powder
- Colour: White to cream/off-white
- Solubility: Dispersible and soluble in water with strong viscosity-building properties
- Purity: Typically supplied to applicable industry-grade specifications, with certificate of analysis available upon request
- Viscosity: Grade-dependent; available in specifications suitable for different formulation requirements
- Packaging options: 25kg bags and bulk packaging available subject to order requirements
- Shelf life: Typically 24 months when stored in original, sealed packaging under recommended conditions
- Storage: Keep dry, cool, and protected from moisture and direct sunlight
- Origin: Available from qualified international manufacturing sources
3. Core Industrial Applications
Xanthan Gum is widely used in food and beverage, pharmaceutical, cosmetics and personal care, oilfield, agricultural, and industrial chemical formulations. In food processing, it provides viscosity, suspension, texture, and emulsion stability in sauces, dressings, beverages, dairy products, bakery formulations, and processed foods. Pharmaceutical and personal-care manufacturers use it to improve formulation consistency, suspension stability, and controlled flow properties. Its strong thickening efficiency at relatively low dosage levels can reduce formulation requirements while delivering dependable processing and finished-product performance.
4. Competitive Advantages
- Consistent quality: Reliable rheological performance supports repeatable production and formulation control.
- High functional efficiency: Provides effective thickening and stabilization at low inclusion levels.
- Broad formulation compatibility: Performs across diverse pH, temperature, and processing conditions.
- Supply reliability: Suitable for structured B2B procurement and recurring industrial supply programs.
- Logistics capability: Bulk commercial supply and containerized shipment options support international sourcing.
- Price competitiveness: Scalable procurement options help optimize total formulation and sourcing costs.
- Technical documentation: Product specifications, certificates of analysis, and relevant documentation can be provided according to grade and application.
- Strategic sourcing value: A versatile, high-efficiency functional ingredient suitable for manufacturers seeking dependable quality and supply continuity.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Approximately 20–25 MT per 20-foot container, subject to packaging configuration, product grade, and applicable shipping limitations
- Supply Format: Bulk commercial and containerized international supply available


Reviews
There are no reviews yet.