
1. Product Overview
Sorbitol 70% Solution is a high-purity aqueous solution of sorbitol, widely used as a functional sweetener, humectant, stabilizer, plasticizer, and formulation aid across multiple industries. Its excellent moisture-retention, solubility, sweetness, and formulation properties make it valuable in food, pharmaceutical, personal care, and industrial applications. The product supports consistent processing performance while helping manufacturers optimize formulation stability, texture, and product shelf life. As a versatile, high-volume ingredient, Sorbitol 70% Solution is a strategically important raw material for reliable industrial and commercial sourcing.
2. Key Specifications & Technical Characteristics
- Chemical Composition: Sorbitol dissolved in purified water
- Concentration: 70% sorbitol solution
- Grade: Industrial / Food / Pharmaceutical grade available according to specification
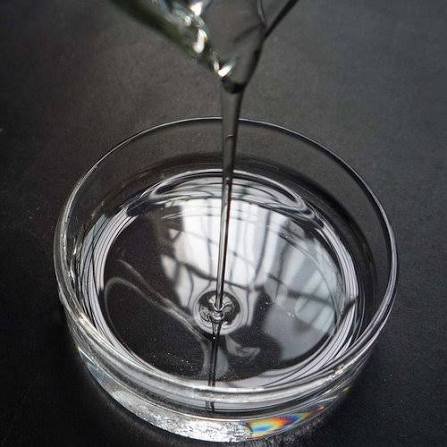
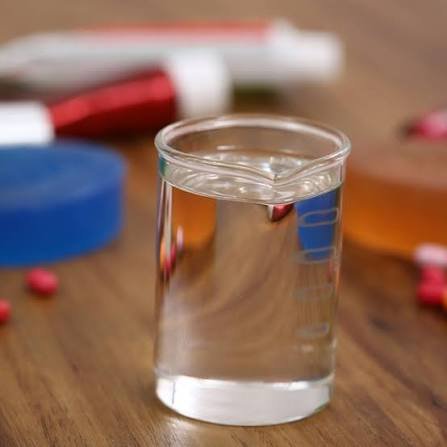
- Physical Form: Clear, viscous liquid
- Color: Colorless to slightly yellow, depending on specification
- Solubility: Highly soluble in water
- Functional Properties: Humectant, sweetener, stabilizer, plasticizer, moisture-retention agent
- Packaging Options: Drums, IBC totes, flexitanks, or bulk tanker supply
- Shelf Life: Typically up to 24 months when stored under recommended conditions
- Storage: Store in tightly sealed containers in a cool, dry, clean environment, protected from contamination and extreme temperatures
- Origin: Available from established international manufacturing and supply sources
3. Core Industrial Applications
- Food & Beverage: Used as a sweetener, humectant, texture modifier, and moisture-retention agent in confectionery, bakery products, beverages, and processed foods.
- Pharmaceuticals: Used as an excipient, sweetening agent, humectant, and formulation aid in syrups, oral-care products, and other pharmaceutical preparations.
- Personal Care & Cosmetics: Supports moisture retention and formulation stability in toothpaste, creams, lotions, gels, and other personal-care products.
- Industrial Manufacturing: Used as a functional ingredient and plasticizing or moisture-control component in selected industrial formulations.
- Performance Benefits: Provides consistent solubility, moisture control, formulation flexibility, and dependable batch-to-batch performance, supporting efficient large-scale production and formulation consistency.
4. Competitive Advantages
- Quality Consistency: Controlled concentration and consistent physical characteristics support reliable industrial processing.
- Supply Reliability: Suitable for recurring bulk procurement and long-term supply programs.
- Logistics Capability: Available in multiple packaging formats to support containerized, IBC, flexitank, and bulk transportation requirements.
- Price Competitiveness: Bulk sourcing options help manufacturers optimize total raw-material procurement costs.
- Sustainability: Efficient bulk packaging and transportation formats can help reduce packaging requirements and improve supply-chain efficiency.
- Technical Documentation: Product specifications, certificates of analysis, safety documentation, and other technical information can be provided according to buyer requirements.
- Strategic Sourcing Value: A versatile, high-volume ingredient suitable for manufacturers seeking dependable quality, scalable supply, and commercially competitive procurement.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Approximately 20–24 MT per 20-foot container, subject to packaging format, product density, and applicable transport regulations



Reviews
There are no reviews yet.