
1. Product Overview
Soy Protein Isolate Food Grade is a high-purity plant-based protein ingredient derived from soybeans, typically containing approximately 90% protein on a dry basis. Supplied in 25kg bags, it is widely used by food manufacturers to enhance protein content, nutritional value, texture, and functional performance across diverse formulations. Its strong emulsification, water-binding, and dispersibility characteristics make it a commercially valuable alternative to animal-derived and other plant-based proteins. It supports growing demand for scalable, cost-efficient, and sustainable protein solutions in global food manufacturing.
2. Key Specifications & Technical Characteristics
- Product: Soy Protein Isolate
- Grade: Food Grade
- Protein Content: Typically ≥90% on a dry basis
- Raw Material: Defatted, processed soybeans
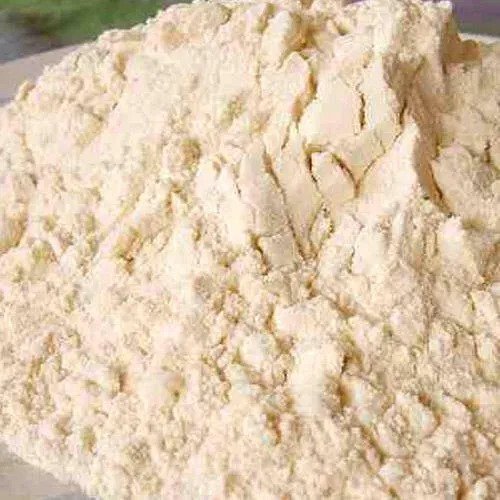
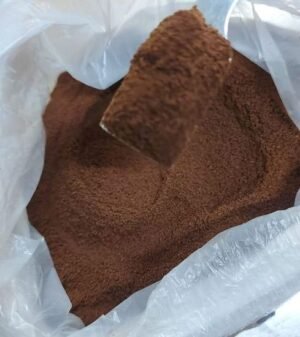
- Form: Fine powder
- Color: Cream to light yellow
- Taste & Odor: Mild, characteristic soy profile
- Functional Properties: High protein concentration, emulsification, water absorption, dispersibility, and binding capability
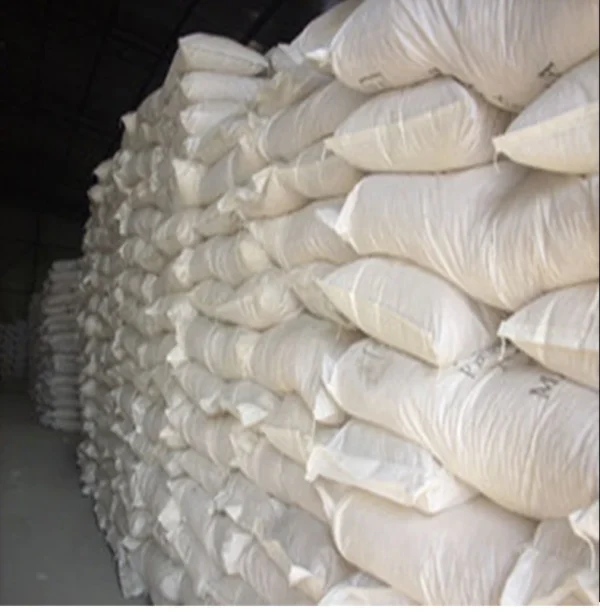
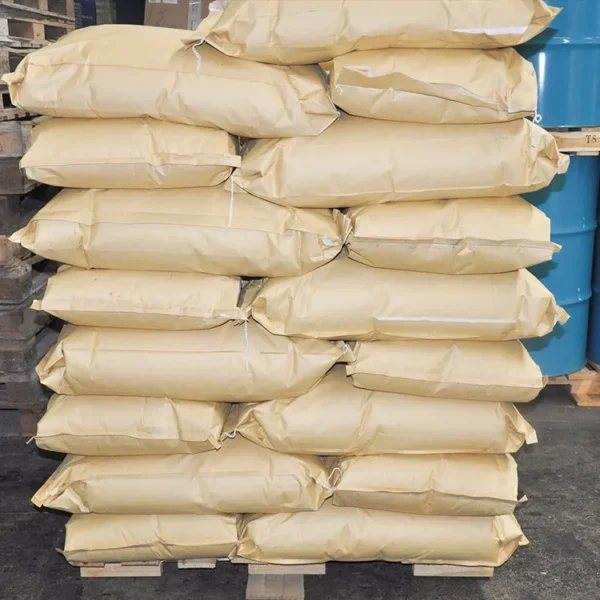
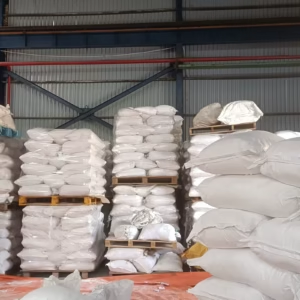
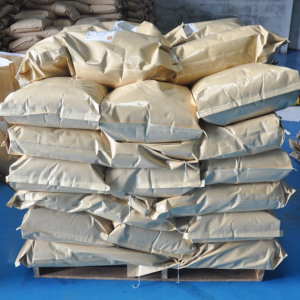
- Packaging: 25kg food-grade bags; bulk packaging available subject to supply requirements
- Storage: Store in a cool, dry, well-ventilated area away from direct sunlight and moisture
- Shelf Life: Typically 12–24 months when stored under recommended conditions
- Documentation: Product specification, Certificate of Analysis (CoA), and other quality documentation available subject to order requirements
3. Core Industrial Applications
- Protein-Enriched Foods: Used in nutritional products, protein foods, meal replacements, and functional food formulations to increase protein content efficiently.
- Meat Alternatives: Provides structure, binding, water retention, and protein enrichment in plant-based meat and meat-substitute products.
- Bakery & Cereals: Incorporated into bread, bakery mixes, cereal products, and nutrition bars to improve nutritional profiles.
- Dairy Alternatives: Used in plant-based beverages and other formulated products to increase protein content and improve mouthfeel.
- Sports Nutrition: Suitable for protein powders, nutritional blends, and performance-oriented food formulations.
- Processed Foods: Supports texture, emulsification, binding, and formulation stability in a range of processed food applications.
4. Competitive Advantages
- High Protein Concentration: Delivers a concentrated source of plant-based protein, supporting efficient nutritional fortification.
- Consistent Quality: Manufactured and supplied to food-grade specifications for dependable formulation performance.
- Functional Performance: Offers useful emulsification, water-binding, and binding properties across multiple food-processing applications.
- Supply Reliability: Suitable for commercial and bulk procurement programs requiring dependable volumes and repeat supply.
- Logistics Capability: 25kg bag packaging facilitates handling, warehousing, distribution, and international shipment.
- Price Competitiveness: Bulk sourcing can support cost-efficient procurement for industrial food manufacturers.
- Sustainability: Plant-based protein supports diversified protein sourcing and can contribute to formulations designed around alternative protein systems.
- Technical Documentation: Product specifications and quality documentation can be provided to support buyer qualification and quality-control processes.
5. Commercial & Supply Information
- Packaging: 25kg bag
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Approximately 20–24 MT per 20-foot container, depending on packaging configuration, loading method, and applicable shipping restrictions
- Supply: Bulk and commercial quantities available
- Documentation: CoA and relevant product documentation available upon request
Reviews
There are no reviews yet.