
1. Product Overview
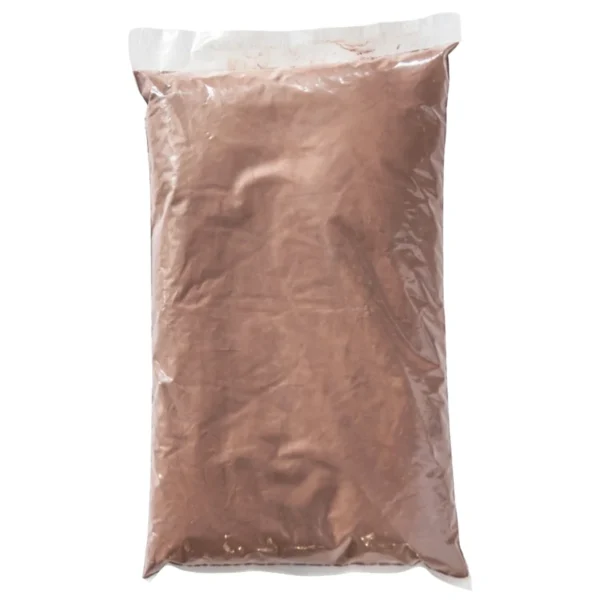
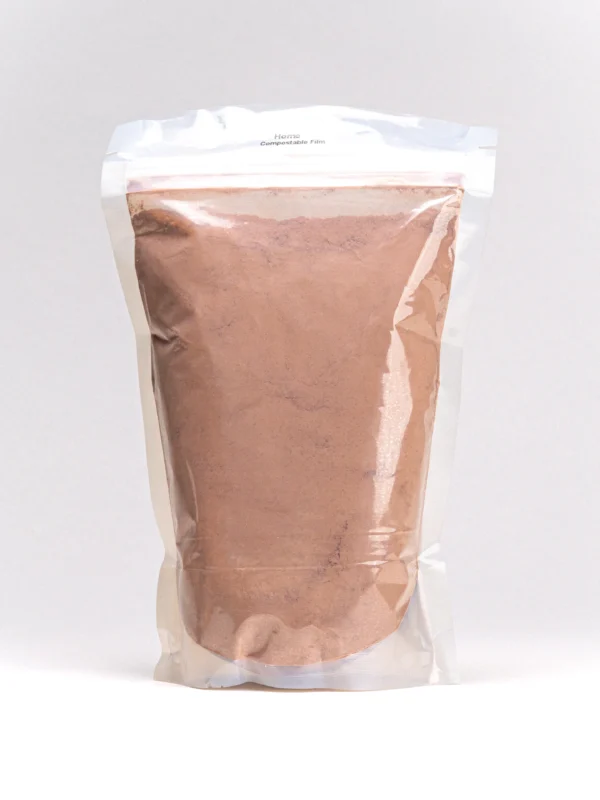
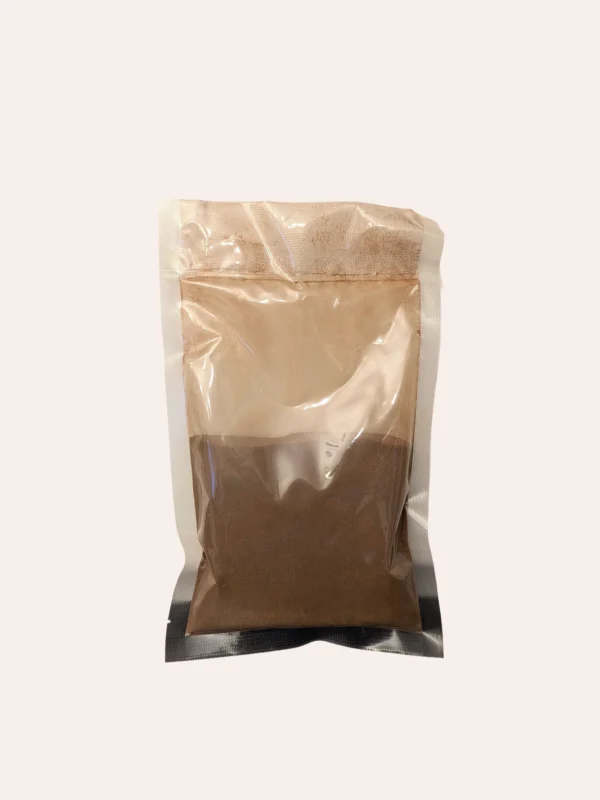
Soluble Instant Coffee Powder Food Grade is a convenient, rapidly dissolving coffee ingredient designed for beverage manufacturers, food processors, cafés, hospitality operators, and institutional applications. Produced for consistent flavour, aroma, and solubility, it enables efficient preparation of instant coffee beverages without conventional brewing equipment. Its practical handling, reliable performance, and bulk 20kg packaging make it well suited to commercial-scale procurement and production. The product supports streamlined beverage manufacturing and dependable supply across international B2B markets.
2. Key Specifications & Technical Characteristics
- Product Type: Soluble instant coffee powder
- Grade: Food Grade
- Material Composition: Soluble coffee solids derived from roasted and processed coffee beans
- Form: Fine, free-flowing powder or granulated soluble coffee
- Colour: Brown to dark brown, subject to product specification
- Solubility: Rapidly soluble in hot water; suitable for instant beverage preparation
- Aroma & Flavour: Characteristic coffee aroma and flavour profile
- Purity: Food-grade specification suitable for commercial food and beverage applications
- Packaging: 20kg bulk bags, with packaging configurations available according to buyer requirements
- Shelf Life: Typically up to 24 months when stored in a cool, dry environment in sealed original packaging
- Storage: Protect from moisture, heat, direct sunlight, and contamination
3. Core Industrial Applications
- Food & Beverage Manufacturing: Used in instant coffee blends, ready-to-drink beverages, coffee mixes, and powdered beverage formulations.
- Hospitality & Foodservice: Suitable for hotels, restaurants, cafés, catering companies, and institutional beverage service.
- Bakery & Confectionery: Used as a coffee flavouring and functional ingredient in cakes, biscuits, desserts, chocolates, and fillings.
- Dairy & Dessert Production: Applied in coffee-flavoured dairy products, ice creams, mousses, and other formulated desserts.
- Industrial Beverage Production: Provides rapid dissolution and consistent dosing, helping manufacturers improve production efficiency and formulation control.
- Commercial Advantage: Compared with traditionally brewed coffee, soluble coffee offers faster preparation, easier storage, reduced equipment requirements, and convenient portioning for high-volume operations.
4. Competitive Advantages
- Quality Consistency: Designed to deliver consistent solubility, flavour, aroma, and handling characteristics across commercial batches.
- Supply Reliability: Bulk-oriented sourcing supports recurring procurement requirements for manufacturers and distributors.
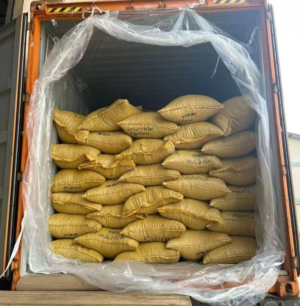
- Logistics Capability: 20kg packaging facilitates efficient warehousing, handling, palletisation, and international shipment.
- Price Competitiveness: Bulk supply can support cost-efficient procurement for high-volume commercial buyers.
- Operational Efficiency: Fast dissolution reduces preparation time and simplifies beverage production and service.
- Sustainability Considerations: Soluble coffee can reduce the need for brewing infrastructure and associated operational resources in suitable applications.
- Technical Documentation: Product specifications, quality documentation, and supporting commercial information can be provided according to buyer and market requirements.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Subject to container type, packaging configuration, palletisation, and applicable shipping requirements
- Packaging: 20kg bags
- Supply: Bulk international B2B supply
Reviews
There are no reviews yet.