
- Product Overview
Sodium Citrate Food Grade is a high-purity food additive supplied in a convenient 25kg bag for industrial food and beverage applications. It is widely used as an acidity regulator, buffering agent, emulsifying aid, and stabilizer in processed foods, beverages, dairy products, and pharmaceutical formulations. Its reliable functional performance supports consistent product quality, pH control, and formulation stability. For bulk buyers, it provides a versatile and commercially efficient ingredient for large-scale manufacturing. - Key Specifications & Technical Characteristics
- Chemical Composition: Trisodium citrate, commonly supplied as sodium citrate dihydrate or anhydrous grade depending on specification
- Grade: Food Grade
- Purity: Typically high purity, subject to applicable food-grade specification and certificate of analysis
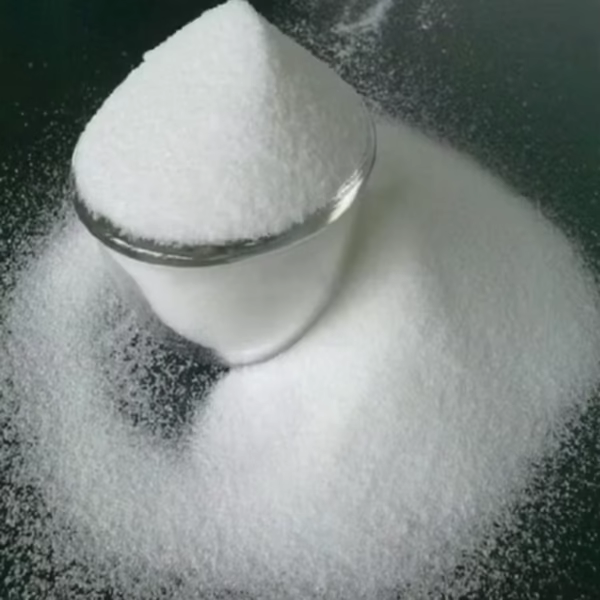
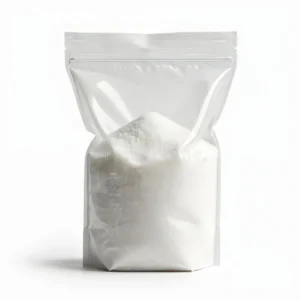
- Physical Form: White crystalline powder or granules
- Appearance: White, free-flowing crystalline material
- Solubility: Highly soluble in water
- Functionality: Acidity regulator, buffering agent, stabilizer, sequestrant, and emulsifying aid
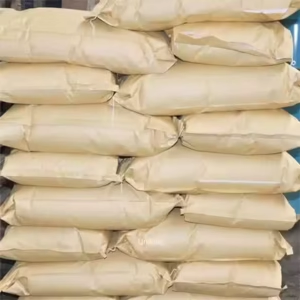
- Packaging: 25kg bags; bulk packaging options may be available upon request
- Shelf Life: Typically 24–36 months when stored in sealed packaging under cool, dry conditions
- Documentation: Certificate of Analysis (COA) and relevant technical documentation available subject to supply specification
- Core Industrial Applications
- Food & Beverage: Used in soft drinks, fruit beverages, sauces, jams, confectionery, and processed foods for acidity and pH regulation.
- Dairy & Cheese Processing: Supports emulsification, texture control, and processing stability in cheese and dairy formulations.
- Bakery & Processed Foods: Helps maintain consistent formulation performance and product stability.
- Pharmaceutical Manufacturing: Used as a buffering and formulation ingredient where food/pharmaceutical-grade specifications are required.
- Industrial Food Processing: Provides dependable pH control and sequestration performance, helping manufacturers achieve consistent batch quality and processing efficiency.
- Competitive Advantages
- Quality Consistency: Food-grade material designed for reliable performance across industrial formulations.
- Supply Reliability: Suitable for structured bulk procurement and recurring B2B supply programs.
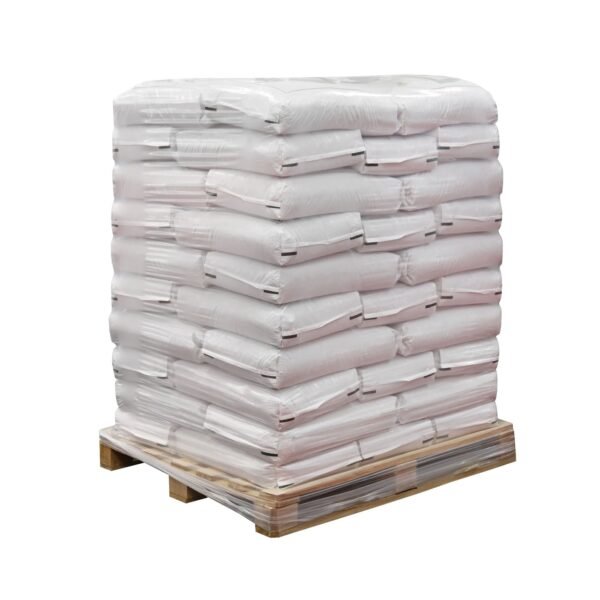
- Logistics Capability: 25kg bag packaging supports efficient handling, warehousing, palletization, and international shipment.
- Price Competitiveness: Bulk sourcing enables commercially efficient procurement for high-volume manufacturers and distributors.
- Sustainability: Efficient bulk packaging and consolidated shipments can support optimized transportation and material handling.
- Technical Documentation: Product specifications and quality documentation can be provided to support buyer qualification and procurement requirements.
- Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Approximately 20–25 MT per 20ft container, depending on packaging configuration, palletization, and applicable shipping limits
Reviews
There are no reviews yet.