
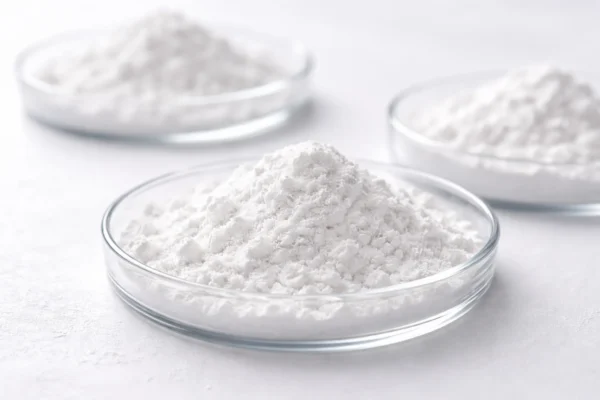
1. Product Overview
Sodium Benzoate is a high-purity, water-soluble preservative widely used to inhibit the growth of bacteria, yeast, and molds in formulated products. It is primarily supplied to the food, beverage, pharmaceutical, personal care, and industrial sectors where product stability and shelf-life are critical. Its consistent performance, ease of incorporation, and cost efficiency make it a dependable choice for large-scale manufacturing. As a globally traded functional ingredient, Sodium Benzoate supports reliable formulation control and efficient industrial production.
2. Key Specifications & Technical Characteristics
- Chemical composition: Sodium benzoate (C₇H₅NaO₂)
- CAS No.: 532-32-1
- Purity: Typically ≥99% for standard industrial/food-grade material
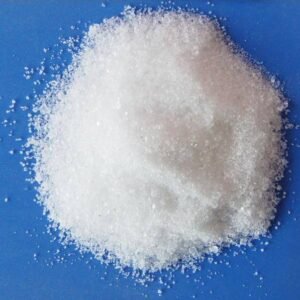
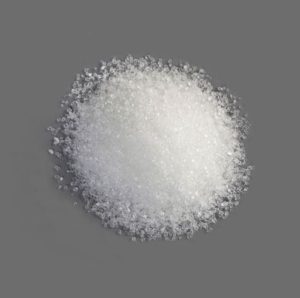
- Appearance: White crystalline powder or granules
- Solubility: Highly soluble in water
- Odor: Practically odorless
- Grade options: Food grade, pharmaceutical grade, and industrial grade, subject to specification
- Packaging options: 25 kg bags; 500 kg–1,000 kg jumbo bags; customized bulk packaging available
- Shelf life: Typically 24 months when stored in sealed packaging under dry, cool conditions
- Storage: Protect from moisture, direct sunlight, and contamination
3. Core Industrial Applications
- Food & Beverage: Used as a preservative in acidic foods, beverages, sauces, condiments, fruit preparations, and other formulated products to help control microbial growth.
- Pharmaceuticals: Utilized as an excipient and preservative in selected pharmaceutical formulations.
- Personal Care & Cosmetics: Supports preservation systems in creams, lotions, shampoos, and other water-based formulations.
- Industrial Formulations: Used where controlled microbial stability and formulation consistency are required.
Sodium Benzoate offers effective preservation particularly in acidic formulations, with good water solubility and straightforward processing. Its dependable performance can help manufacturers maintain product quality while supporting efficient formulation and inventory management.
4. Competitive Advantages
- Quality consistency: Controlled purity and uniform physical characteristics support repeatable manufacturing results.
- Supply reliability: Suitable for regular industrial procurement and contract-based supply programs.
- Logistics capability: Bulk packaging and containerized shipment options support international sourcing and efficient material handling.
- Price competitiveness: Cost-effective performance makes it suitable for high-volume commercial applications.
- Storage efficiency: Stable under recommended storage conditions, supporting practical warehousing and extended supply planning.
- Technical documentation: Product specifications, certificates of analysis, safety documentation, and other compliance documents can be provided according to grade and buyer requirements.
- Strategic sourcing value: Available in bulk quantities to support manufacturers seeking predictable quality, dependable supply, and competitive procurement economics.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20 MT
- Loading Capacity: Approximately 20–25 MT per 20-foot container, subject to packaging configuration, product density, and applicable shipping requirements
- Packaging: 25 kg bags or jumbo bags; customized packing available upon request
- Supply: Bulk and recurring contract orders supported

Reviews
There are no reviews yet.