
1. Product Overview
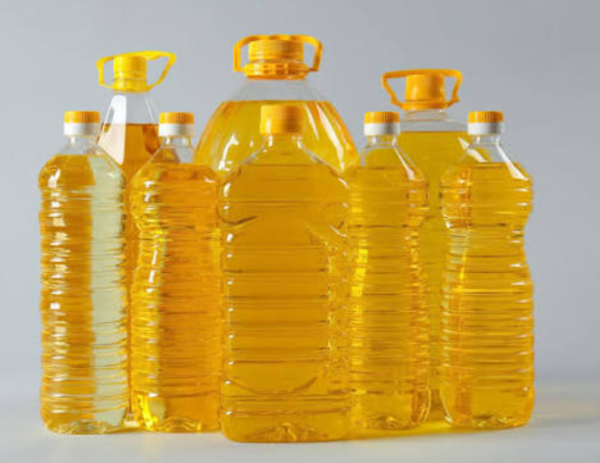
Refined Sunflower Oil Food Grade is a high-quality, refined edible vegetable oil processed to deliver consistent taste, appearance, and performance. It is widely used across food manufacturing, commercial cooking, frying, baking, and food-service operations. Its neutral flavor, light color, and reliable thermal performance make it a versatile ingredient for large-scale food production. As a globally traded edible oil, it provides buyers with a dependable, cost-effective solution for consistent food manufacturing and distribution.
2. Key Specifications & Technical Characteristics
- Product: Refined Sunflower Oil – Food Grade
- Origin: Sunflower seeds
- Grade: Food Grade / EdibleRefined Canola Oil Food Grade
- Composition: Predominantly sunflower oil triglycerides, naturally rich in unsaturated fatty acids
- Purity: Refined, suitable for food-processing applications and manufactured according to applicable food-grade requirements
- Appearance: Clear, bright liquid
- Color: Pale yellow to golden yellow
- Flavor & Odor: Neutral to mild, characteristic of refined sunflower oil
- Physical Form: Liquid at ambient temperature
- Moisture & Impurities: Controlled to food-industry specifications
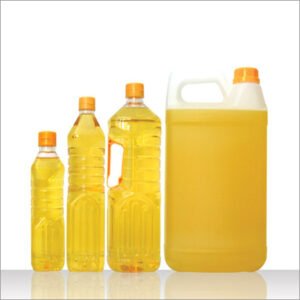
- Packaging Options: Bulk tanker, flexitank, drums, IBC containers, and other customized formats subject to order requirements
- Shelf Life: Typically up to 12–24 months when stored appropriately in sealed, food-grade containers away from heat, light, and moisture
3. Core Industrial Applications
- Food Manufacturing: Used in sauces, dressings, margarine, mayonnaise, processed foods, and ready-to-eat products.
- Baking & Confectionery: Suitable for cakes, pastries, bakery mixes, and other formulations requiring a neutral-tasting vegetable oil.
- Frying & Food Service: Provides dependable performance for commercial and industrial frying operations.
- Snack Production: Used in the preparation and processing of chips, crisps, nuts, and other fried snacks.
- Food Ingredient Formulation: Serves as a versatile base oil where consistent quality, neutral flavor, and light appearance are required.
- Commercial Advantage: Its neutral sensory profile and versatile functionality allow manufacturers to achieve consistent product quality while maintaining efficient large-volume processing.
4. Competitive Advantages
- Quality Consistency: Refined and standardized for dependable performance across repeated production batches.
- Supply Reliability: Suitable for structured bulk procurement and recurring industrial supply programs.
- Logistics Capability: Available in bulk and multiple packaging formats to support international and industrial distribution requirements.
- Price Competitiveness: Bulk procurement options help optimize landed cost and improve purchasing efficiency.
- Versatile Performance: Suitable for frying, baking, food formulation, and general food-processing applications.
- Sourcing Efficiency: Consolidated bulk supply can reduce procurement complexity and support predictable production planning.
- Documentation: Product specifications, quality documentation, certificates of analysis, and relevant shipping documentation can be provided according to buyer and destination requirements.
- Strategic Value: A dependable option for food manufacturers, distributors, wholesalers, and commercial buyers seeking consistent edible-oil supply at industrial scale.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK – 20 MT
- Loading Capacity: Approximately 20–24 MT per 20-foot container, subject to packaging configuration, container payload restrictions, and destination requirements
- Supply Format: Bulk and customized industrial packaging available
- International Supply: Export-oriented supply available subject to destination, regulatory, and logistics requirements
Reviews
There are no reviews yet.