
1. Product Overview
Refined Corn Oil Food Grade is a high-quality edible vegetable oil derived from carefully processed corn germ and refined to deliver consistent purity, flavor, and performance. It is widely used across food manufacturing, cooking-oil production, bakery, snack, and processed-food applications. Its neutral taste, stable performance, and versatile functionality make it a dependable ingredient for large-scale food production. Strategically, it offers buyers a scalable, commercially efficient vegetable-oil solution for consistent manufacturing requirements.
2. Key Specifications & Technical Characteristics
- Material: Refined vegetable oil derived from corn germ
- Grade: Food Grade
- Composition: Predominantly triglycerides of fatty acids, naturally containing oleic and linoleic acids
- Purity: Refined, bleached, and deodorized; specification-controlled for food applications
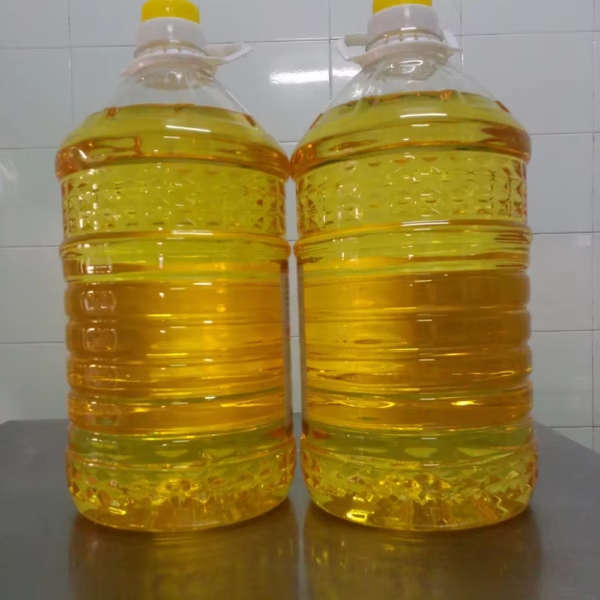
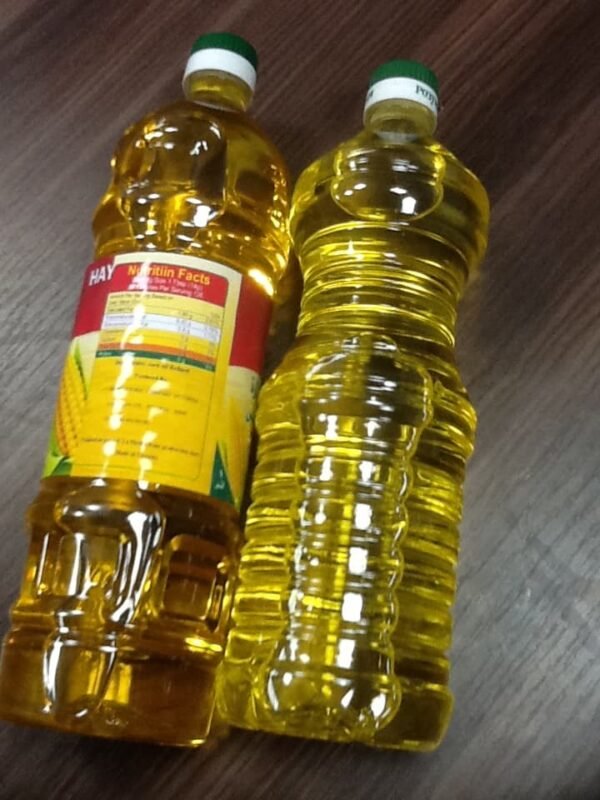
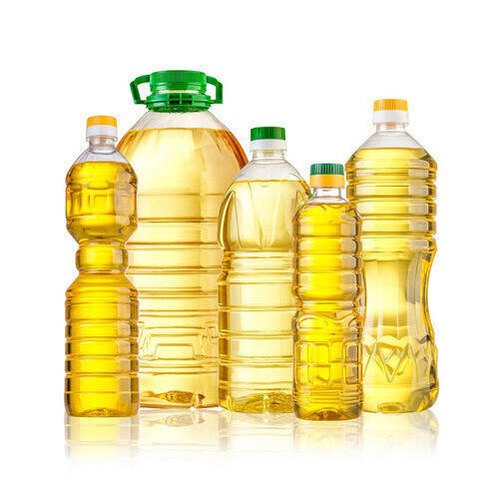
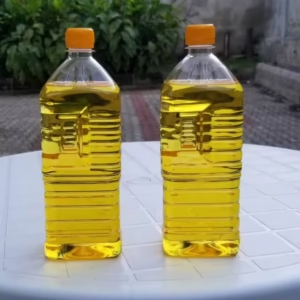
- Appearance: Clear, bright liquid
- Color: Pale yellow to golden yellow
- Odor & Taste: Mild, clean, and neutral
- Moisture & Impurities: Controlled to food-grade specifications
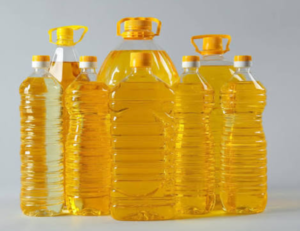
- Packaging Options: Bulk tanker, flexitank, IBC, drums, and other buyer-specified industrial packaging
- Shelf Life: Typically up to 12–24 months when stored under recommended conditions and in suitable packaging
- Storage: Store in a cool, dry place away from direct sunlight, heat, moisture, and strong odors
3. Core Industrial Applications
- Food Manufacturing: Used as a versatile cooking and processing oil in large-scale food production.
- Bakery & Confectionery: Suitable for formulations requiring a mild-tasting vegetable oil.
- Snack Production: Used in frying and processing applications where consistent oil performance is required.
- Margarine & Fat Blends: Serves as a functional vegetable-oil component in blended formulations.
- Sauces, Dressings & Processed Foods: Provides a neutral oil base without overpowering product flavor.
- Foodservice & Industrial Frying: Supports high-volume cooking operations with dependable handling and performance.
- Performance Advantage: Its refined, neutral profile and consistent physical characteristics support standardized production, efficient processing, and reliable product quality.
4. Competitive Advantages
- Quality Consistency: Controlled refining and specification management support dependable batch-to-batch performance.
- Supply Reliability: Suitable for recurring bulk procurement and long-term industrial sourcing programs.
- Logistics Capability: Available in bulk and flexible packaging formats to support international B2B distribution.
- Price Competitiveness: Bulk procurement and optimized supply-chain handling can provide attractive landed-cost economics.
- Sustainability: Vegetable-based sourcing provides a renewable-origin alternative to petroleum-derived processing inputs.
- Technical Documentation: Product specifications, certificates of analysis, safety/handling documentation, and other compliance documents can be supplied according to buyer requirements.
- Strategic Sourcing Value: Combines consistent food-grade quality, scalable supply, flexible packaging, and commercially competitive procurement for professional buyers.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20 MT
- Loading Capacity: Approximately 20–24 MT per container, depending on packaging configuration, container type, and applicable transport regulations
Reviews
There are no reviews yet.