

1. Product Overview
Potassium Sorbate is a high-performance food-grade preservative widely used to inhibit the growth of molds, yeasts, and selected microorganisms in food, beverage, and formulated products. It provides effective preservation while maintaining product quality, flavor, and shelf stability, making it a preferred solution for manufacturers requiring dependable microbial control. Its broad application range and strong performance make it strategically important for large-scale food processing and ingredient supply chains.
2. Key Specifications & Technical Characteristics
- Chemical Name: Potassium Sorbate
- Chemical Formula: C₆H₇KO₂
- CAS Number: 590-00-1
- Purity: Typically ≥99% for industrial/food-grade supply
- Grade: Food Grade; other grades available subject to specification
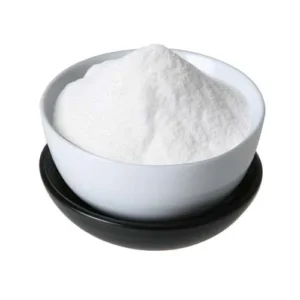
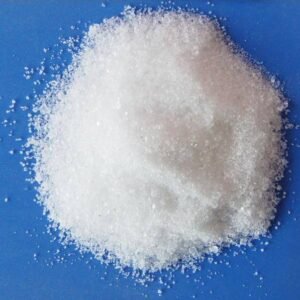
- Physical Form: White to off-white crystalline powder or granules
- Solubility: Highly soluble in water
- Particle Size: Available according to buyer or application requirements
- Packaging Options: 25 kg bags; bulk packaging available upon request
- Shelf Life: Typically 24 months when stored in a cool, dry, sealed environment
- Storage: Protect from moisture, excessive heat, and direct sunlight
3. Core Industrial Applications
- Food & Beverage Manufacturing: Used as a preservative in beverages, dairy products, sauces, dressings, jams, bakery products, and processed foods.
- Bakery & Confectionery: Helps control mold and yeast growth, supporting extended shelf life and reduced product losses.
- Dairy & Processed Foods: Supports microbial stability in selected cheese, dairy, and prepared-food applications.
- Sauces, Preserves & Condiments: Helps maintain product quality during storage and distribution.
- Industrial Formulations: Used in selected cosmetic, pharmaceutical, and other formulated products where permitted by applicable regulations.
Compared with less versatile preservation solutions, Potassium Sorbate offers effective antimicrobial protection at relatively low use levels, helping manufacturers improve shelf stability while maintaining product characteristics.
4. Competitive Advantages
- Quality Consistency: Controlled purity and physical characteristics support reliable batch-to-batch manufacturing performance.
- Supply Reliability: Suitable for scheduled bulk procurement and recurring industrial requirements.
- Logistics Capability: Bulk export supply, standardized packaging, and containerized shipment options support international sourcing.
- Price Competitiveness: Competitive bulk procurement structures help optimize ingredient costs for manufacturers and distributors.
- Product Stability: Provides dependable preservation performance when properly formulated and stored.
- Technical Documentation: Product specifications, Certificate of Analysis (CoA), Safety Data Sheet (SDS), and relevant quality documentation can be provided subject to order requirements.
- Strategic Sourcing Value: Suitable for manufacturers seeking a scalable, internationally supplyable preservative with consistent quality and predictable procurement.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): Bulk — 20 MT
- Loading Capacity: Approximately 20–22 MT per 20-foot container, subject to packaging configuration, container regulations, and destination requirements
- Packaging: Standard 25 kg bags or customized bulk packaging upon request

Reviews
There are no reviews yet.