
1. Product Overview
Potassium Sorbate Food Grade is a high-purity preservative widely used to inhibit the growth of moulds, yeasts, and selected microorganisms in food and beverage formulations. Supplied as a practical 25kg bag, it supports consistent preservation, extended shelf life, and stable product quality across commercial production environments. Its broad application range and reliable performance make it a strategically important ingredient for food manufacturers seeking efficient, scalable preservation solutions.
2. Key Specifications & Technical Characteristics
- Chemical Composition: Potassium sorbate, the potassium salt of sorbic acid
- CAS Number: 590-00-1
- Grade: Food Grade
- Purity: Typically ≥99% on a dry basis, subject to supplier specification
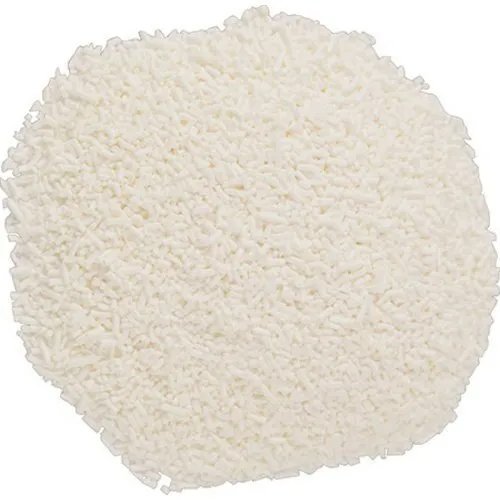
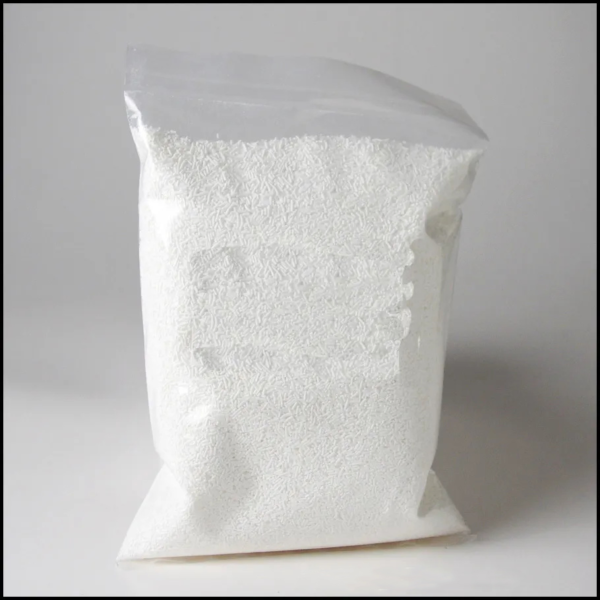
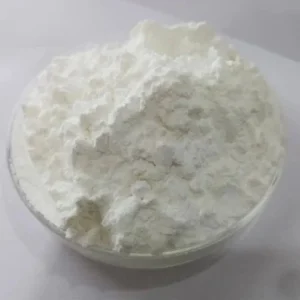
- Physical Form: White crystalline powder or granules
- Appearance: White to off-white
- Function: Antimicrobial food preservative, particularly effective against moulds and yeasts
- Solubility: Readily soluble in water
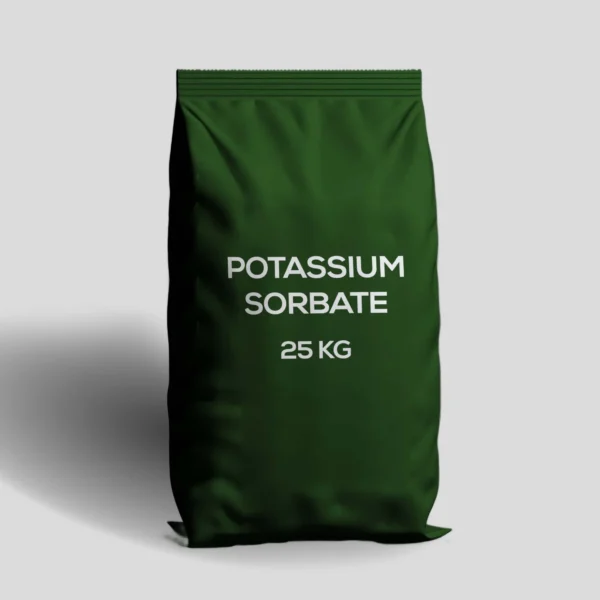
- Packaging: 25kg bags; bulk packaging available subject to commercial requirements
- Shelf Life: Typically 24–36 months when stored in a cool, dry environment in sealed original packaging
- Storage: Protect from moisture, heat, direct sunlight, and contamination
3. Core Industrial Applications
- Food & Beverage Manufacturing: Used in bakery products, sauces, dressings, jams, preserves, beverages, dairy products, and other formulated foods.
- Bakery & Confectionery: Helps control mould growth and supports longer shelf life during storage and distribution.
- Sauces & Processed Foods: Provides effective preservation while supporting product stability and consistent quality.
- Beverages: Used in selected beverage formulations where yeast and mould control is required.
- Industrial Food Processing: Suitable for large-scale manufacturing where dependable preservation and controlled formulation costs are essential.
Its effectiveness at relatively low application levels, broad formulation compatibility, and established food-industry use provide manufacturers with an efficient alternative to less versatile preservation systems.
4. Competitive Advantages
- Quality Consistency: Food-grade material designed for dependable performance across production batches.
- Supply Reliability: Suitable for recurring B2B procurement and large-volume sourcing programs.
- Logistics Capability: Standard 25kg packaging supports efficient handling, warehousing, container loading, and international distribution.
- Price Competitiveness: Bulk procurement enables commercially efficient sourcing for industrial-scale requirements.
- Product Stability: Helps extend shelf life and reduce losses associated with mould and yeast spoilage.
- Documentation: Product specifications, certificates of analysis, and relevant quality documentation can be provided subject to order and supplier availability.
- Strategic Sourcing Value: A scalable preservation ingredient for manufacturers seeking reliable quality, competitive supply, and international procurement efficiency.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Packaging: 25kg bags
- Loading Capacity: Approximately 20–25 MT per 20ft container, subject to packaging configuration, palletisation, and applicable container weight limits
- Supply: Bulk international B2B supply
Reviews
There are no reviews yet.