
- Product Overview
Potassium Sorbate is a high-performance food-grade preservative widely used to inhibit the growth of molds, yeasts, and selected microorganisms in food, beverage, pharmaceutical, and personal-care formulations. It provides reliable shelf-life extension while maintaining product quality, taste, and appearance when used within applicable formulation limits. Its broad compatibility, effective preservation performance, and ease of incorporation make it a strategically important ingredient for manufacturers seeking consistent product stability and reduced spoilage risk. - Key Specifications & Technical Characteristics
- Chemical Name: Potassium Sorbate
- Chemical Formula: C₆H₇KO₂
- CAS Number: 590-00-1
- Grade: Food Grade / Industrial Grade, subject to specification
- Purity: Typically ≥99%
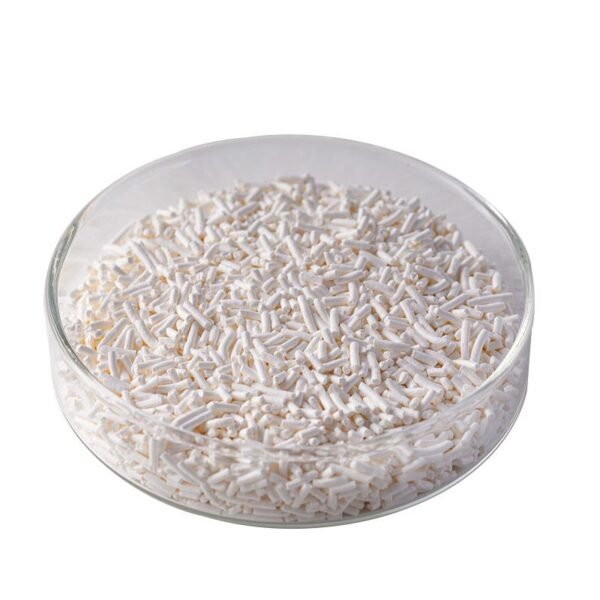
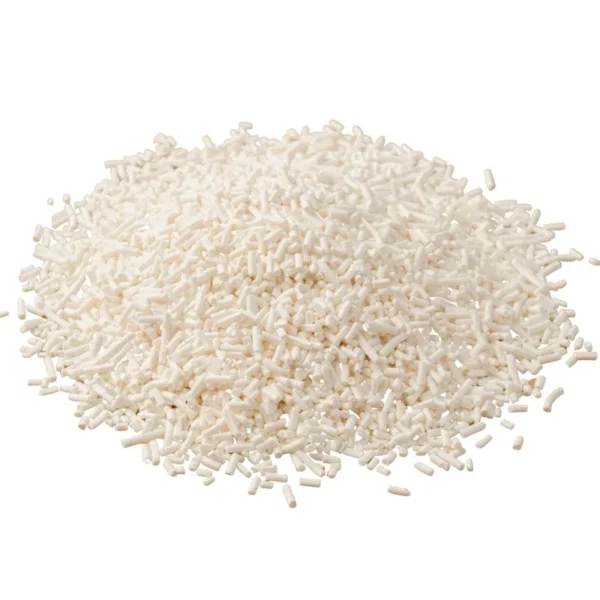
- Physical Form: White to off-white crystalline powder or granules
- Solubility: Highly soluble in water
- Function: Antimicrobial preservative, primarily effective against yeasts and molds
- Packaging Options: 25kg bags; bulk packaging available subject to order requirements
- Shelf Life: Typically 24 months when stored in sealed, dry conditions
- Storage: Cool, dry, well-ventilated environment away from moisture and direct sunlight
- Origin: Available from qualified international manufacturing and supply sources
- Core Industrial Applications
- Food & Beverage: Used in bakery products, beverages, sauces, dairy products, confectionery, jams, dressings, and processed foods to control yeast and mold growth.
- Pharmaceuticals: Applied as a preservative in selected formulations where microbial stability is required.
- Personal Care & Cosmetics: Used in creams, lotions, shampoos, and other water-containing formulations to support product preservation.
- Industrial Formulations: Suitable for applications requiring dependable antimicrobial protection and extended storage stability.
- Performance Advantage: Provides effective preservation at relatively low application levels, helping manufacturers reduce spoilage, maintain product consistency, and extend usable shelf life.
- Competitive Advantages
- Consistent Quality: High-purity material suitable for demanding manufacturing and formulation requirements.
- Reliable Supply: Structured sourcing supports continuity for recurring industrial and commercial orders.
- Logistics Capability: Bulk procurement and export-oriented supply options support international distribution requirements.
- Price Competitiveness: Suitable for cost-conscious manufacturers seeking dependable preservative performance at scale.
- Sustainability: Efficient preservative performance can help reduce product spoilage and associated material waste.
- Technical Documentation: Product specifications, certificates of analysis, and supporting documentation can be provided subject to order and supplier requirements.
- Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Approximately 20–25 MT per 20ft container, subject to packaging configuration, loading restrictions, and final shipping requirements.

Reviews
There are no reviews yet.