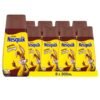
1. Product Overview
Nesquik Chocolate Milk – 300 ml is a ready-to-drink chocolate-flavoured milk beverage designed for convenient consumption across retail, foodservice, hospitality, and institutional channels. Its practical single-serve format supports efficient merchandising, distribution, and on-the-go consumption. The product combines a familiar chocolate flavour profile with the convenience of a ready-to-drink dairy beverage, making it commercially attractive for wholesalers and distributors. Its established consumer recognition and scalable pack format support dependable demand across international B2B supply markets.
2. Key Specifications & Technical Characteristics
- Product Type: Ready-to-drink chocolate milk beverage
- Brand: Nesquik
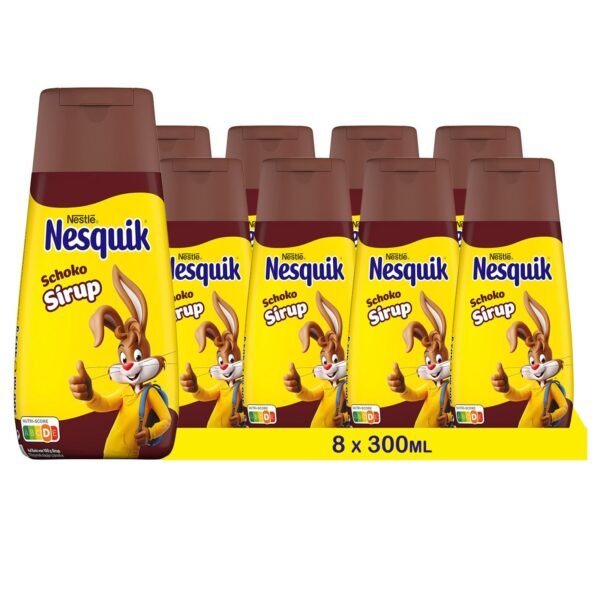
- Net Volume: 300 ml per unit
- Composition: Milk/dairy ingredients, water, cocoa/chocolate flavouring, sweetening ingredients, and permitted stabilising or nutritional ingredients depending on market formulation
- Grade: Food Grade
- Physical Form: Liquid beverage
- Colour: Chocolate brown
- Flavour: Chocolate
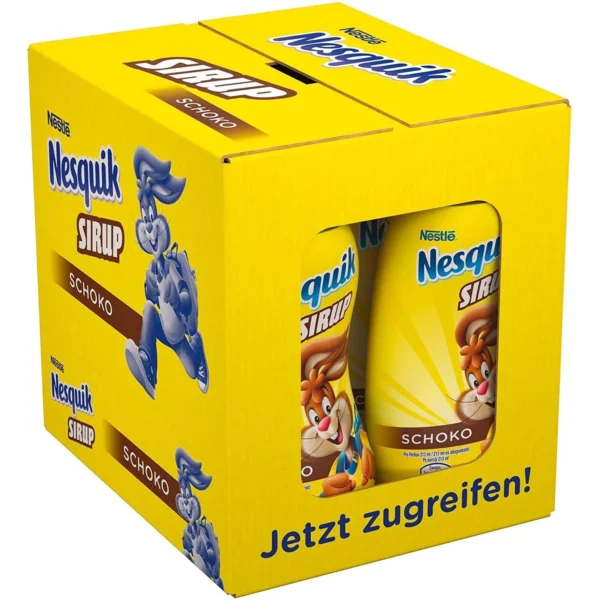
- Packaging: Individual 300 ml retail-ready containers; outer cartons/cases available according to supplier configuration
- Shelf Life: Subject to manufacturer batch specification, production date, storage conditions, and applicable market requirements
- Storage: Store according to the manufacturer’s stated temperature and handling requirements
- Documentation: Product specification, batch information, packaging details, and applicable food-safety documentation available subject to supplier and destination requirements
3. Core Industrial Applications
- Food & Beverage Distribution: Suitable for wholesalers, importers, distributors, and retail supply chains requiring established branded beverages.
- Retail & Convenience: The 300 ml format is suited to supermarkets, convenience stores, vending operations, and grab-and-go channels.
- Foodservice & Hospitality: Can support hotels, cafés, catering operators, schools, workplaces, and institutional beverage programmes where permitted.
- Bulk Resale & Export: Standardised single-serve packaging simplifies inventory management, case distribution, merchandising, and international wholesale procurement.
- Operational Advantages: Ready-to-drink presentation eliminates preparation requirements, reduces serving complexity, and supports fast product turnover compared with beverages requiring on-site preparation.
4. Competitive Advantages
- Quality Consistency: Established branded formulation and standardised retail packaging support consistent product presentation and consumer expectations.
- Supply Reliability: Suitable for structured wholesale procurement and repeat distribution programmes, subject to stock and supplier availability.
- Logistics Capability: Compact 300 ml units and case-packed distribution support efficient warehousing, palletisation, transportation, and retail handling.
- Price Competitiveness: Bulk procurement can provide commercially efficient purchasing for distributors, wholesalers, and institutional buyers.
- Market Recognition: The established Nesquik brand can support product visibility and consumer familiarity across suitable sales channels.
- Sustainability: Packaging and logistics efficiencies can be supported through responsible warehousing, pallet optimisation, and consolidated shipments where applicable.
- Technical & Commercial Documentation: Batch, packaging, specification, and food-safety documentation can be supplied subject to supplier and destination requirements.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Approximately 20–24 MT per standard container, subject to packaging configuration, palletisation, container restrictions, and applicable shipping requirements
Reviews
There are no reviews yet.