
1. Product Overview
Flexible Packaging Film is a high-performance polymer-based film engineered for the packaging, protection, and preservation of a wide range of consumer, food, industrial, and commercial products. Manufactured from materials such as polyethylene (PE), polypropylene (PP), polyester (PET), or multilayer polymer structures, it provides excellent flexibility, sealing performance, barrier protection, and mechanical strength. Its lightweight construction helps reduce material consumption, transportation costs, and overall packaging weight while maintaining reliable product protection. Strategically, it is a high-demand packaging material supporting efficient, scalable, and cost-effective packaging operations across global supply chains.
2. Key Specifications & Technical Characteristics
- Material Composition: PE, PP, PET, or customized multilayer polymer structures according to application requirements.
- Grade: Industrial, food-packaging, commercial, or customized grade subject to specification.
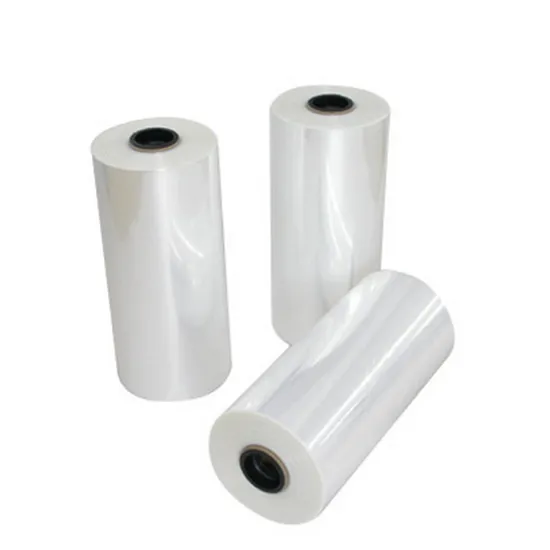
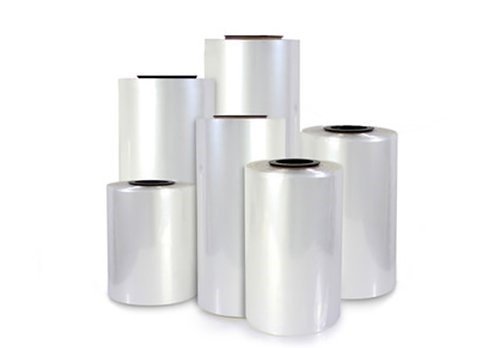
- Form: Flexible rolls, reels, sheets, or converted film.
- Appearance: Clear, translucent, white, or customized color.
- Thickness: Available in various thicknesses according to packaging and performance requirements.
- Width: Customizable to customer production and converting requirements.
- Surface: Smooth, printable, sealable, laminated, or treated as required.
- Mechanical Properties: Designed for good tensile strength, puncture resistance, flexibility, and dimensional stability.
- Packaging: Export-grade rolls packed with protective wrapping, cartons, pallets, or customized bulk packaging.
- Shelf Life: Typically up to 12 months when stored in a cool, dry environment away from direct sunlight and excessive heat.
- Customization: Thickness, width, printing, lamination, barrier properties, and roll dimensions can be supplied according to approved technical specifications.
3. Core Industrial Applications
- Food & Beverage Packaging: Used for wrapping, sealing, laminating, and protecting food products against moisture, contamination, and handling damage.
- Consumer Goods: Suitable for packaging household products, personal-care products, retail goods, and general merchandise.
- Industrial Packaging: Used for protective wrapping, bundling, lining, and secondary packaging of industrial products.
- Agricultural Packaging: Applied in packaging and protecting agricultural products and related materials.
- Pharmaceutical & Healthcare Packaging: Used in suitable grades for protective and hygienic packaging applications.
- E-Commerce & Logistics: Provides lightweight protection and secure product containment during storage, handling, and transportation.
Its combination of flexibility, strength, sealing capability, and low weight enables efficient high-speed packaging while reducing material and transportation costs compared with heavier rigid packaging alternatives.
4. Competitive Advantages
- Quality Consistency: Controlled manufacturing specifications support uniform thickness, strength, sealing performance, and reliable processing.
- Supply Reliability: Structured bulk sourcing supports consistent availability for manufacturers, distributors, and large-scale packaging operations.
- Logistics Capability: Export-oriented packaging and bulk shipment solutions facilitate efficient international transportation and containerized supply.
- Price Competitiveness: High-volume procurement and optimized packaging-to-product ratios provide opportunities for competitive landed costs.
- Sustainability Benefits: Lightweight film can reduce packaging weight and transportation requirements, while recyclable polymer structures can support resource-efficiency objectives where appropriate recycling infrastructure exists.
- Technical Support: Product specifications, technical documentation, certificates, and customized film configurations can be provided according to buyer and application requirements.
- Strategic Sourcing Value: Suitable for buyers seeking dependable quality, scalable supply, customized specifications, and commercially competitive procurement for continuous packaging operations.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK — 20 MT
- Loading Capacity: Approximately 18–22 MT per container, subject to film specifications, roll dimensions, packaging configuration, and applicable container weight limits.
- Supply Format: Bulk commercial supply with export-ready packaging.
- Specification: Customized according to buyer requirements and mutually approved technical specifications.


Reviews
There are no reviews yet.