
1. Product Overview
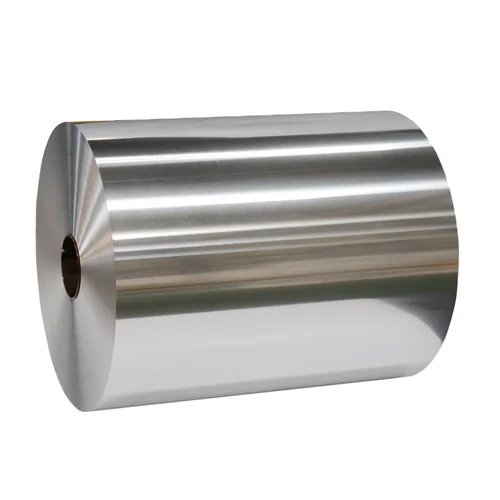
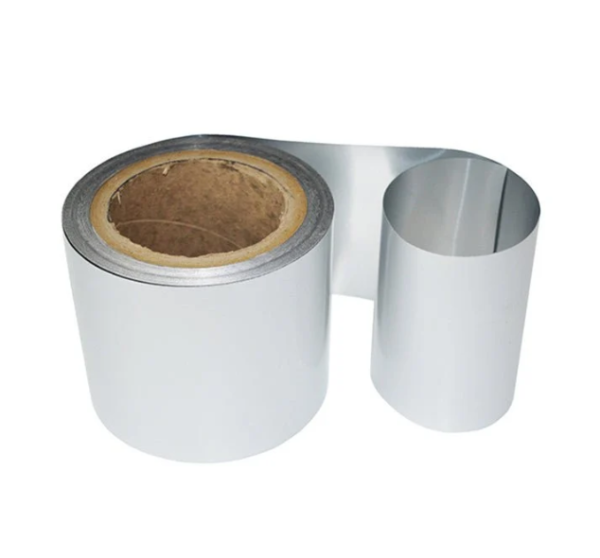
Aluminium Foil Packaging Rolls are high-performance aluminium-based packaging materials engineered for reliable protection, sealing, wrapping, and barrier applications across industrial and commercial operations. They provide an effective barrier against moisture, oxygen, light, contaminants, and external environmental factors, helping preserve product integrity and shelf life. Their flexibility, durability, and excellent barrier performance make them strategically important for food, pharmaceutical, chemical, and consumer-goods packaging. Consistent quality and scalable bulk supply support efficient procurement for demanding B2B operations.
2. Key Specifications & Technical Characteristics
- Material Composition: Aluminium foil, typically supplied as high-purity aluminium suitable for packaging applications.
- Grade: Packaging-grade aluminium foil; specifications can be customized according to application and buyer requirements.
- Purity: Typically high-purity aluminium suitable for food, pharmaceutical, and industrial packaging.
- Form: Continuous rolls with smooth, uniform foil surface.
- Color/Finish: Metallic silver/aluminium finish; available in plain or application-specific formats.
- Thickness: Available in multiple thickness options according to packaging, forming, and barrier requirements.
- Width: Customizable to meet specific machinery and packaging-line requirements.
- Barrier Performance: Excellent resistance to moisture, oxygen, light, odors, and contaminants.
- Mechanical Characteristics: Flexible, lightweight, tear-resistant, and suitable for forming, wrapping, laminating, and sealing applications.
- Packaging Options: Export-standard protective rolls, cartons, pallets, or customized industrial packaging.
- Shelf Life: Long-term shelf stability when stored in dry, clean conditions away from excessive humidity and contamination.
- Documentation: Product specifications, technical data, certificates, and other documentation can be provided subject to order requirements.
3. Core Industrial Applications
- Food & Beverage Packaging: Used for wrapping, sealing, lidding, pouches, sachets, and multilayer packaging to protect products from moisture, oxygen, light, and contamination.
- Pharmaceutical Packaging: Suitable for blister packs, sachets, strip packaging, and other applications requiring strong barrier protection and product integrity.
- Household & Consumer Products: Used for flexible packaging, wrapping, and protective applications where durability and barrier performance are essential.
- Industrial & Chemical Packaging: Provides protective wrapping and barrier layers for selected industrial materials and products.
- Insulation & Specialized Packaging: Utilized where lightweight construction, reflective properties, and resistance to environmental exposure are required.
- Performance Advantage: Compared with many conventional packaging films, aluminium foil offers superior barrier protection while remaining lightweight, flexible, and compatible with high-speed converting and packaging processes.
4. Competitive Advantages
- Quality Consistency: Controlled thickness, surface quality, dimensional accuracy, and material performance support dependable production results.
- Supply Reliability: Structured bulk sourcing supports repeat procurement and continuity for industrial buyers.
- Logistics Capability: Export-oriented packaging and containerized shipment options facilitate efficient international distribution.
- Price Competitiveness: Competitive bulk pricing and scalable supply can help optimize total packaging procurement costs.
- Sustainability: Aluminium is highly recyclable, supporting circular-material strategies when appropriate collection and recycling systems are available.
- Technical Support: Product specifications, quality documentation, and application-related technical information can be supplied according to buyer requirements.
- Strategic Sourcing Value: A combination of barrier performance, customization, scalable supply, and procurement efficiency makes Aluminium Foil Packaging Rolls a dependable choice for industrial packaging programs.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20 MT
- Loading Capacity: Approximately 20–25 MT per 20-foot container, subject to roll dimensions, packaging configuration, product specifications, and applicable container weight limits.
- Packaging: Export-standard industrial packaging with customized packing options available upon request.
- Supply Terms: Bulk and contract supply available for qualified B2B buyers.


Reviews
There are no reviews yet.