
1. Product Overview
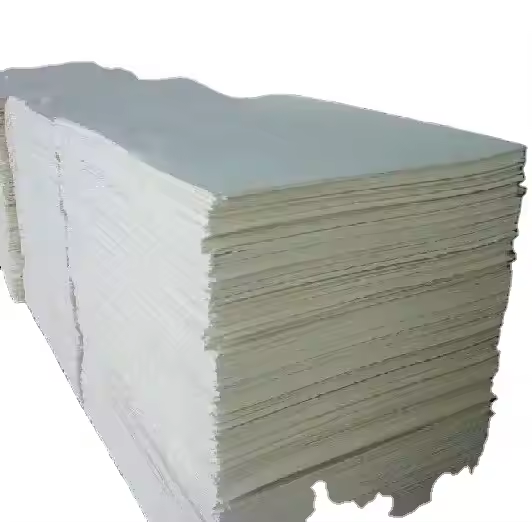
Bleached Kraft Pulp is a high-quality, chemically processed wood pulp designed for the production of premium paper, tissue, packaging, and specialty cellulose-based products. Its high brightness, clean fiber structure, and consistent formation characteristics support efficient industrial paper manufacturing and superior finished-product quality. The product offers reliable performance, excellent strength, and process stability, making it a strategically important raw material for manufacturers seeking consistent output and optimized production costs.
2. Key Specifications & Technical Characteristics
- Material Composition: Predominantly purified cellulose fibers derived from sustainably managed wood sources.
- Grade: Bleached Kraft Pulp, industrial/paper-making grade.
- Brightness: Typically high brightness, commonly around 88% ISO or as specified by grade.
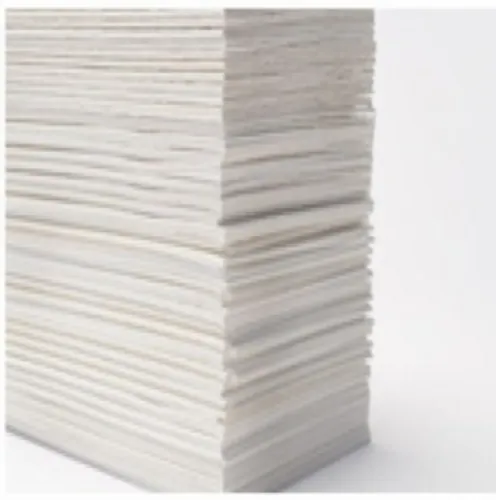
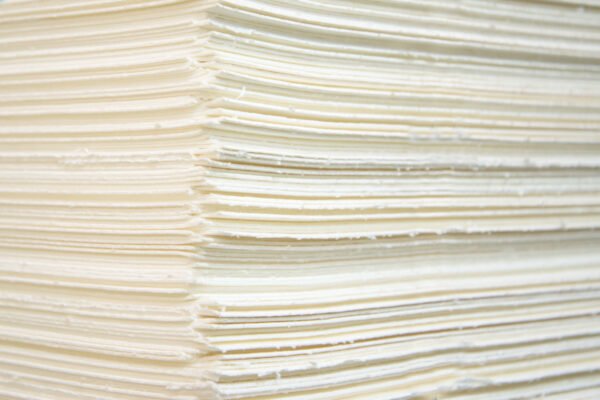
- Form: Dried, compressed pulp sheets or bales.
- Color: White to bright white.
- Fiber Characteristics: High-strength, clean, uniform cellulose fibers suitable for industrial paper processing.
- Moisture: Typically controlled to meet standard pulp industry specifications.
- Purity: High cellulose content with controlled levels of residual lignin, ash, and extractives.
- Packaging: Standardized export-grade wrapped bales, suitable for containerized and bulk transportation.
- Shelf Life: Long shelf life when stored in dry, clean, and well-ventilated conditions away from moisture and contamination.
3. Core Industrial Applications
- Paper Manufacturing: Used in printing, writing, office, publishing, and specialty papers where brightness, strength, and printability are essential.
- Tissue & Hygiene Products: Supports production of facial tissue, toilet tissue, paper towels, and other absorbent products requiring softness and consistent formation.
- Packaging & Board: Used in selected packaging papers and paperboard formulations to improve fiber strength and appearance.
- Specialty Cellulose Products: Suitable for applications requiring refined and purified cellulose fibers.
- Industrial Processing: Its consistent fiber quality enables efficient refining, blending, forming, and converting operations while supporting predictable production performance.
4. Competitive Advantages
- Quality Consistency: Uniform fiber characteristics and controlled brightness support stable production and consistent finished-product quality.
- Supply Reliability: Suitable for structured industrial procurement and recurring bulk requirements.
- Logistics Capability: Export-grade bale packaging facilitates efficient container loading, handling, storage, and international transportation.
- Price Competitiveness: Bulk sourcing provides opportunities for cost optimization across high-volume manufacturing operations.
- Sustainability: Can support responsible sourcing strategies when supplied from certified or sustainably managed forestry sources.
- Technical Documentation: Product specifications, quality documentation, and relevant compliance certificates can be provided according to buyer and destination-market requirements.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK — 20 MT
- Loading Capacity: Approximately 20–25 MT per 20-foot container, subject to bale configuration, product density, and applicable container weight restrictions.


Reviews
There are no reviews yet.