
1. Product Overview
Stevia Extract 95% Steviol Glycosides is a high-purity, plant-derived sweetening ingredient formulated for food, beverage, nutraceutical, and functional-product applications. Its concentrated sweetness enables manufacturers to reduce or replace conventional sugar while supporting reduced-calorie product formulations. The 95% steviol glycoside specification provides a strong balance of sweetness intensity, formulation efficiency, and consistent performance for commercial-scale production. Supplied in 25kg bags, it is well suited to professional B2B ingredient sourcing and bulk manufacturing requirements.
2. Key Specifications & Technical Characteristics
- Product: Stevia Extract 95% Steviol Glycosides
- Active Component: Steviol glycosides derived from Stevia rebaudiana
- Purity: 95% steviol glycosides
- Grade: Food Grade
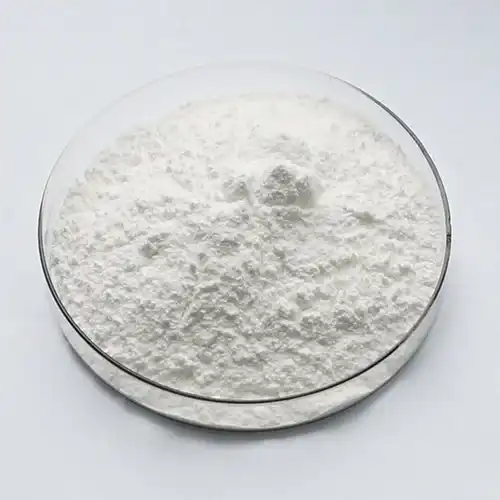
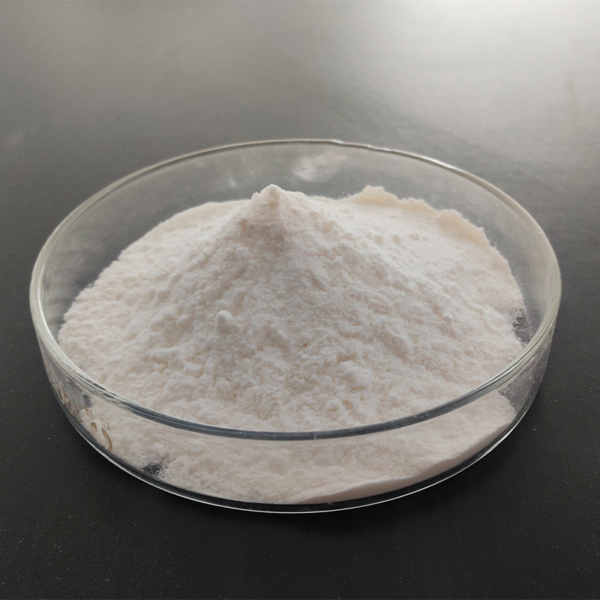
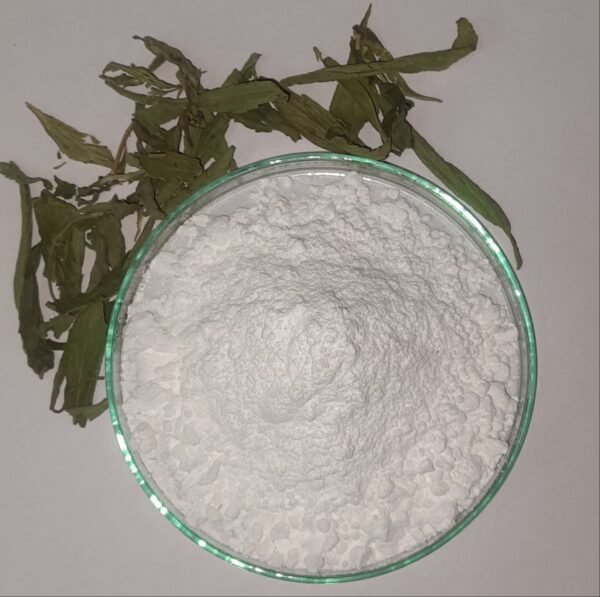
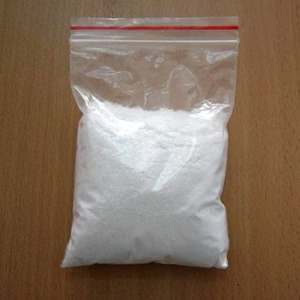
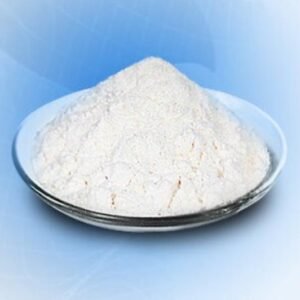
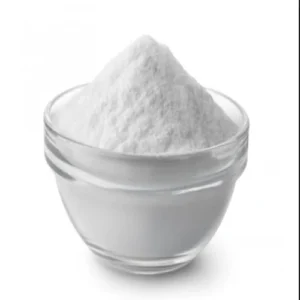
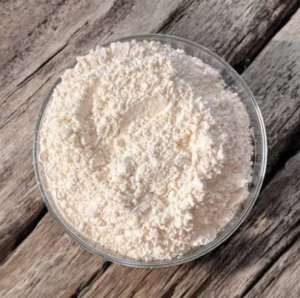
- Form: Fine powder
- Colour: Typically white to off-white
- Solubility: Suitable for incorporation into a range of food and beverage formulations
- Packaging: 25kg bag
- Shelf Life: Typically 24 months when stored under recommended conditions
- Storage: Keep sealed in a cool, dry place away from moisture, heat, and direct sunlight
- Origin: Subject to supply and production batch
- Documentation: Product specification and quality documentation available upon request
3. Core Industrial Applications
- Food & Beverage Manufacturing: Used as a high-intensity sweetener in beverages, dairy products, confectionery, sauces, bakery products, and formulated foods.
- Reduced-Sugar Products: Supports sugar-reduction strategies while maintaining a sweet taste profile.
- Nutraceuticals & Functional Foods: Suitable for sweetening supplements, nutritional products, and functional formulations.
- Powdered & Dry Mixes: Can be incorporated into beverage powders, instant mixes, and other dry-blend formulations.
- Commercial Advantage: Its high concentration allows manufacturers to achieve sweetness using relatively small inclusion rates, supporting formulation efficiency and ingredient-cost management.
4. Competitive Advantages
- High Purity: 95% steviol glycosides provide concentrated sweetening performance for industrial formulations.
- Consistent Quality: Specification-focused supply supports repeatable production and formulation control.
- Supply Reliability: Bulk-oriented sourcing is suitable for manufacturers, distributors, and international ingredient buyers.
- Logistics Capability: 25kg commercial packaging facilitates handling, storage, palletisation, and international shipment.
- Cost Efficiency: High sweetness intensity can reduce the quantity of sweetener required compared with conventional sugar-based formulations.
- Plant-Derived Ingredient: Provides manufacturers with a naturally sourced sweetening option for products positioned around sugar reduction.
- Technical Documentation: Product specifications and supporting documentation can be provided to assist procurement and quality-control processes.
5. Commercial & Supply Information
- Packaging: 25kg bag
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Approximately 20–25 MT per 20ft container, subject to packaging configuration, palletisation, and applicable shipping limits
- Supply: Bulk international B2B supply available
Reviews
There are no reviews yet.