
1. Product Overview
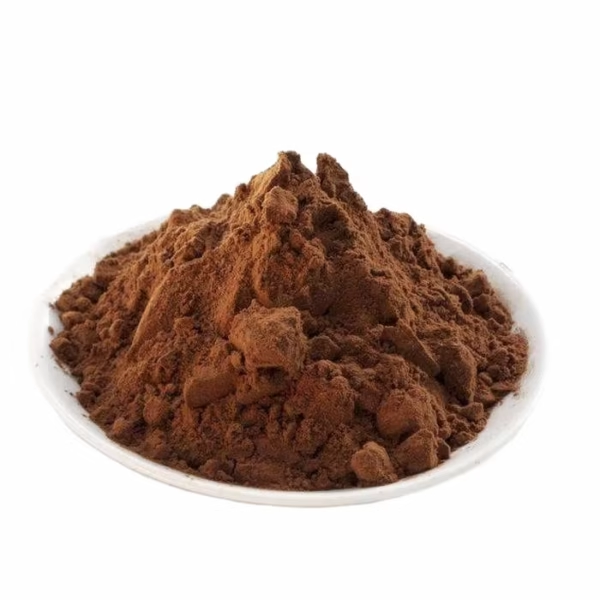
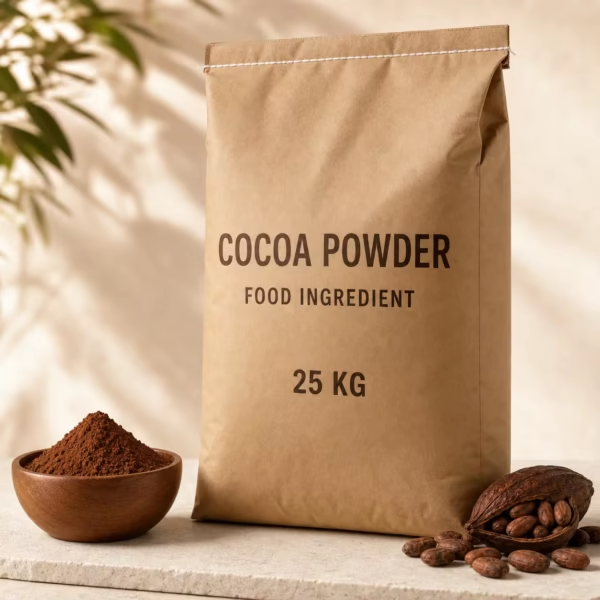
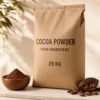
Cocoa Powder Alkalized Food Grade is a premium, processed cocoa ingredient designed to deliver rich cocoa flavor, deep color, and consistent performance across food and beverage applications. It is produced by alkalizing cocoa powder to modify its acidity, enhance color development, and improve dispersibility in formulations. The product is widely used by manufacturers of chocolate, bakery products, beverages, confectionery, dairy products, and dessert mixes. Supplied in convenient 25kg bags, it provides industrial buyers with a dependable ingredient for consistent, scalable production.
2. Key Specifications & Technical Characteristics
- Product: Cocoa Powder Alkalized Food Grade
- Grade: Food Grade
- Processing: Alkalized/Dutch-processed cocoa powder
- Form: Fine, free-flowing powder
- Color: Brown to dark brown, depending on alkalization level
- Flavor & Aroma: Characteristic rich cocoa flavor and aroma
- Composition: Cocoa solids with approved food-grade alkalizing treatment
- Particle Size: Fine powder suitable for industrial food processing
- Moisture: Typically controlled to meet food-industry specifications
- Packaging: 25kg food-grade bags
- Shelf Life: Typically 12–24 months when stored under recommended conditions
- Storage: Store in a cool, dry, clean environment away from moisture, heat, odors, and direct sunlight
3. Core Industrial Applications
- Bakery & Biscuits: Used in cakes, cookies, brownies, pastries, and chocolate-flavored baked goods for rich flavor and enhanced color.
- Chocolate & Confectionery: Supports the production of chocolate products, fillings, coatings, compound chocolate, and confectionery formulations.
- Beverages: Used in cocoa drinks, chocolate beverages, instant drink mixes, and powdered beverage formulations.
- Dairy & Desserts: Suitable for flavored milk, ice cream, puddings, dessert mixes, and other cocoa-based dairy products.
- Food Manufacturing: Provides consistent cocoa color, flavor, and functionality across large-scale formulations.
- Performance Advantage: Alkalization can provide improved color intensity, reduced acidity, smoother flavor profiles, and better dispersion compared with natural cocoa powder in applications requiring darker color and a milder cocoa profile.
4. Competitive Advantages
- Quality Consistency: Controlled processing supports consistent color, flavor, texture, and formulation performance across production batches.
- Supply Reliability: Suitable for regular bulk procurement and continuous industrial manufacturing requirements.
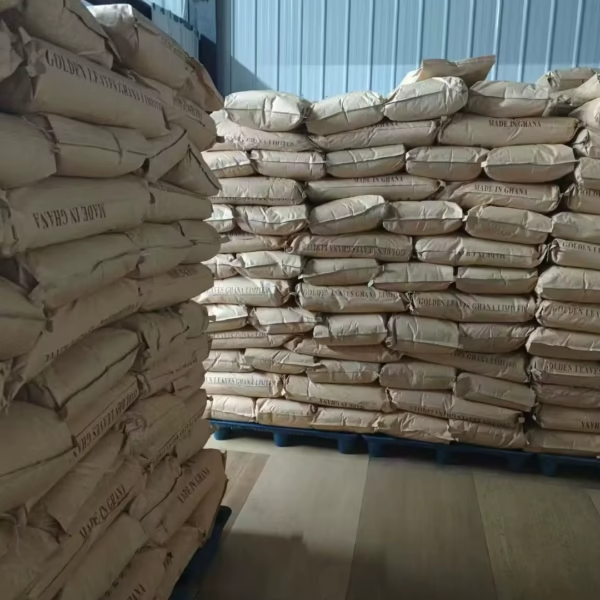
- Logistics Capability: Standard 25kg packaging facilitates handling, warehousing, palletization, and international shipment.
- Price Competitiveness: Bulk sourcing provides opportunities for cost-efficient procurement and improved supply-chain economics.
- Versatile Performance: Suitable for diverse food and beverage formulations requiring dependable cocoa functionality.
- Sustainability: Efficient bulk packaging and consolidated shipments can support more streamlined industrial supply operations.
- Technical Documentation: Product specifications, quality documentation, and relevant food-safety documentation can be provided according to supply requirements.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Packaging: 25kg bags
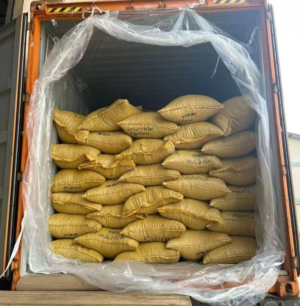
- Loading Capacity: Approximately 20–24 MT per 20ft container, depending on packaging configuration, palletization, and applicable shipping limits
- Supply: Bulk and international B2B supply available
Reviews
There are no reviews yet.