
1. Product Overview
Coffee Creamer Non-Dairy Food Grade is a powdered creaming ingredient formulated to enhance the body, smoothness, whiteness, and overall sensory profile of coffee and other beverage applications. Designed for commercial food and beverage processing, it provides consistent dispersion and a convenient alternative to liquid dairy cream. Its dry format supports efficient storage, handling, transportation, and large-scale production. The product is strategically suited to manufacturers, beverage processors, cafés, hospitality suppliers, and bulk distributors seeking dependable, scalable creaming functionality.
2. Key Specifications & Technical Characteristics
- Product Type: Non-dairy powdered coffee creamer
- Grade: Food Grade
- Typical Composition: Glucose syrup solids, vegetable fat, milk-derived proteins or permitted dairy solids where applicable, stabilizers/emulsifiers, and anti-caking agents
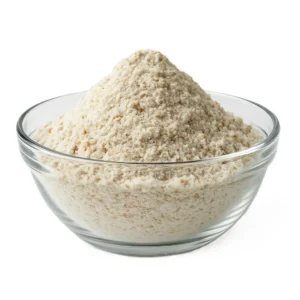
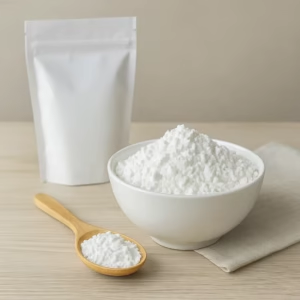
- Physical Form: Free-flowing powder
- Colour: White to creamy white
- Flavour/Aroma: Mild, neutral creamy profile suitable for coffee and beverage formulations
- Functional Characteristics: Provides creaminess, body, whitening, and improved mouthfeel
- Solubility: Designed for efficient dispersion in hot beverages
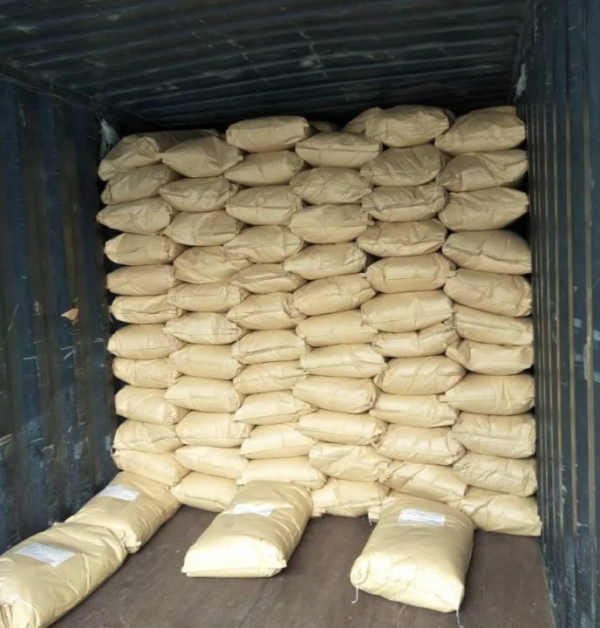
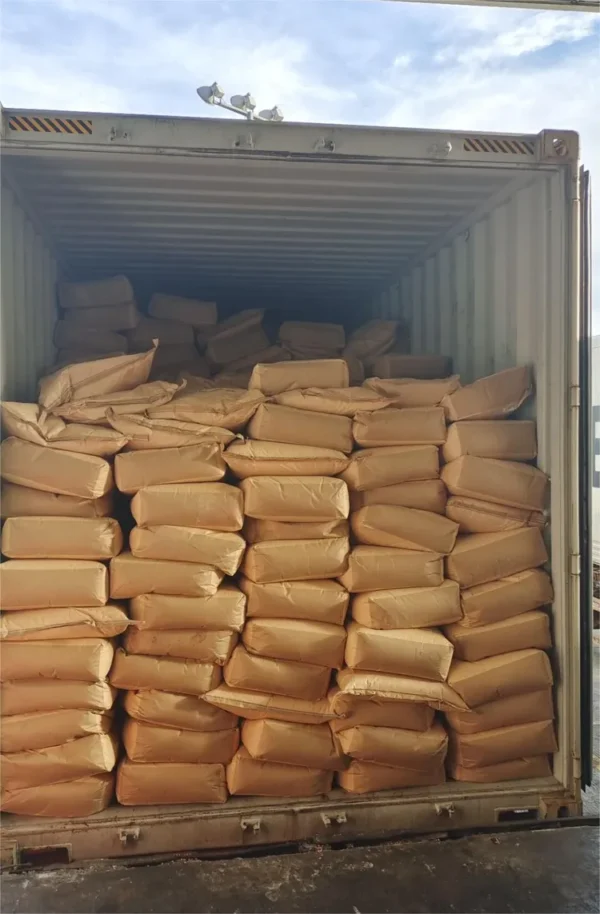
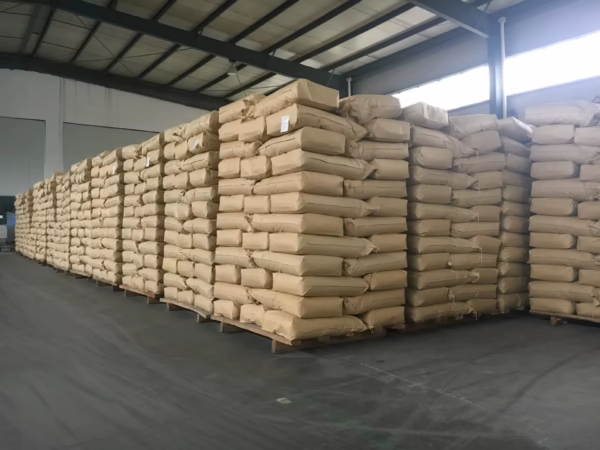
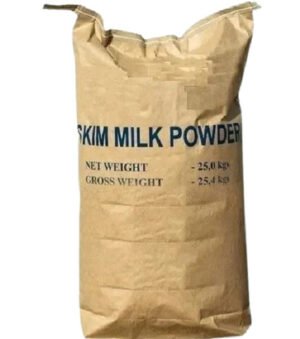
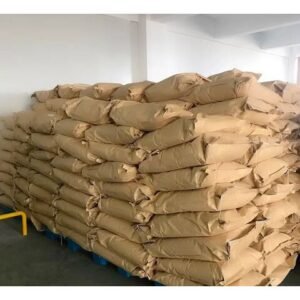
- Packaging: 25kg food-grade bags
- Shelf Life: Typically 12–24 months when stored unopened under recommended conditions; subject to the manufacturer’s specification
- Storage: Store in a cool, dry, clean environment away from direct sunlight, moisture, and strong odours
- Documentation: Product specification, certificate of analysis, and relevant food-safety documentation available subject to supply and batch requirements
3. Core Industrial Applications
- Coffee & Beverage Manufacturing: Used in instant coffee, vending beverages, cappuccino mixes, latte preparations, and powdered beverage formulations.
- Foodservice & Hospitality: Suitable for hotels, cafés, restaurants, catering operations, and institutional beverage programs requiring consistent portion and formulation control.
- Instant Beverage Production: Supports large-scale production of dry beverage mixes by delivering consistent creaminess and whitening without the handling requirements of liquid dairy cream.
- Food Ingredient Blending: Can be incorporated into powdered formulations where improved texture, mouthfeel, and creamy flavour characteristics are required.
- Commercial Advantage: The powdered format reduces refrigeration requirements compared with liquid cream while supporting convenient bulk storage, transportation, and dosing.
4. Competitive Advantages
- Quality Consistency: Uniform powdered format supports repeatable formulation and beverage performance across production batches.
- Supply Reliability: Suitable for structured bulk procurement and recurring B2B supply programs.
- Logistics Capability: 25kg bag packaging facilitates palletisation, container loading, warehouse handling, and international distribution.
- Price Competitiveness: Bulk procurement can provide cost efficiencies for manufacturers, distributors, and high-volume commercial users.
- Operational Efficiency: Dry, shelf-stable handling can simplify storage and transportation compared with refrigerated liquid creaming ingredients.
- Sustainability Considerations: Dry-format logistics can reduce cold-chain requirements and associated handling demands.
- Technical Documentation: Product specifications and batch documentation can be provided to support procurement, quality assurance, and regulatory review.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Packaging: 25kg bags
- Loading Capacity: Approximately 20–24 MT per standard container, subject to packaging configuration, container payload restrictions, and final loading plan
- Supply Format: Bulk B2B / wholesale supply
Reviews
There are no reviews yet.