
1. Product Overview
Granulated White Sugar Refined Food Grade is a high-purity crystalline sucrose product manufactured for consistent sweetness, solubility, and reliable performance across food and beverage applications. It is widely used in confectionery, bakery, beverages, dairy products, food processing, and industrial food manufacturing. Its uniform granulation, clean appearance, and dependable quality make it a practical choice for high-volume commercial production. As a globally traded staple commodity, refined white sugar supports stable procurement and efficient formulation across diverse food-processing operations.
2. Key Specifications & Technical Characteristics
- Product: Granulated White Sugar, Refined Food Grade
- Chemical Composition: Predominantly sucrose (C₁₂H₂₂O₁₁)
- Grade: Food Grade, Refined
- Purity: Typically ≥99.8% sucrose, subject to specification and supplier certificate
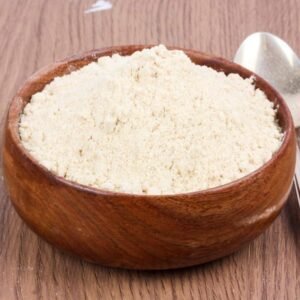
- Physical Form: Free-flowing crystalline granules
- Color: White to bright white
- Taste & Odor: Clean, sweet taste with no abnormal odor
- Solubility: Readily soluble in water
- Granulation: Uniform crystal size suitable for food-processing applications
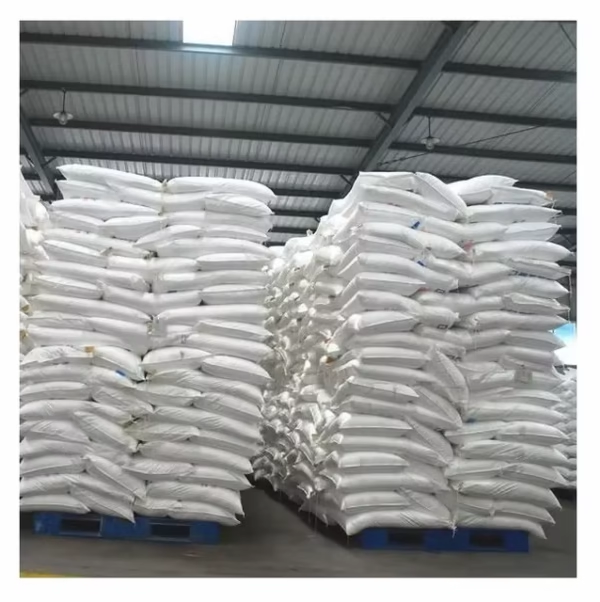
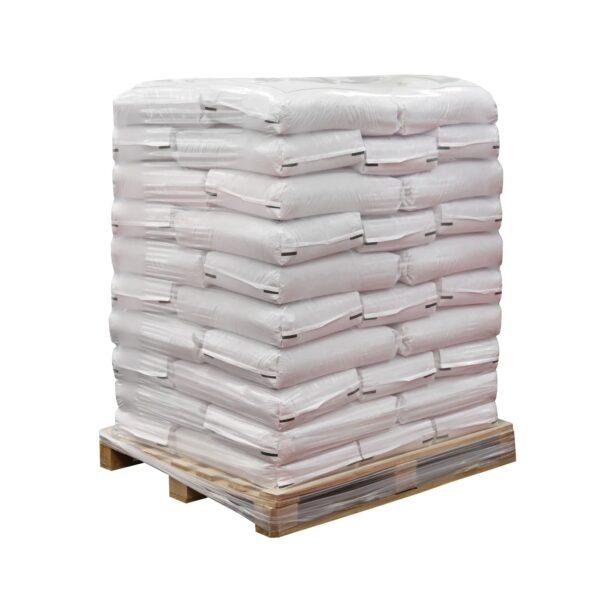
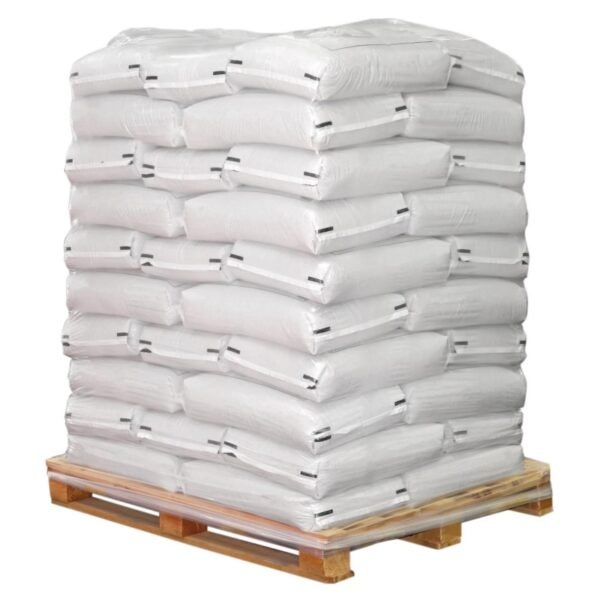
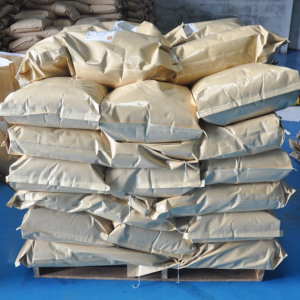
- Packaging: 25kg food-grade bags; bulk packaging available subject to order requirements
- Shelf Life: Typically 24 months when stored in a cool, dry, clean environment away from moisture and contamination
- Documentation: Certificate of Analysis (COA) and relevant quality documentation available subject to supply specification
3. Core Industrial Applications
- Beverage Manufacturing: Used in soft drinks, juices, syrups, energy drinks, and flavored beverages for controlled sweetness and formulation consistency.
- Bakery & Confectionery: Essential for cakes, biscuits, pastries, candies, chocolates, fondants, and other sweetened products.
- Dairy & Food Processing: Used in yogurts, desserts, preserves, sauces, jams, and processed foods.
- Pharmaceutical & Nutraceutical Processing: Suitable as a formulation ingredient where food-grade refined sucrose is required.
- Industrial Food Production: Supports high-volume manufacturing where consistent granulation, predictable dissolution, and standardized sweetness are commercially important.
- Operational Advantages: Uniform crystals promote predictable dosing and rapid dissolution, helping manufacturers maintain consistent formulations and efficient production processes.
4. Competitive Advantages
- Quality Consistency: Refined food-grade quality with uniform crystalline structure and consistent sweetness.
- Supply Reliability: Suitable for recurring commercial procurement and high-volume sourcing programs.
- Logistics Capability: Available in standardized 25kg bags for efficient handling, warehousing, palletization, and international shipment.
- Price Competitiveness: Bulk procurement can support competitive landed costs for distributors, manufacturers, and institutional buyers.
- Sustainability: Efficient bulk logistics and standardized packaging can help optimize transportation and material usage across large-volume supply chains.
- Technical Documentation: Product specifications, COA, and applicable quality documentation can be provided to support commercial qualification and procurement requirements.
- Strategic Sourcing Value: A dependable commodity input suitable for manufacturers seeking consistent quality, scalable supply, and predictable procurement planning.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Approximately 20–25 MT per 20-foot container, subject to packaging configuration, container payload limits, and shipping requirements
- Packaging: 25kg bags
Reviews
There are no reviews yet.