
1. Product Overview
Xanthan Gum Food Grade is a high-performance food hydrocolloid used as a thickening, stabilizing, emulsifying, and viscosity-control agent across a wide range of food and beverage formulations. It provides reliable texture, suspension, and consistency even under varying processing conditions, making it valuable for sauces, dressings, beverages, bakery products, dairy alternatives, and processed foods. Its efficient performance at relatively low inclusion levels supports formulation optimization, product consistency, and cost-effective manufacturing. Supplied in convenient 25kg bags, it is well suited to professional food processors, ingredient distributors, and international bulk procurement.
2. Key Specifications & Technical Characteristics
- Product: Xanthan Gum Food Grade
- Material: Microbial fermentation-derived polysaccharide hydrocolloid
- Grade: Food Grade
- Function: Thickener, stabilizer, emulsifier, suspending and viscosity-control agent
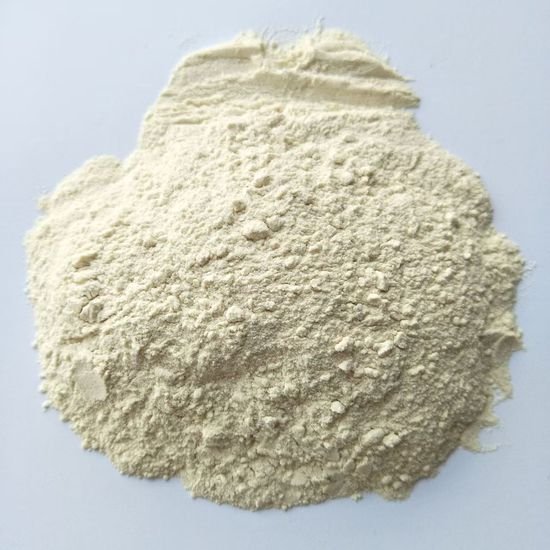
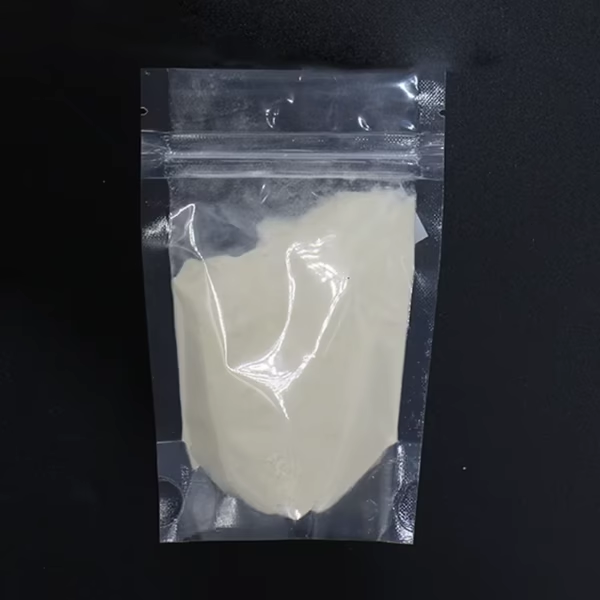
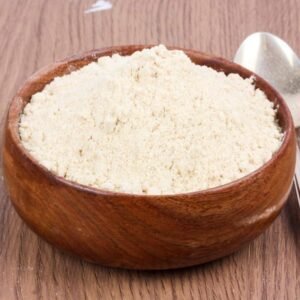
- Form: Fine powder
- Color: Typically cream to off-white
- Solubility: Dispersible in water and capable of producing high viscosity
- Texture Control: Provides consistent viscosity and stabilization across a broad range of formulations
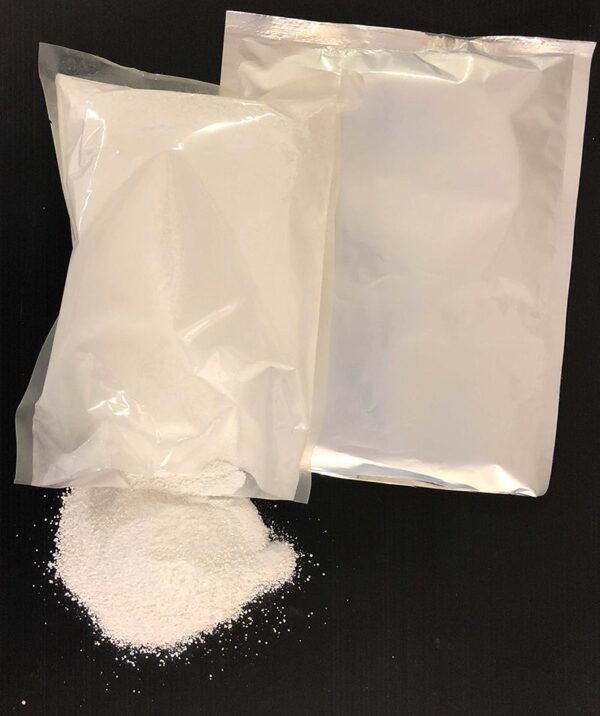
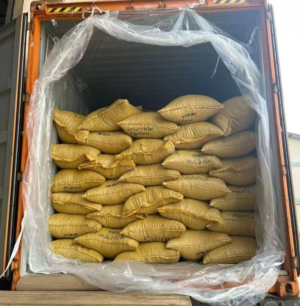
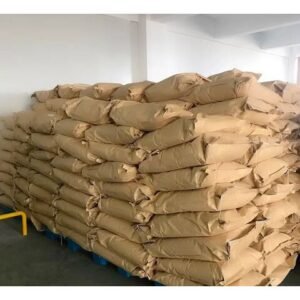
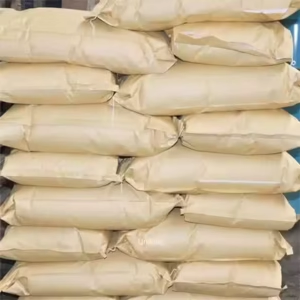
- Packaging: 25kg industrial-grade bags
- Shelf Life: Typically up to 24 months when stored in a cool, dry environment in sealed original packaging
- Storage: Protect from moisture, heat, direct sunlight, and contamination
3. Core Industrial Applications
- Food & Beverage Manufacturing: Used in sauces, ketchup, mayonnaise, salad dressings, gravies, beverages, and ready-to-eat formulations for viscosity and stability.
- Bakery & Gluten-Free Products: Improves dough handling, structure, moisture retention, and texture in gluten-free breads, cakes, pastries, and mixes.
- Dairy & Dairy Alternatives: Supports suspension, mouthfeel, and formulation stability in dairy-based and plant-based products.
- Processed Foods: Helps maintain consistent texture and prevents ingredient separation during storage and distribution.
- Functional Performance: Delivers strong thickening and stabilizing performance at low usage levels, providing efficient formulation control compared with many conventional thickeners.
4. Competitive Advantages
- Quality Consistency: Designed to deliver dependable viscosity, texture, and stabilization across production batches.
- Supply Reliability: Suitable for structured B2B procurement and recurring industrial requirements.
- Logistics Capability: Standardized 25kg packaging facilitates handling, warehousing, container loading, and international distribution.
- Price Competitiveness: Efficient performance at low dosage levels can support economical formulation and reduce overall ingredient consumption.
- Sustainability: Fermentation-based production provides an efficient route to a versatile functional ingredient with broad formulation applications.
- Technical Documentation: Product specifications and supporting quality documentation can be provided to assist professional buyers with sourcing, quality control, and formulation requirements.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Packaging: 25kg bags
- Loading Capacity: Approximately 20–22 MT per 20ft container, subject to packaging configuration, palletization, and applicable container weight limits
- Supply: Available for bulk B2B and international procurement
Reviews
There are no reviews yet.