
1. Product Overview
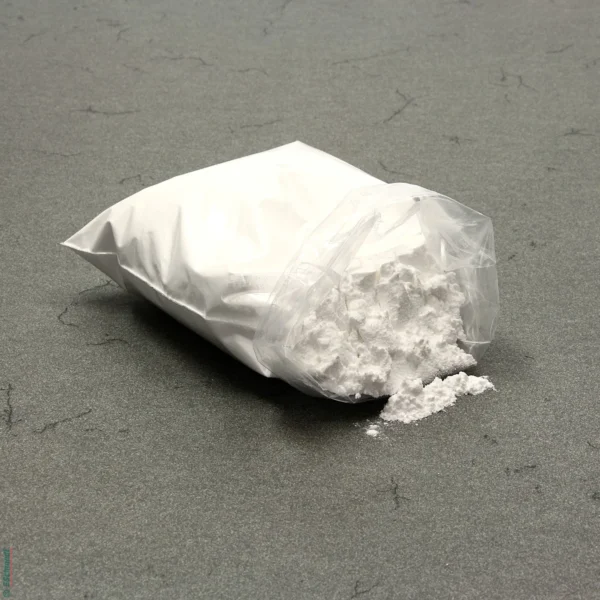
Wheat Starch Food Grade is a refined, high-purity starch derived from wheat and supplied in convenient 25kg bags for commercial food and industrial processing. It is widely used as a thickening, binding, stabilizing, texturizing, and formulation ingredient across food manufacturing and related applications. Its consistent functional performance supports reliable production, improved product texture, and efficient formulation control. As a versatile, high-volume ingredient, wheat starch is strategically important for manufacturers seeking dependable quality and scalable bulk supply.
2. Key Specifications & Technical Characteristics
- Product: Wheat Starch Food Grade
- Raw Material: Wheat-derived starch
- Grade: Food Grade
- Composition: Predominantly wheat starch; may contain naturally occurring trace components associated with wheat
- Purity: High-purity food-grade starch, subject to agreed specification
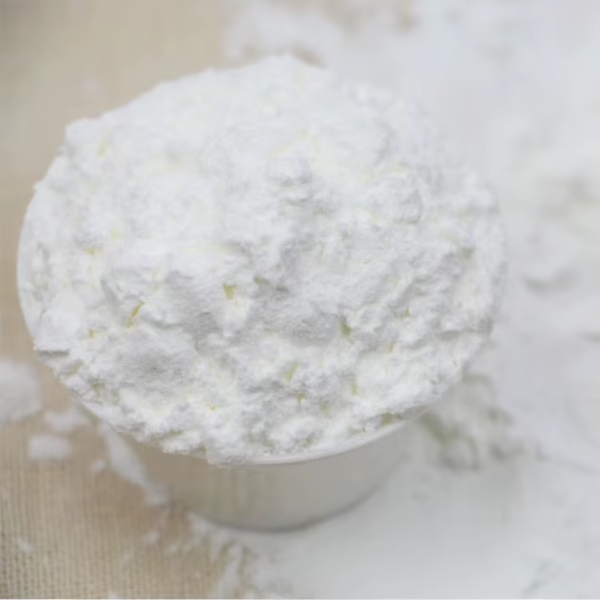
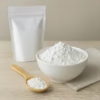
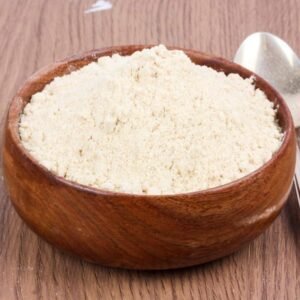
- Physical Form: Fine powder
- Color: White to off-white
- Functional Properties: Thickening, binding, stabilizing, texturizing, and moisture-control performance
- Particle Characteristics: Fine, free-flowing powder suitable for industrial processing
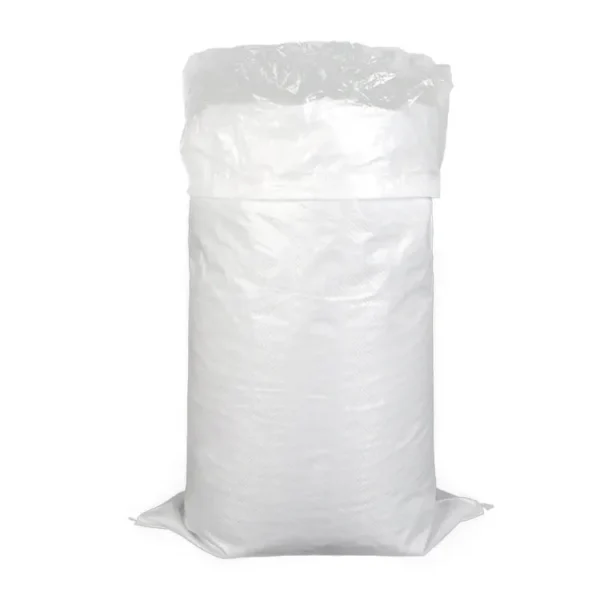
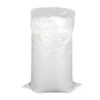
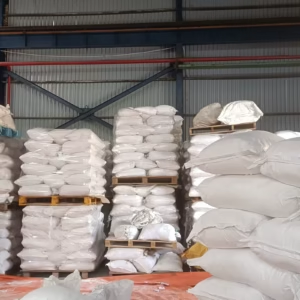
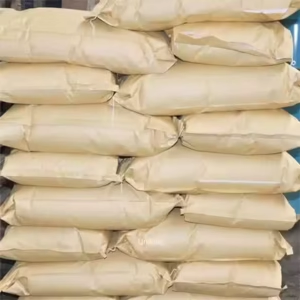
- Packaging: 25kg industrial-grade bags
- Shelf Life: Typically up to 24 months when stored under recommended conditions
- Storage: Keep sealed in a cool, dry, clean environment away from moisture, heat, and contamination
- Documentation: Product specification, Certificate of Analysis (COA), and other relevant documentation available upon request
3. Core Industrial Applications
- Food & Beverage Manufacturing: Used in sauces, soups, bakery products, noodles, confectionery, processed foods, and prepared mixes for texture and consistency control.
- Bakery & Flour Processing: Supports dough structure, texture modification, and formulation optimization in selected bakery applications.
- Confectionery: Used as a functional ingredient for controlling texture, viscosity, and product consistency.
- Processed Foods: Provides binding and thickening functionality in formulated and convenience food products.
- Industrial Food Formulations: Suitable for manufacturers requiring a versatile starch ingredient with predictable processing characteristics.
Its fine powder form, functional versatility, and consistent performance can help manufacturers achieve controlled formulations while supporting efficient large-scale production.
4. Competitive Advantages
- Quality Consistency: Food-grade material designed for reliable batch-to-batch functional performance.
- Supply Reliability: Suitable for recurring commercial procurement and bulk purchasing programs.
- Logistics Capability: Standard 25kg packaging supports efficient handling, storage, palletization, and international shipment.
- Price Competitiveness: Bulk sourcing options support cost-effective procurement for industrial buyers.
- Versatile Performance: Suitable for multiple food-processing applications, reducing the need for separate functional ingredients.
- Sourcing Efficiency: Consolidated commercial supply helps streamline procurement for manufacturers and distributors.
- Technical Documentation: Product specifications and relevant quality documentation can be provided to support buyer evaluation and compliance requirements.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Packaging: 25kg bags
- Loading Capacity: Approximately 20–25 MT per 20ft container, depending on packaging configuration, palletization, and loading requirements
- Supply: Bulk commercial quantities available
- Documentation: COA and product specifications available upon request
Reviews
There are no reviews yet.