
1. Product Overview
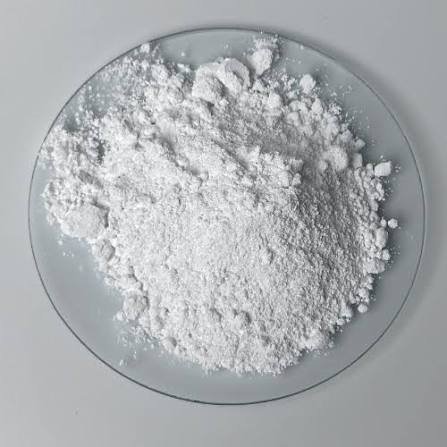
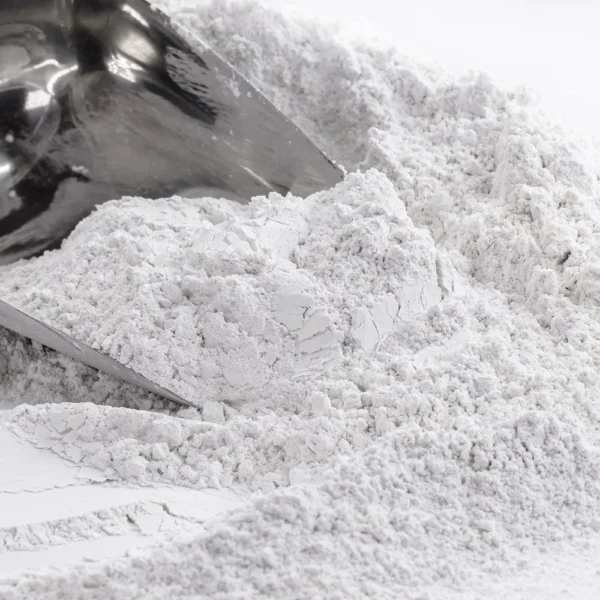
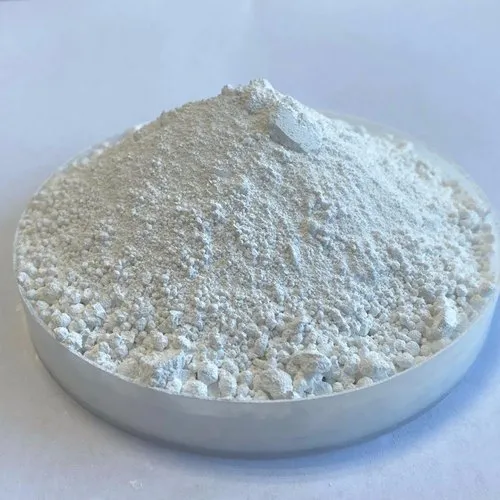
Titanium Dioxide (TiO₂) is a high-performance white pigment valued for its exceptional opacity, brightness, whiteness, and light-scattering capability. It is widely used across coatings, paints, plastics, inks, paper, masterbatch, rubber, and other industrial formulations where superior whiteness, coverage, and durability are required. Its strong performance-to-use ratio enables manufacturers to achieve consistent product quality while optimizing pigment efficiency. As a globally essential industrial pigment, Titanium Dioxide remains a strategic raw material for high-volume manufacturing and formulation applications.
2. Key Specifications & Technical Characteristics
- Chemical Composition: Titanium Dioxide (TiO₂)
- Grade: Industrial / Pigment Grade
- Purity: Typically ≥93–98% TiO₂, depending on grade and specification
- Physical Form: Fine white powder
- Color: Bright white
- Particle Characteristics: Fine, controlled particle size for high opacity and dispersion
- Key Properties: High refractive index, excellent whiteness, strong hiding power, UV resistance, and chemical stability
- Packaging: 25 kg bags; customized bulk packaging available subject to supply requirements
- Shelf Life: Typically 24 months when stored in dry, sealed conditions
- Origin: Available from qualified international sources, subject to specification and availability
3. Core Industrial Applications
- Paints & Coatings: Provides whiteness, opacity, coverage, durability, and UV resistance in architectural and industrial coatings.
- Plastics & Masterbatch: Enhances whiteness, brightness, opacity, and weather resistance in plastic products and compounds.
- Printing Inks: Supports strong color brightness, coverage, and consistent print quality.
- Paper Manufacturing: Improves paper brightness, opacity, and surface appearance.
- Rubber & Elastomers: Used as a white pigment and functional additive in selected rubber formulations.
- Construction Materials: Applied in coatings, decorative products, and cement-based formulations requiring high whiteness and durability.
Its high refractive index and efficient light-scattering performance provide superior opacity and coverage compared with many lower-performance white pigments, helping manufacturers achieve consistent visual quality with optimized formulation efficiency.
4. Competitive Advantages
- Quality Consistency: Controlled pigment characteristics support reliable formulation and batch-to-batch performance.
- High Performance: Excellent whiteness, opacity, brightness, and UV resistance for demanding industrial applications.
- Supply Reliability: Suitable for bulk procurement and recurring industrial supply programs.
- Logistics Capability: International bulk shipment solutions available for commercial buyers.
- Price Competitiveness: Structured for cost-effective sourcing at industrial and container-scale volumes.
- Sustainability: Efficient pigment performance can support optimized formulation and material utilization.
- Technical Documentation: Product specifications, technical data, and relevant quality documentation can be provided according to buyer requirements.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Typically 20–25 MT per 20-foot container, subject to packaging configuration, product density, and applicable shipping limitations


Reviews
There are no reviews yet.