
- Product Overview
Sodium Isobutyl Xanthate (SIBX) 85% Min is a high-performance flotation collector widely used in mineral processing to selectively recover valuable sulfide minerals from ore. It is primarily applied in the flotation of copper, lead, zinc, nickel, and other sulfide-bearing ores, where strong mineral collection and effective separation are essential. With a minimum active content of 85%, SIBX offers reliable flotation performance, consistent recovery, and efficient reagent consumption. Its established performance makes it a strategically important reagent for modern mining operations seeking dependable mineral recovery and competitive processing costs.
- Key Specifications & Technical Characteristics
- Product: Sodium Isobutyl Xanthate (SIBX)
- Chemical type: Xanthate-based sulfide mineral flotation collector
- Purity: 85% Min
- Primary function: Collector for froth flotation of sulfide minerals
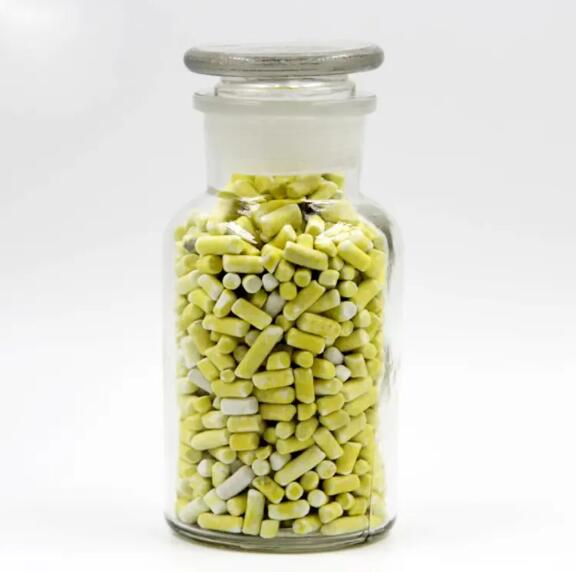
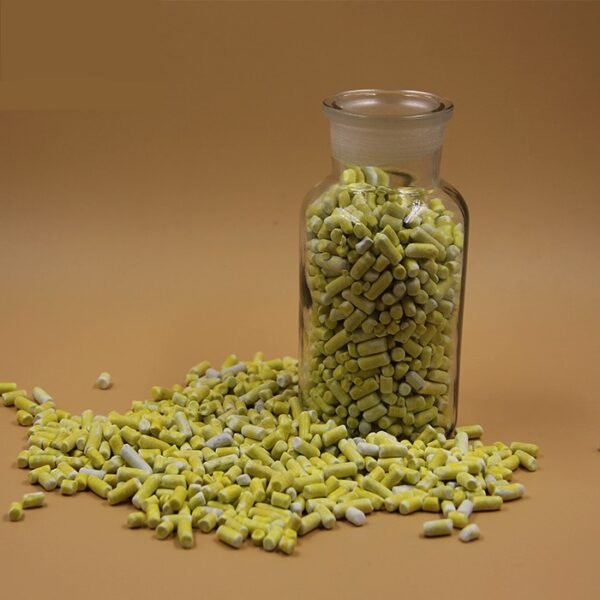
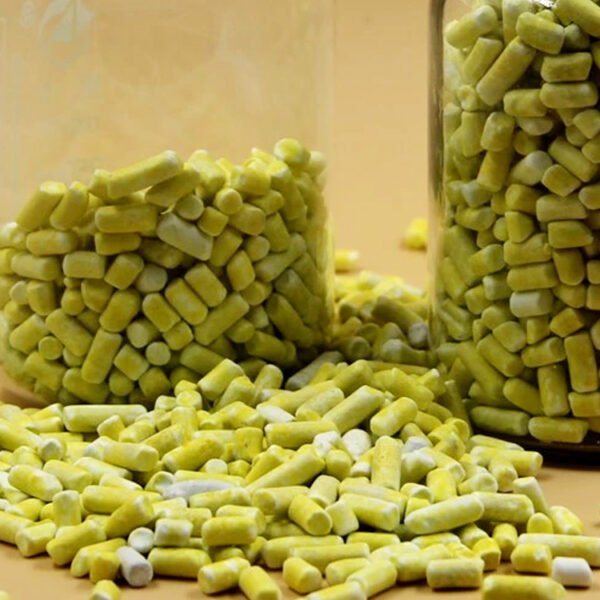
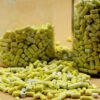
- Physical form: Granular or pelletized solid
- Typical color: Pale yellow to yellow
- Solubility: Soluble in water and suitable for preparation of flotation reagent solutions
- Grade: Mining and mineral-processing grade
- Packaging options: Commonly supplied in moisture-resistant bags, drums, or customized industrial packaging
- Shelf life: Typically up to 12 months when stored sealed in a cool, dry, well-ventilated location away from heat, moisture, and incompatible materials
- Core Industrial Applications
- Copper flotation: Supports the recovery of copper sulfide minerals from complex ores.
- Lead and zinc processing: Used as a collector in selective flotation circuits for sulfide concentrates.
- Nickel sulfide recovery: Supports flotation-based concentration of nickel-bearing sulfide minerals.
- Polymetallic ore processing: Applicable to flotation circuits requiring effective collection of multiple sulfide minerals.
- Mineral beneficiation: Helps improve valuable-mineral recovery and concentrate production efficiency.
SIBX provides strong collecting characteristics and effective mineral surface interaction, making it suitable for demanding flotation circuits where recovery, selectivity, and reagent efficiency are commercially important.
- Competitive Advantages
- Quality consistency: 85% Min specification supports dependable flotation performance across production batches.
- Reliable supply: Suitable for planned bulk procurement and continuous industrial mining operations.
- Processing efficiency: Strong collecting performance can support efficient recovery of targeted sulfide minerals.
- Commercial competitiveness: Bulk supply enables cost-effective procurement for large-scale mineral-processing operations.
- Logistics capability: Available for international industrial supply with packaging and shipment arrangements suited to bulk buyers.
- Technical documentation: Product specifications and relevant quality documentation can be provided for industrial procurement and quality-control requirements.
- Responsible handling: Proper storage, dosing, and process management can help optimize reagent consumption and minimize unnecessary chemical usage.
- Strategic sourcing value: Combines established flotation performance, bulk availability, and commercial scalability for mining companies and mineral-processing facilities.
- Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20 MT
- Loading Capacity: Approximately 20–25 MT per 20-foot container, subject to packaging configuration, container payload limits, and shipping requirements



Reviews
There are no reviews yet.