
1. Product Overview
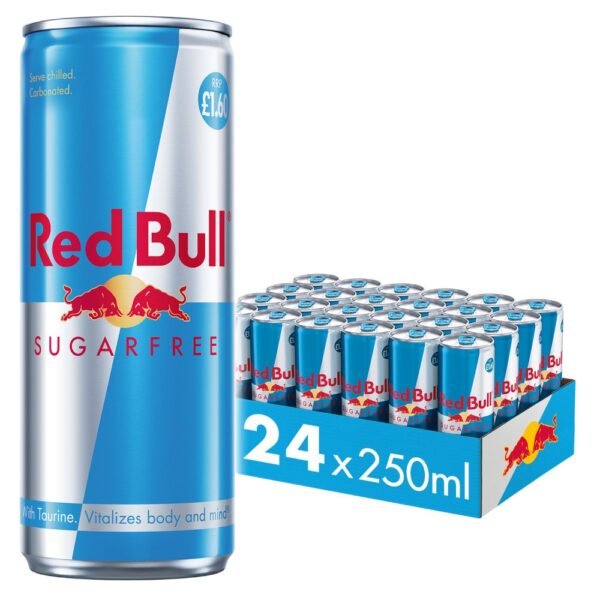
Red Bull Sugarfree – 250 ml is a sugar-free energy drink formulated with caffeine, taurine, B-group vitamins, and other functional ingredients to support alertness and energy. It is widely suited for wholesale distribution across retail, convenience, hospitality, vending, and foodservice channels. The 250 ml can format provides convenient single-serve consumption with established consumer recognition and strong international market demand. Its sugar-free positioning supports growing demand for energy beverages with reduced sugar content.
2. Key Specifications & Technical Characteristics
- Product Type: Sugar-free energy drink
- Key Components: Caffeine, taurine, B-group vitamins, carbonated water, sweeteners, acids, and flavouring ingredients
- Sugar Content: Sugar-free formulation
- Caffeine: Approximately 80 mg per 250 ml can
- Form: Carbonated ready-to-drink liquid
- Appearance: Clear, lightly coloured carbonated beverage
- Pack Size: 250 ml aluminium can
- Packaging Options: Individual cans, multipacks, cartons, and palletized bulk shipments
- Shelf Life: Typically approximately 12 months, subject to the manufacturer’s batch specification
- Storage: Store in a cool, dry environment away from direct sunlight and excessive heat
- Origin: Varies according to production batch and destination market
3. Core Industrial Applications
- Retail & Wholesale Distribution: Suitable for supermarkets, convenience stores, beverage wholesalers, and cash-and-carry operations.
- Foodservice & Hospitality: Used across restaurants, cafés, hotels, bars, entertainment venues, and catering channels.
- Vending & Convenience: Compact 250 ml packaging supports vending machines, forecourts, offices, and high-traffic locations.
- Corporate & Commercial Supply: Suitable for offices, events, hospitality programs, and institutional beverage procurement.
- Commercial Advantage: The sugar-free formulation, recognized product positioning, convenient single-serve format, and established consumer demand support efficient distribution and broad market coverage.
4. Competitive Advantages
- Quality Consistency: Manufactured to established beverage quality and formulation standards.
- Supply Reliability: Suitable for structured wholesale procurement and recurring international supply programs.
- Logistics Capability: Compact 250 ml cans enable efficient palletized handling and containerized transportation.
- Market Positioning: Strong brand recognition and sugar-free formulation support broad retail and commercial distribution.
- Sustainability: Aluminium can packaging offers established recycling potential within appropriate waste-management systems.
- Documentation: Commercial buyers can request applicable product specifications, batch information, packaging details, and export documentation subject to supply source.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Approximately 20–24 MT per 20-ft container, subject to packaging configuration, palletization, and applicable container weight limits


Reviews
There are no reviews yet.