
- Product Overview
Polysorbate 20 is a non-ionic surfactant and emulsifying agent widely used to stabilize, solubilize, and disperse ingredients across food, pharmaceutical, cosmetic, and industrial formulations. It is particularly valued for improving the uniformity, stability, and performance of formulations containing oils, flavors, fragrances, and other difficult-to-mix components. Its versatile functionality and compatibility with aqueous systems make it an important ingredient for manufacturers seeking consistent formulation performance and efficient processing. As a globally traded specialty ingredient, Polysorbate 20 supports reliable large-scale production across multiple industries. - Key Specifications & Technical Characteristics
- Chemical composition: Polyoxyethylene (20) sorbitan monolaurate
- CAS Number: 9005-64-5
- Grade: Industrial, food, cosmetic, or pharmaceutical grade subject to specification
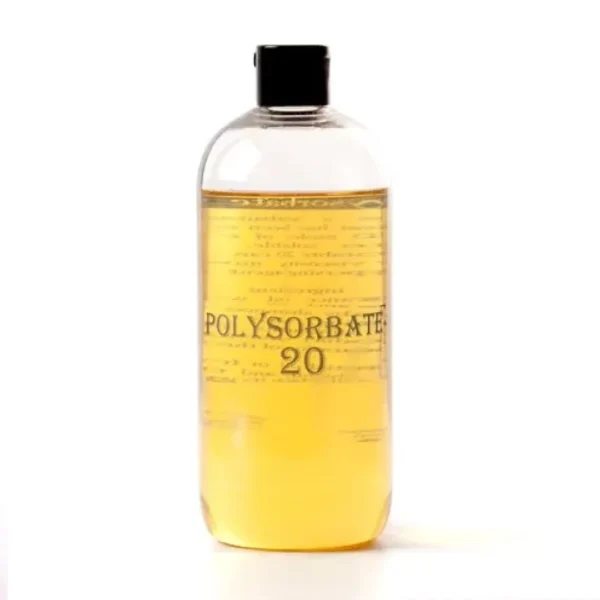
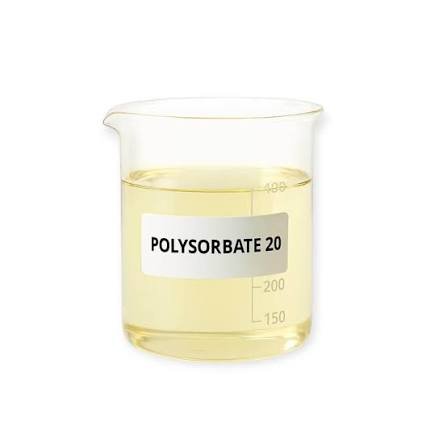
- Form: Clear to slightly yellow, viscous liquid or semi-liquid
- Solubility: Readily dispersible/soluble in water and compatible with many polar and non-polar formulation systems
- Function: Emulsifier, solubilizer, dispersing agent, stabilizer, and wetting agent
- Purity: Available according to applicable grade and buyer specification
- Packaging options: 25 kg drums, 200 kg drums, IBC tanks, and bulk supply subject to order requirements
- Shelf life: Typically 24 months when stored in original sealed packaging under recommended conditions
- Storage: Store in a cool, dry, well-ventilated location away from excessive heat and direct sunlight
- Origin: Available from qualified international manufacturing and supply sources
- Core Industrial Applications
- Food & Beverage: Used as an emulsifier and stabilizer in beverages, flavor systems, confectionery, sauces, and formulated foods.
- Pharmaceuticals: Supports solubilization, dispersion, and stabilization of active and inactive ingredients in pharmaceutical formulations.
- Cosmetics & Personal Care: Used in creams, lotions, shampoos, cleansers, fragrances, and other formulations requiring effective emulsification and ingredient dispersion.
- Chemical & Industrial Formulations: Functions as a wetting, dispersing, and stabilizing agent in specialized formulation processes.
- Performance advantage: Its non-ionic nature, broad formulation compatibility, and effective emulsification properties help manufacturers achieve consistent product quality while improving processing efficiency and formulation stability.
- Competitive Advantages
- Consistent Quality: Supplied to defined technical specifications for dependable batch-to-batch performance.
- Supply Reliability: Suitable for recurring industrial procurement and large-volume sourcing programs.
- Logistics Capability: Available in drum, IBC, and bulk formats to support different production and transportation requirements.
- Price Competitiveness: Bulk sourcing options help optimize total procurement costs for commercial manufacturers.
- Formulation Efficiency: Provides multifunctional emulsifying, solubilizing, stabilizing, and dispersing performance in a single ingredient.
- Technical Documentation: Product specifications, certificates, and quality documentation can be provided subject to grade and supply arrangement.
- Strategic Sourcing Value: A versatile, high-demand specialty ingredient suitable for manufacturers seeking dependable international supply and scalable procurement.
- Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20 MT
- Loading Capacity: Approximately 20–22 MT per 20-foot container, subject to packaging configuration, product density, container regulations, and final loading plan.


Reviews
There are no reviews yet.