
1. Product Overview
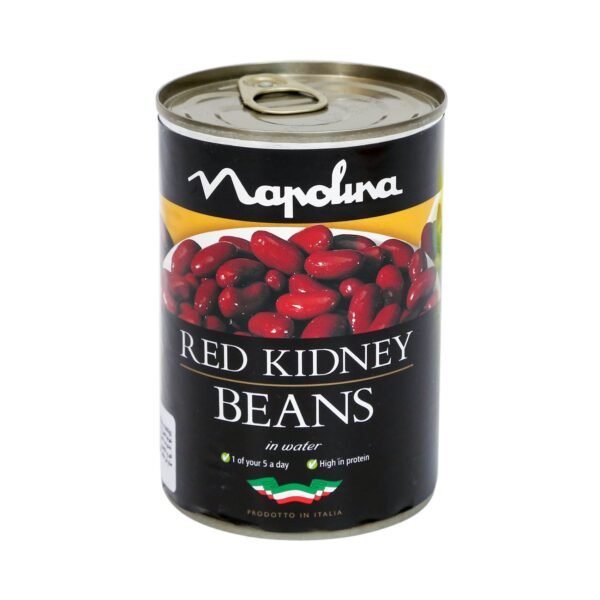
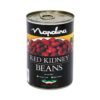
Napolina Red Kidney Beans — 400g are prepared red kidney beans selected for consistent quality, convenient use, and dependable culinary performance. They are primarily used in food manufacturing, catering, hospitality, retail foodservice, and prepared-meal applications, providing a ready-to-use source of plant-based protein and dietary fibre. Their convenient canned format reduces preparation time, labour requirements, and handling compared with dried alternatives. For commercial buyers, they offer a practical solution for standardized recipes, portion control, and efficient food production.
2. Key Specifications & Technical Characteristics
- Product: Red Kidney Beans
- Food Grade: Human consumption / foodservice grade
- Main Ingredient: Red kidney beans
- Form: Whole cooked beans
- Colour: Characteristic deep red to reddish-brown
- Texture: Cooked, tender, and suitable for direct culinary use
- Packaging: 400g retail can
- Net Weight: 400g
- Preparation: Ready to use after opening; suitable for incorporation into recipes
- Shelf Life: Typically extended under unopened, properly stored conditions; refer to manufacturer’s date marking
- Storage: Store unopened in a cool, dry place; refrigerate after opening and consume according to manufacturer guidance
- Origin: As specified on the manufacturer’s packaging and batch documentation
3. Core Industrial Applications
- Food Manufacturing: Suitable for canned meals, ready meals, sauces, soups, stews, and mixed-bean products.
- Restaurants & Catering: Provides a convenient ingredient for chilli, salads, rice dishes, Mexican-style meals, and other prepared recipes.
- Hospitality & Foodservice: Supports consistent portioning and rapid meal preparation without the extended soaking and cooking process required for dried beans.
- Retail & Wholesale Distribution: Convenient 400g format suitable for grocery, foodservice, and commercial distribution channels.
- Prepared Foods: Adds plant-based protein, fibre, texture, colour, and nutritional value to formulated food products.
The ready-to-use format improves operational efficiency by reducing preparation time, cooking requirements, and ingredient handling while supporting consistent recipe outcomes.
4. Competitive Advantages
- Quality Consistency: Standardized canned format supports dependable taste, appearance, texture, and portion control.
- Operational Efficiency: Ready-to-use beans reduce preparation and cooking time compared with conventional dried beans.
- Supply Reliability: Established branded food product suitable for structured wholesale and commercial sourcing programs.
- Logistics Capability: Compact, shelf-stable canned packaging supports efficient storage, handling, palletization, and distribution.
- Commercial Value: Helps food operators control preparation costs and labour requirements while maintaining recipe consistency.
- Versatile Application: Suitable across food manufacturing, catering, hospitality, retail, and institutional foodservice.
- Documentation: Product and packaging information can support commercial purchasing, traceability, and food-safety requirements.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Subject to container type, pallet configuration, packaging arrangement, and applicable shipment requirements
- Supply Format: Commercial bulk supply available subject to order confirmation and availability
Reviews
There are no reviews yet.