
1. Product Overview
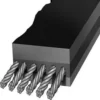
Mining Conveyor Belt – Steel Cord Heavy-Duty Ore Handling Grade is an industrial-grade conveyor belt engineered for continuous transport of heavy, abrasive bulk materials in demanding mining and mineral-processing environments. Its steel-cord reinforcement provides high tensile strength, dimensional stability, long-distance conveying capability, and resistance to severe mechanical loading. Designed for reliable handling of ore, rock, coal, aggregates, and other bulk materials, it supports high-throughput operations while reducing downtime and maintenance requirements. Its combination of strength, durability, and dependable performance makes it a strategically important solution for modern mining and bulk-material logistics.
2. Key Specifications & Technical Characteristics
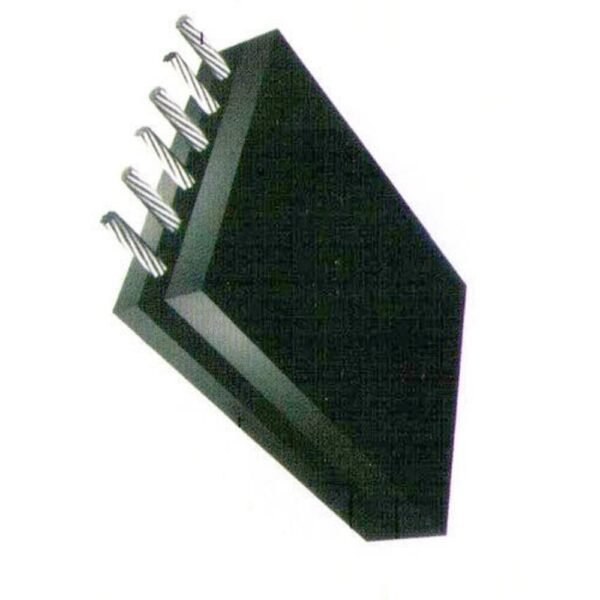
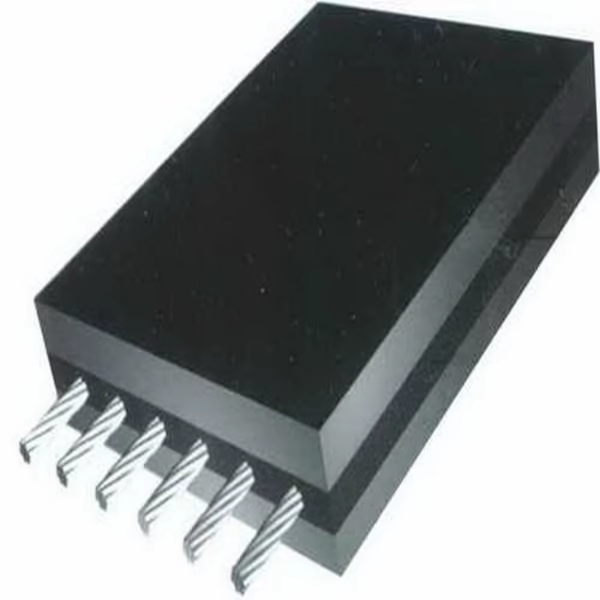
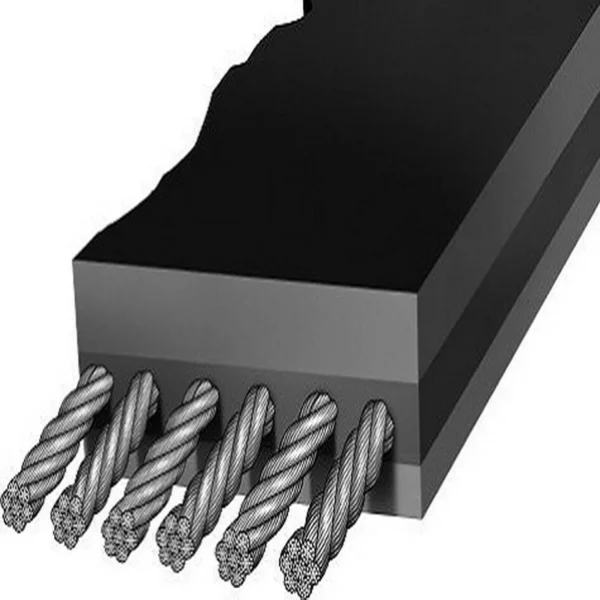
- Reinforcement: High-strength longitudinal steel cords embedded within a rubber conveyor-belt structure.
- Cover Material: Heavy-duty abrasion-resistant rubber compound engineered for demanding bulk-material handling.
- Grade: Heavy-duty mining and ore-handling grade.
- Material Characteristics: Steel cord reinforcement with wear-resistant rubber top and bottom covers.
- Tensile Strength: Available in multiple high-tensile-strength ratings according to conveyor system requirements.
- Belt Width: Available in various widths for different conveyor capacities and system configurations.
- Belt Thickness: Available in multiple thicknesses depending on load, application, and operating conditions.
- Color: Typically black industrial rubber.
- Operating Performance: Designed for continuous conveying of heavy, abrasive and high-volume materials.
- Abrasion Resistance: High resistance to wear caused by ore, rock, aggregate and other abrasive materials.
- Impact Resistance: Engineered to withstand heavy loading and material impact at transfer points.
- Packaging: Supplied rolled and securely packaged for industrial transportation and storage.
- Customization: Belt width, length, tensile rating, cover thickness and other specifications can be supplied according to project requirements.
- Shelf Life: Store in a cool, dry location away from direct sunlight, heat, ozone-generating equipment and chemicals; storage life depends on applicable manufacturer specifications and conditions.
3. Core Industrial Applications
- Mining: Continuous transportation of iron ore, copper ore, gold ore, coal, limestone and other mined materials.
- Mineral Processing: Feeding and transferring crushed ore between crushers, screens, stockpiles and processing units.
- Quarrying: Handling stone, aggregates, gravel, sand and other high-abrasion materials.
- Bulk Material Terminals: High-volume transportation of minerals and bulk commodities over long conveying distances.
- Steel & Cement Industries: Moving raw minerals, limestone, clinker-related materials and other heavy bulk inputs.
- Power & Industrial Plants: Conveying coal and other bulk materials in large-scale material-handling systems.
Steel-cord construction delivers superior tensile strength and dimensional stability compared with conventional fabric-reinforced belts, making it particularly suitable for long-distance, high-load conveyor systems. The robust rubber covers provide resistance against abrasion and impact, helping extend service intervals and reduce belt replacement frequency. High load-carrying capability also enables efficient continuous material movement, supporting greater operational throughput and lower material-handling costs.
4. Competitive Advantages
- Quality Consistency: Engineered with controlled steel-cord reinforcement and durable rubber compounds for dependable performance across demanding applications.
- High Durability: Strong resistance to abrasion, impact and heavy mechanical loading helps extend operating life.
- Supply Reliability: Suitable for scheduled bulk procurement and ongoing mining-project requirements, subject to specification and production availability.
- Logistics Capability: Supplied in industrial rolls and prepared for efficient international shipment and project-based deliveries.
- Price Competitiveness: High service life and reduced replacement frequency can contribute to lower total cost of ownership.
- Operational Efficiency: High tensile strength and load-carrying capability support continuous, high-volume material transportation.
- Sustainability Benefits: Longer service intervals can reduce material consumption, replacement frequency, maintenance activity and associated operational waste.
- Technical Support: Product specifications, technical documentation and application guidance can be provided according to project and conveyor-system requirements.
- Strategic Sourcing Value: Combines heavy-duty performance, scalable supply, customizable specifications and international logistics suitability for mining and industrial procurement programs.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Dependent on belt width, thickness, roll dimensions and container configuration; container loading can be optimized according to the confirmed order specification.


Reviews
There are no reviews yet.