


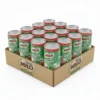

1. Product Overview
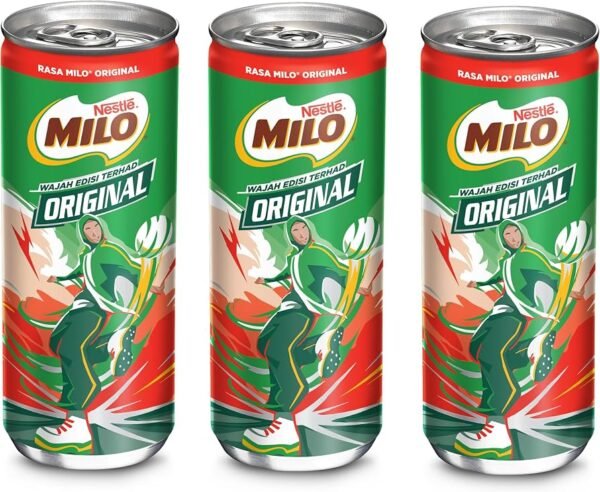
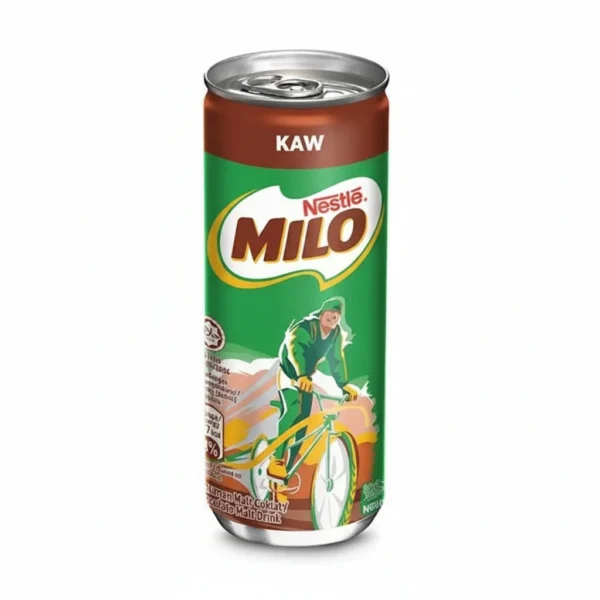
Milo Chocolate Malt – 240 ml is a ready-to-drink chocolate malt beverage formulated to deliver a convenient combination of chocolate flavour, malt nourishment, and refreshment. It is suitable for wholesale distribution across retail, foodservice, convenience, and institutional beverage channels. Its single-serve format supports convenient consumption while enabling efficient merchandising and high-volume distribution. The product offers commercial value for buyers seeking an established chocolate malt beverage category with broad consumer appeal.
2. Key Specifications & Technical Characteristics
- Product Type: Ready-to-drink chocolate malt beverage
- Flavour: Chocolate malt
- Form: Liquid, ready for consumption
- Pack Size: 240 ml
- Colour: Chocolate brown
- Key Components: Milk and/or milk-derived ingredients, malt extract, cocoa/chocolate ingredients, sweeteners, vitamins and minerals; exact formulation varies by market
- Grade: Commercial food & beverage grade
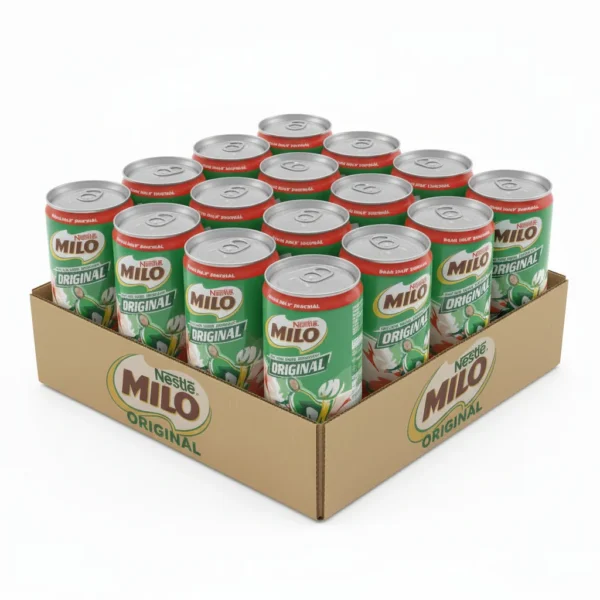
- Packaging: 240 ml individual retail units; outer cartons/cases available according to supplier configuration
- Shelf Life: Subject to manufacturer batch specification and storage conditions
- Storage: Store according to the manufacturer’s labelled requirements
- Origin: Market-dependent; confirm country of origin and batch documentation with supplier
3. Core Industrial Applications
- Retail & Wholesale Distribution: Suitable for supermarkets, wholesalers, convenience stores, and general retail networks.
- Foodservice & Hospitality: Practical for cafés, restaurants, hotels, catering operations, and institutional beverage supply.
- Convenience Beverage Channels: The 240 ml format supports grab-and-go merchandising and portion-controlled consumption.
- Institutional Supply: Suitable for schools, workplaces, hospitality groups, and other high-volume beverage procurement programs.
- Commercial Advantage: Ready-to-drink convenience reduces preparation requirements compared with powdered malt beverages, supporting efficient handling, merchandising, and service.
4. Competitive Advantages
- Quality Consistency: Standardized branded formulation supports consistent flavour and product presentation across supplied batches.
- Supply Reliability: Suitable for structured wholesale procurement and repeat commercial orders, subject to availability and destination requirements.
- Logistics Capability: Compact single-serve packaging facilitates case handling, warehousing, distribution, and retail replenishment.
- Price Competitiveness: Bulk procurement can support commercially efficient sourcing for distributors and high-volume buyers.
- Market Appeal: Chocolate malt combines familiar flavour characteristics with convenient ready-to-drink consumption.
- Documentation: Product specifications, batch information, and applicable commercial documentation can be provided subject to supplier availability.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Dependent on packaging configuration, carton dimensions, palletization, and container type; confirm final loading plan with supplier


Reviews
There are no reviews yet.