
1. Product Overview
Methylparaben is a high-purity ester of p-hydroxybenzoic acid widely used as an effective antimicrobial preservative in pharmaceutical, cosmetic, personal care, and selected industrial formulations. It helps inhibit the growth of bacteria, yeast, and molds, supporting product stability and extending usable shelf life. Its reliable preservative performance, formulation versatility, and cost efficiency make it an important ingredient for manufacturers requiring consistent protection against microbial deterioration. Available for bulk B2B sourcing, Methylparaben supports scalable production and international procurement requirements.
2. Key Specifications & Technical Characteristics
- Chemical Name: Methylparaben
- Chemical Formula: C₈H₈O₃
- CAS Number: 99-76-3
- Purity: Typically ≥99%
- Grade: Pharmaceutical, cosmetic, personal care, or industrial grade subject to specification
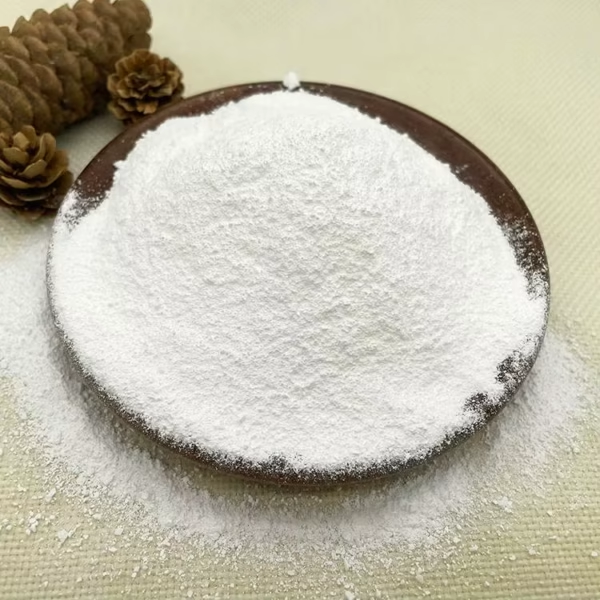
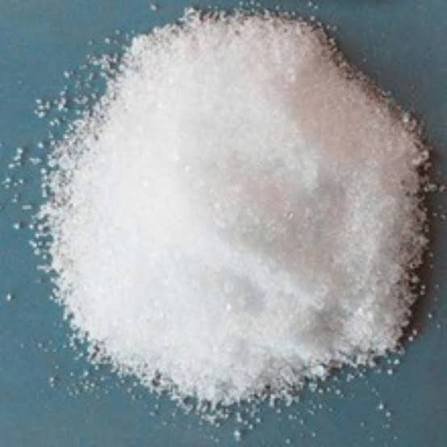
- Physical Form: White to almost white crystalline powder or crystals
- Odor: Practically odorless
- Solubility: Slightly soluble in water; soluble in alcohol and other suitable organic solvents
- Packaging Options: Standard industrial bags or customized bulk packaging
- Shelf Life: Typically 24–36 months when stored under recommended conditions
- Storage: Keep tightly sealed in a cool, dry, well-ventilated area away from excessive heat and moisture
- Origin: Available from qualified international manufacturing and supply sources
- Documentation: Certificate of Analysis (CoA), Safety Data Sheet (SDS), and applicable technical documentation available subject to order requirements
3. Core Industrial Applications
- Pharmaceuticals: Used as an antimicrobial preservative in selected pharmaceutical formulations, topical preparations, and other products requiring microbial protection.
- Cosmetics & Personal Care: Applied in creams, lotions, shampoos, conditioners, gels, and other water-containing formulations to help control microbial growth.
- Food & Specialty Formulations: Used in permitted applications where regulatory requirements specifically allow its use as a preservative.
- Industrial Formulations: Suitable for selected chemical and formulation processes where reliable antimicrobial preservation is required.
- Performance Advantage: Provides consistent preservative activity at relatively low use levels, helping manufacturers maintain formulation stability, reduce spoilage risk, and improve product shelf-life economics.
4. Competitive Advantages
- Quality Consistency: High-purity material with controlled physical and chemical characteristics for dependable formulation performance.
- Supply Reliability: Suitable for recurring industrial procurement and large-volume purchasing programs.
- Logistics Capability: Bulk export supply with packaging and shipment configurations adaptable to international B2B requirements.
- Price Competitiveness: Efficient bulk sourcing supports competitive landed-cost management for manufacturers and distributors.
- Technical Documentation: CoA, SDS, specifications, and relevant quality documentation can be provided according to customer and regulatory requirements.
- Strategic Sourcing Value: Combines dependable preservative performance, scalable availability, and bulk procurement efficiency for long-term industrial supply.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20 MT
- Loading Capacity: Up to approximately 20 MT per 20-foot container, subject to packaging configuration, product density, and applicable shipping limitations
- Supply Format: Bulk B2B international supply
- Packaging: Standard industrial packaging or customized packaging available upon request



Reviews
There are no reviews yet.