

1. Product Overview
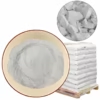
Hydrated Lime 90% Ca(OH)₂ Min is a high-purity calcium hydroxide material engineered for demanding mining and mineral processing applications. It is primarily used for pH control, mineral processing, flotation support, water treatment, and chemical neutralization operations. Its consistent chemical performance enables efficient process control, improved recovery conditions, and dependable treatment performance. As a strategic industrial reagent, it supports mining operations seeking reliable quality, predictable processing results, and cost-efficient bulk supply.
2. Key Specifications & Technical Characteristics
- Product: Hydrated Lime
- Chemical Composition: Calcium Hydroxide [Ca(OH)₂]
- Minimum Purity: 90% Ca(OH)₂
- Grade: Mining & Mineral Processing Grade
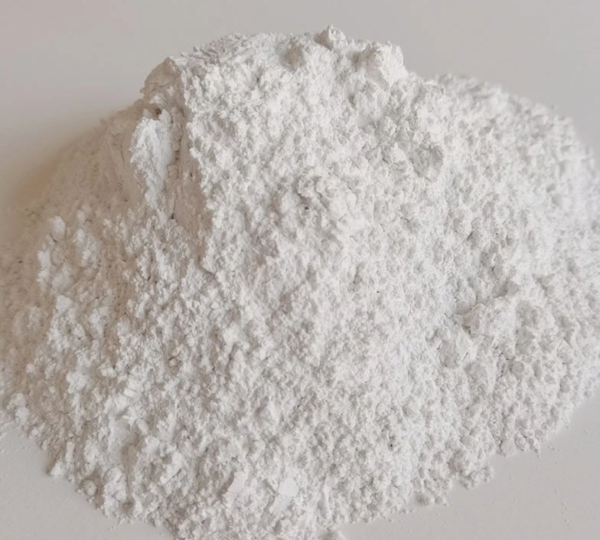
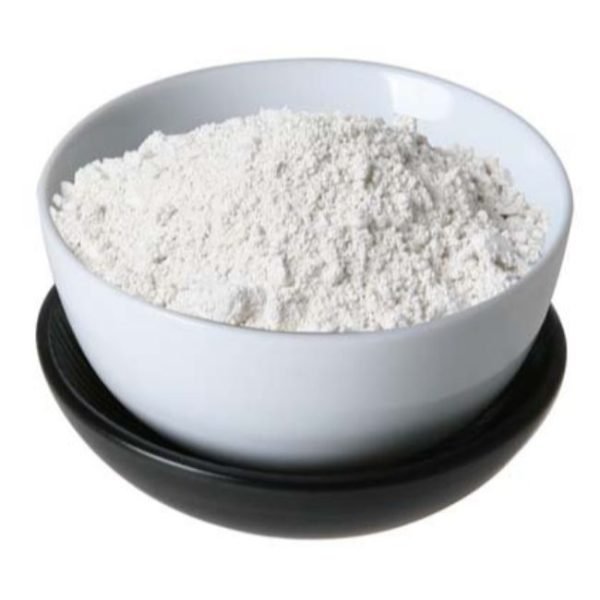
- Physical Form: Fine powder
- Colour: Typically white to off-white
- Particle Size: Fine, controlled powder suitable for industrial processing
- Solubility: Low water solubility with effective alkalinity for process applications
- Packaging Options: 25 kg bags, 500 kg–1,000 kg jumbo bags, or bulk loading
- Shelf Life: Typically up to 12 months when stored sealed in a dry, well-ventilated environment
- Storage: Protect from moisture, contamination, and prolonged exposure to atmospheric carbon dioxide
3. Core Industrial Applications
- Gold Mining & Mineral Processing: Used for pH adjustment and alkalinity control in mineral recovery and processing circuits.
- Flotation Operations: Supports controlled pH conditions to optimize mineral separation and recovery.
- Water & Wastewater Treatment: Neutralizes acidic water and helps control treatment-process alkalinity.
- Acid Mine Drainage Treatment: Provides effective neutralization of acidic streams and process water.
- Metallurgical Processing: Used in various chemical treatment and mineral-processing operations requiring controlled alkalinity.
- Chemical Neutralization: Suitable for industrial processes requiring a dependable alkaline reagent.
Its high Ca(OH)₂ content provides effective neutralization and process control while offering practical handling and dosing advantages compared with less concentrated lime materials.
4. Competitive Advantages
- Consistent Quality: Minimum 90% Ca(OH)₂ specification supports predictable industrial performance.
- Reliable Bulk Supply: Structured sourcing supports continuous requirements for mining and mineral-processing operations.
- Logistics Capability: Available in industrial packaging and bulk shipment formats to accommodate different supply-chain requirements.
- Price Competitiveness: Bulk procurement supports cost-efficient sourcing for large-scale operations.
- Operational Efficiency: Effective alkalinity enables controlled pH adjustment and efficient neutralization.
- Sustainability: Supports water-treatment and acid-neutralization processes while reducing the need for more complex chemical treatment solutions.
- Technical Documentation: Product specifications and supporting commercial documentation can be provided for qualified industrial buyers.
- Strategic Sourcing: Suitable for mining companies, mineral processors, distributors, and industrial procurement teams seeking dependable international supply.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20 MT
- Loading Capacity: Approximately 20–25 MT per 20-ft container, subject to packaging configuration, loading regulations, and destination requirements.


Reviews
There are no reviews yet.