1. Product Overview
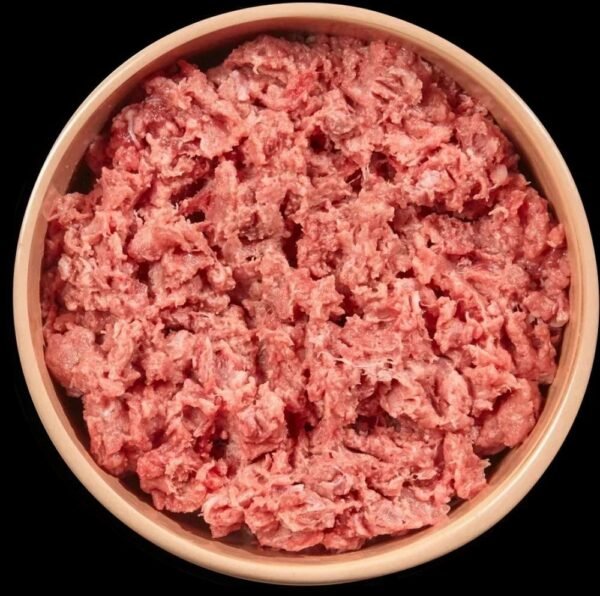
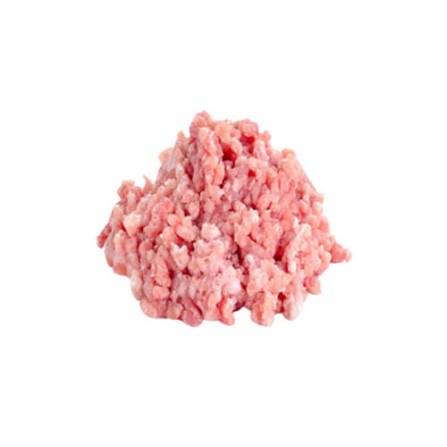
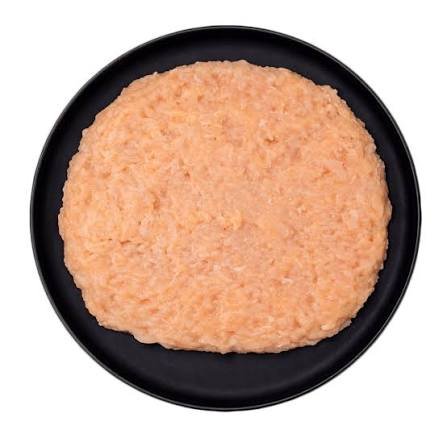
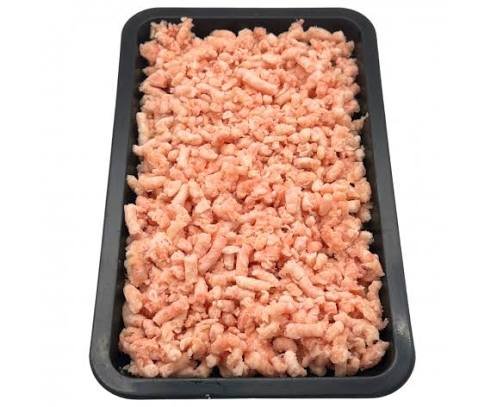
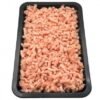
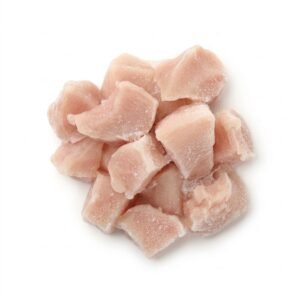
Frozen Chicken Minced Meat is finely minced chicken meat processed and frozen to preserve freshness, flavour, and nutritional value. It is suitable for large-scale food manufacturing, meat processing, catering, and commercial food preparation. Its consistent texture and versatility support efficient production of burgers, sausages, meatballs, dumplings, fillings, and ready-to-cook meals. As a widely used poultry ingredient, it offers food producers and distributors a practical, cost-effective solution for meeting demand across retail and food-service markets.
2. Key Specifications & Technical Characteristics
- Composition: Minced chicken meat; fat content and other specifications depend on the agreed product grade.
- Grade: Food-grade frozen poultry product.
- Physical Form: Finely minced meat.
- Colour: Typically pale pink to light pink when frozen or thawed under appropriate conditions.
- Processing: Hygienically processed and frozen for preservation.
- Packaging Options: Food-grade, sealed bags or bulk cartons; pack sizes subject to supplier specifications.
- Storage Conditions: Store at −18°C or below.
- Shelf Life: Subject to the manufacturer’s specification, packaging, and uninterrupted frozen storage.
- Origin: Country of origin confirmed according to supplier documentation.
- Documentation: Product specification, batch details, and applicable food-safety or export documents subject to availability.
3. Core Industrial Applications
- Meat Processing: Production of chicken burgers, sausages, meatballs, nuggets, and formed poultry products.
- Food Manufacturing: Ingredient for frozen meals, ready-to-cook products, dumplings, pies, and prepared fillings.
- Hospitality & Catering: Suitable for restaurants, hotels, institutional kitchens, and large-scale catering operations.
- Retail & Food Distribution: Supply to supermarkets, frozen-food distributors, wholesalers, and food-service suppliers.
- Commercial Food Preparation: Supports portion-controlled production, streamlined preparation, and efficient ingredient handling.
Its versatility, ease of portioning, and suitability for batch processing help reduce preparation time and support consistent production when managed under appropriate food-safety and quality-control procedures.
4. Competitive Advantages
- Quality Consistency: Defined product specifications and batch controls support dependable manufacturing results.
- Supply Reliability: Bulk procurement options support recurring demand and larger production requirements, subject to availability.
- Logistics Capability: Frozen-chain handling and temperature-controlled transport help maintain product integrity during distribution.
- Price Competitiveness: Bulk purchasing can improve procurement efficiency and cost management.
- Storage Efficiency: Frozen preservation supports inventory planning and extended distribution cycles when stored correctly.
- Food Safety & Documentation: Product specifications, traceability information, and relevant compliance documents can be requested, subject to supplier availability.
- Versatile Applications: Suitable for multiple food-processing and food-service applications, helping simplify ingredient sourcing.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): Bulk — 20 MT.
- Loading Capacity: Dependent on container type, packaging configuration, payload limits, and frozen-transport requirements; confirm the exact metric-ton capacity with the supplier before shipment.
Reviews
There are no reviews yet.