
1. Product Overview
Epoxy Floor Coating 20L is a high-performance protective coating designed to create a durable, seamless, and chemically resistant surface on concrete and other suitable substrates. It is widely used in industrial facilities, warehouses, factories, workshops, commercial buildings, garages, and high-traffic environments where floor protection and easy maintenance are essential. The coating provides strong adhesion, abrasion resistance, and a smooth finish that helps extend floor service life while reducing maintenance requirements. Its combination of durability, protection, and operational efficiency makes it a strategic solution for demanding flooring applications.
2. Key Specifications & Technical Characteristics
- Material Composition: Two-component epoxy resin and curing-agent system
- Grade: Industrial-grade floor coating
- Physical Form: Liquid coating system
- Finish: Smooth, hard-wearing protective finish
- Chemical Resistance: Resistant to a broad range of oils, fuels, chemicals, and industrial contaminants
- Abrasion Resistance: Designed for high-traffic and heavy-use environments
- Adhesion: Strong bonding to properly prepared concrete and compatible substrates
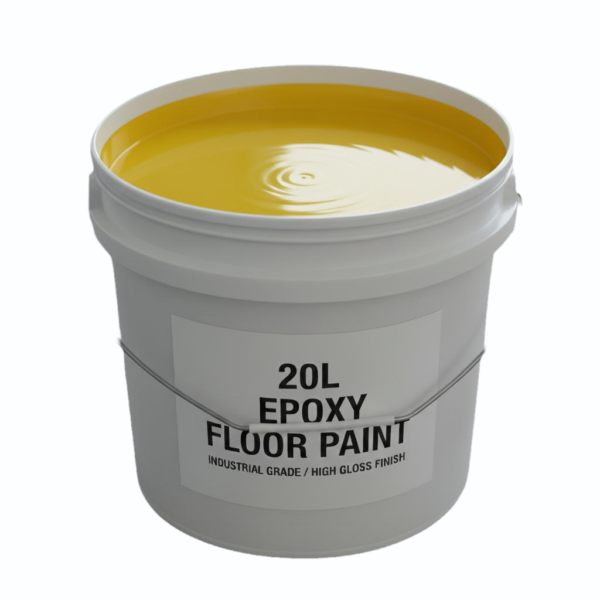
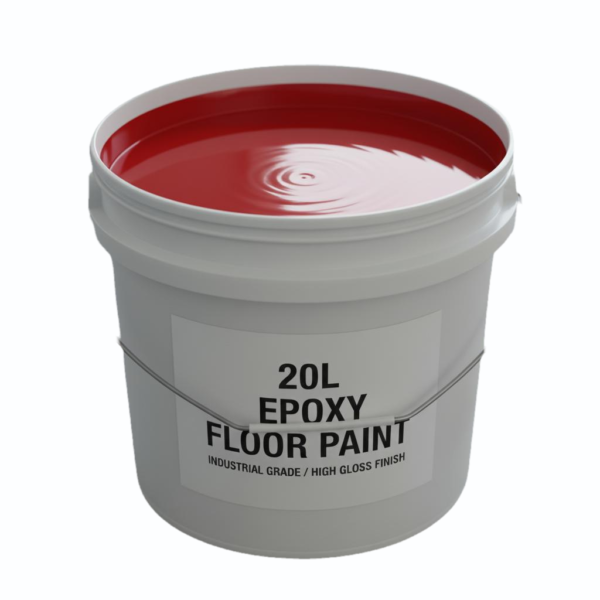
- Packaging: 20L industrial container
- Application: Roller, brush, or suitable industrial coating equipment, subject to product specification
- Colour: Available in various industrial colours, subject to order
- Shelf Life: Typically 12–24 months when stored unopened under recommended conditions
- Storage: Store sealed in a cool, dry, well-ventilated area away from direct sunlight and ignition sources
- Origin: Available for international wholesale supply
3. Core Industrial Applications
- Manufacturing & Industrial Plants: Protects production floors against abrasion, oils, chemicals, and continuous operational traffic.
- Warehouses & Distribution Centres: Provides a durable, easy-to-clean surface suitable for forklifts, pallet trucks, and heavy pedestrian traffic.
- Automotive Workshops & Garages: Creates a resilient surface capable of withstanding oils, lubricants, vehicle fluids, and mechanical activity.
- Commercial & Institutional Facilities: Suitable for workshops, service areas, corridors, utility rooms, and other demanding environments.
- Food & Processing Facilities: Provides a smooth, cleanable flooring surface where compatible with the specific operational and regulatory requirements.
- Commercial Benefits: Compared with conventional floor paints, epoxy systems can provide greater durability, chemical resistance, easier maintenance, and longer service performance when correctly specified and applied.
4. Competitive Advantages
- Quality Consistency: Formulated for reliable application performance and consistent protective coverage.
- Durability: Provides a hard-wearing surface designed for demanding industrial traffic and operating conditions.
- Chemical & Abrasion Protection: Helps protect concrete substrates from common industrial chemicals, oils, impact, and wear.
- Supply Reliability: Suitable for structured wholesale procurement and recurring industrial requirements.
- Logistics Capability: 20L packaging supports efficient handling, storage, and international shipment.
- Price Competitiveness: Bulk procurement can support cost-efficient sourcing for contractors, distributors, and industrial buyers.
- Sustainability Benefits: Extends floor service life and can reduce the frequency of repairs, recoating, and substrate replacement.
- Technical Support: Product specifications, application guidance, safety documentation, and technical information can be provided subject to supply requirements.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Subject to packaging configuration, container dimensions, and applicable shipping regulations
- Supply Format: Wholesale and bulk industrial supply
- International Availability: Available for export and global B2B procurement

Reviews
There are no reviews yet.