
1. Product Overview
Dipotassium Phosphate (DKP), commonly supplied as dipotassium hydrogen phosphate (K₂HPO₄), is a high-value inorganic salt widely used as a buffering agent, nutrient source, stabilizer, and processing aid across food, pharmaceutical, agricultural, and industrial applications. Its excellent solubility, reliable potassium and phosphate contribution, and effective pH-buffering performance make it a versatile ingredient for demanding formulations. The product supports consistent processing performance while helping manufacturers optimize formulation stability and operational efficiency. As a strategically important phosphate ingredient, Dipotassium Phosphate offers industrial buyers a dependable solution for high-volume, quality-sensitive applications.
2. Key Specifications & Technical Characteristics
- Chemical composition: Dipotassium hydrogen phosphate (K₂HPO₄)
- Chemical form: Inorganic potassium phosphate salt
- Typical purity: Industrial/commercial grades available according to application requirements
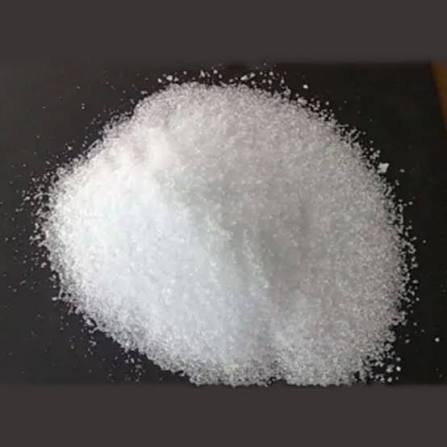
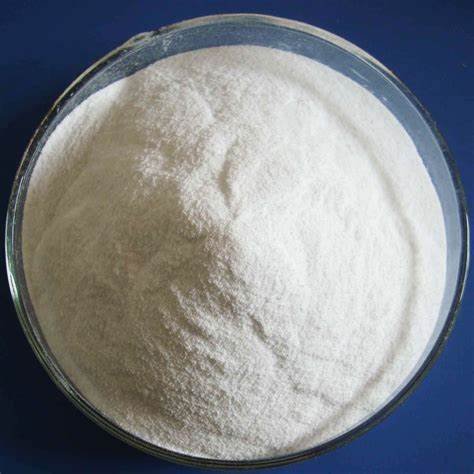
- Physical form: White crystalline powder or granules
- Solubility: Highly soluble in water
- Functional characteristics: Effective buffering capacity, potassium and phosphate source, stabilizing and processing properties
- Grade options: Food grade, pharmaceutical grade, agricultural grade, and industrial grade subject to specification
- Packaging options: 25 kg bags and bulk packaging available according to order requirements
- Shelf life: Typically up to 24 months when stored in original, sealed packaging under recommended dry conditions
- Storage: Store in a cool, dry, well-ventilated area and protect from moisture and contamination
- Origin: Available from established international supply sources, subject to customer specification and availability
3. Core Industrial Applications
- Food & Beverage: Used as a buffering agent, stabilizer, emulsification aid, and mineral source in processed foods, beverages, dairy formulations, and nutritional products.
- Pharmaceutical Manufacturing: Applied as a buffering and formulation component where controlled pH and consistent chemical performance are required.
- Agriculture & Fertilizer Production: Provides readily available potassium and phosphate nutrients for specialized fertilizer and plant-nutrition formulations.
- Biotechnology & Fermentation: Used as a phosphate and potassium nutrient source in fermentation media and laboratory processes.
- Industrial Processing: Supports pH control, formulation stability, and chemical processing where reliable phosphate functionality is required.
Its high water solubility and dependable buffering performance enable efficient incorporation into formulations, while its dual contribution of potassium and phosphate can reduce the need for separate functional ingredients in selected applications.
4. Competitive Advantages
- Quality Consistency: Controlled chemical composition and consistent physical characteristics support repeatable production results.
- Supply Reliability: Structured sourcing supports dependable availability for recurring industrial and bulk requirements.
- Logistics Capability: Suitable for palletized, containerized, and bulk international shipments, supporting efficient global procurement.
- Price Competitiveness: Bulk sourcing and scalable supply programs can provide cost advantages for commercial and industrial buyers.
- Operational Efficiency: High solubility and multifunctional performance simplify formulation and processing requirements.
- Sustainability Considerations: Efficient use of a multifunctional phosphate ingredient can help optimize material consumption within appropriate formulations.
- Technical Documentation: Product specifications, certificates of analysis, safety documentation, and other technical information can be provided according to grade and buyer requirements.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20 MT
- Loading Capacity: Approximately 20–25 MT per 20-foot container, subject to packaging configuration, product density, and applicable container weight limits
- Supply Format: Bulk commercial supply for manufacturers, distributors, formulators, and industrial procurement programs
- International Supply: Export-oriented supply available subject to destination, specifications, packaging, and logistics requirements


Reviews
There are no reviews yet.