
1. Product Overview
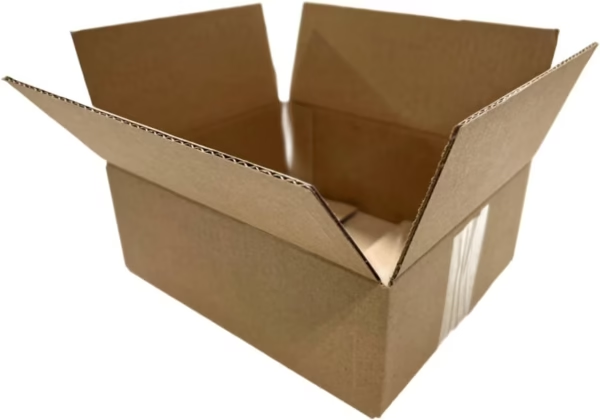
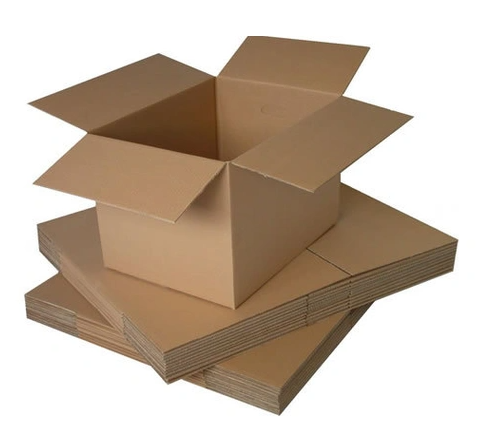
Corrugated Carton Boxes are durable, lightweight packaging solutions manufactured from structured corrugated paperboard for the secure handling, storage, and transportation of goods. They are widely used across manufacturing, retail, e-commerce, food, agriculture, logistics, and industrial supply chains. Their high strength-to-weight ratio provides reliable product protection while optimizing storage, handling, and transportation costs. Strategically, they offer scalable, customizable packaging that supports efficient global distribution and sustainable supply-chain operations.
2. Key Specifications & Technical Characteristics
- Material Composition: Corrugated paperboard comprising kraft or recycled linerboard with a fluted paper medium.
- Grade: Available in single-wall, double-wall, and heavy-duty multi-wall configurations.
- Physical Characteristics: Rigid, lightweight, stackable cartons with strong compression and impact resistance.
- Color: Typically natural kraft brown or white; custom printing and finishes available.
- Dimensions: Customizable length, width, and height according to product and loading requirements.
- Printing: Flexographic, offset-laminated, and customized branding options available.
- Packaging Options: Flat-packed bundles, strapped packs, or palletized shipments.
- Shelf Life: Store in a clean, dry environment away from excessive moisture and direct exposure to water.
3. Core Industrial Applications
- E-Commerce & Retail: Product shipping, order fulfillment, and consumer packaging.
- Food & Agriculture: Packaging for processed foods, produce, and agricultural products where suitable grades are specified.
- Manufacturing: Component, spare-part, machinery, and finished-product packaging.
- Logistics & Distribution: Transit packaging designed for stacking, handling, warehousing, and long-distance transportation.
- Industrial Supply Chains: Protection of products against abrasion, impact, and handling damage.
- Performance Advantage: Corrugated construction delivers dependable cushioning and compression strength while remaining lighter and more cost-efficient than many rigid packaging alternatives.
4. Competitive Advantages
- Quality Consistency: Controlled board construction and dimensional specifications support reliable packaging performance.
- Supply Reliability: Suitable for recurring bulk procurement and structured industrial supply programs.
- Logistics Capability: Flat-pack design maximizes warehouse utilization and shipping efficiency.
- Price Competitiveness: Lightweight construction helps reduce packaging, handling, and transportation costs.
- Sustainability: Paper-based construction can support recyclable and resource-efficient packaging strategies, subject to local recycling requirements and material specifications.
- Customization: Available in multiple sizes, wall constructions, printing formats, and performance grades.
- Technical Documentation: Product specifications, packaging details, and commercial documentation can be provided upon request.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20 MT
- Loading Capacity: Approximately 20–25 MT per 20-foot container, subject to carton dimensions, board specifications, packing method, and applicable container payload limits.



Reviews
There are no reviews yet.