

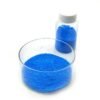
1. Product Overview
Copper Sulfate Pentahydrate 98–99% is a high-purity inorganic copper salt supplied in mining flotation grade for mineral processing applications. It is primarily used as an activator in the flotation of sulfide ores, particularly where controlled copper ion availability is required to improve mineral recovery and selectivity. Its consistent chemical quality supports reliable process performance, helping mining operations optimize recovery efficiency and reagent consumption. As a strategically important flotation reagent, it is widely sourced by mineral processors seeking dependable quality, competitive pricing, and scalable bulk supply.
2. Key Specifications & Technical Characteristics
- Chemical Name: Copper Sulfate Pentahydrate
- Chemical Formula: CuSO₄·5H₂O
- Purity: 98–99% minimum
- Grade: Mining / Flotation Grade
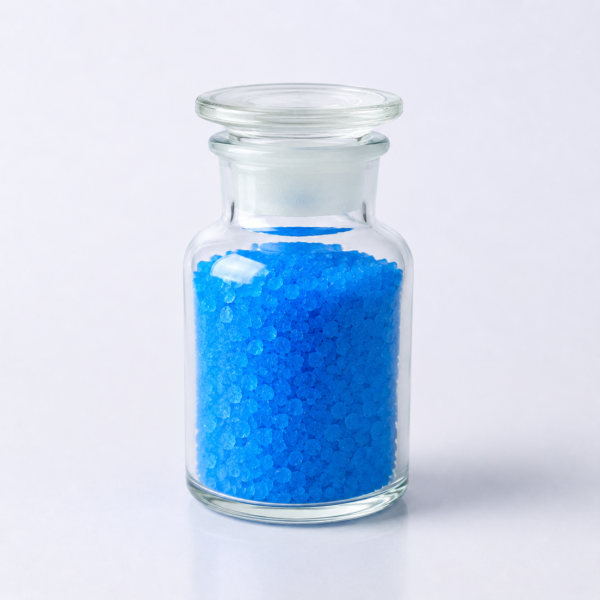
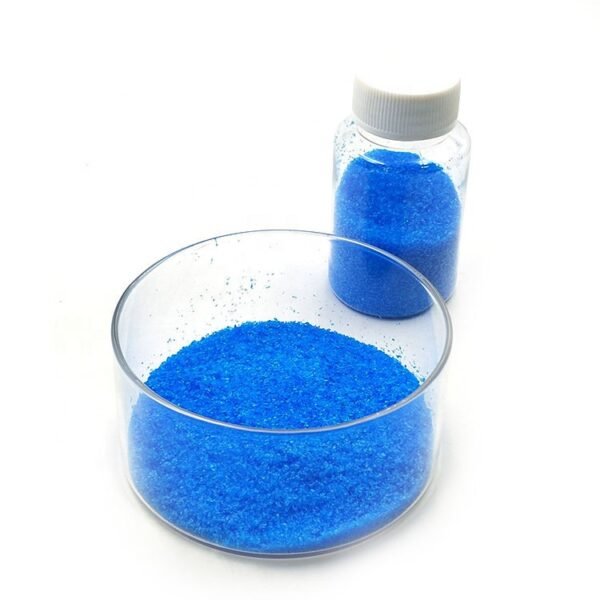
- Appearance: Blue crystalline or granular solid
- Copper Content: Consistent with specified purity and technical grade
- Solubility: Readily soluble in water
- Particle Form: Crystalline, granular, or powder form depending on supply specification
- Packaging Options: 25 kg bags, 50 kg bags, or customized bulk packaging
- Shelf Life: Typically 24 months when stored in a cool, dry, well-ventilated environment in sealed packaging
- Storage: Protect from moisture and contamination; keep packaging tightly closed
3. Core Industrial Applications
- Mining & Mineral Processing: Used extensively as an activator in froth flotation circuits for copper, zinc, lead, and other sulfide minerals.
- Flotation Reagent Systems: Improves mineral surface activation and supports more effective interaction with collectors.
- Ore Beneficiation: Helps enhance mineral recovery and concentrate quality when applied under controlled process conditions.
- Process Optimization: Consistent purity enables more predictable reagent dosing and stable flotation performance.
- Commercial Advantage: Its high solubility and controlled composition support efficient preparation, dosing, and integration into industrial flotation systems.
4. Competitive Advantages
- High Purity & Consistency: 98–99% specification supports dependable performance across industrial processing operations.
- Reliable Supply: Suitable for recurring bulk procurement and large-scale mining requirements.
- Logistics Capability: Available in export-oriented packaging and bulk shipment configurations to support international supply chains.
- Price Competitiveness: Bulk sourcing provides opportunities for cost-efficient procurement and optimized reagent expenditure.
- Process Efficiency: Effective activation performance can contribute to improved mineral recovery and controlled reagent consumption.
- Technical Documentation: Product specifications and quality documentation can be provided to support buyer qualification, quality control, and procurement requirements.
- Strategic Sourcing: Combines consistent quality, scalable availability, and commercial flexibility for mining companies and mineral-processing operations.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Approximately 20–25 MT per 20-ft container, subject to packaging configuration, product density, and applicable shipping limits



Reviews
There are no reviews yet.