


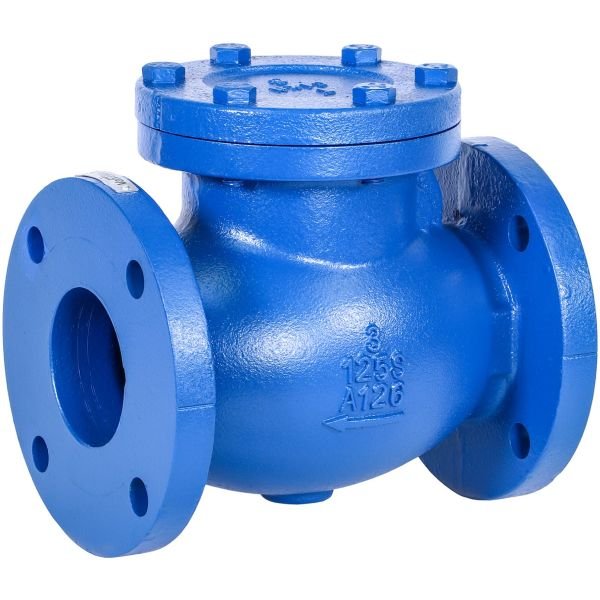


1. Product Overview
Check Valve is a precision-engineered flow-control component designed to permit fluid or gas flow in one direction while automatically preventing reverse flow. It is widely used across industrial piping, water treatment, oil & gas, chemical processing, power generation, and manufacturing systems to protect pumps, compressors, pipelines, and process equipment. Its dependable non-return function helps reduce backflow, pressure-related damage, contamination, and unplanned maintenance. Strategically, it provides an essential safeguard for efficient, reliable, and continuous fluid-handling operations.
2. Key Specifications & Technical Characteristics
- Material Components: Available in industrial-grade stainless steel, carbon steel, cast iron, ductile iron, brass, or other specified alloys depending on application and service conditions.
- Valve Type: Automatic non-return/check valve designed for one-directional flow control.
- Pressure Rating: Available in multiple pressure classes to suit low-, medium-, and high-pressure systems.
- Temperature Range: Configurable according to valve material, seal type, and operating medium.
- Connection Options: Flanged, threaded, wafer, lug, or other industry-standard connections.
- Sealing Components: Industrial-grade elastomers, PTFE, metal-to-metal, or application-specific sealing systems.
- Physical Characteristics: Robust mechanical construction with corrosion-resistant and wear-resistant options available.
- Size Range: Available in multiple nominal diameters to meet diverse industrial piping requirements.
- Packaging: Export-grade protective packaging, pallets, cartons, crates, or customized bulk packaging.
- Documentation: Technical specifications, inspection documentation, certificates, and compliance documents available according to order requirements.
- Shelf Life: Long-term service life when properly stored, installed, operated, and maintained.
3. Core Industrial Applications
- Water & Wastewater Treatment: Prevents reverse flow in pumping, filtration, and distribution systems.
- Oil & Gas: Protects pipelines, pumps, compressors, and process equipment from backflow and pressure surges.
- Chemical Processing: Maintains controlled fluid direction and helps prevent cross-contamination between process lines.
- Power Generation: Supports reliable operation of cooling-water, feedwater, steam, and auxiliary systems.
- Manufacturing & Industrial Processing: Used in compressed-air, hydraulic, process-fluid, and utility piping systems.
- Construction & Plumbing: Provides dependable non-return protection in commercial, industrial, and infrastructure installations.
- Marine & General Engineering: Suitable for demanding fluid-handling applications requiring durable flow-control components.
Its automatic operation eliminates the need for manual intervention, while robust construction and application-specific material options provide dependable performance, reduced maintenance requirements, and protection of critical equipment.
4. Competitive Advantages
- Quality Consistency: Manufactured to defined industrial specifications for reliable dimensional accuracy and operating performance.
- Supply Reliability: Suitable for recurring B2B procurement and bulk industrial requirements.
- Logistics Capability: Export-oriented packaging and supply coordination support international shipment and project-based procurement.
- Price Competitiveness: Competitive bulk sourcing provides opportunities for cost-efficient procurement without compromising essential performance requirements.
- Durability: High-quality material and sealing options support extended service life under demanding operating conditions.
- Application Flexibility: Multiple sizes, materials, pressure ratings, and connection configurations can be supplied to match different systems.
- Technical Support: Product specifications, technical documentation, inspection requirements, and application information can be provided according to buyer needs.
- Strategic Sourcing Value: A dependable check valve supply helps buyers protect critical assets, reduce operational interruptions, and improve overall piping-system reliability.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Approximately 20–25 MT per 20-foot container, subject to valve size, configuration, packaging, and applicable container weight restrictions.
- Supply: Bulk and project-based orders available.
- Packaging: Export-standard packaging suitable for international transportation.
- Delivery: International supply and logistics coordination available.



Reviews
There are no reviews yet.