
1. Product Overview
Aspartame 99% is a high-purity, intense artificial sweetener widely used to provide sweetness in food, beverage, pharmaceutical, and tabletop sweetener formulations. Its high sweetness intensity enables manufacturers to achieve desired sweetness levels with relatively low usage rates, supporting formulation efficiency and cost control. The 25kg bag format is suitable for commercial-scale manufacturing, ingredient blending, and wholesale distribution. Consistent quality and high purity make it a valuable ingredient for industrial buyers seeking reliable sweetening performance.
2. Key Specifications & Technical Characteristics
- Product: Aspartame 99%
- Chemical composition: Aspartame (L-aspartyl-L-phenylalanine methyl ester)
- Purity: 99%
- Grade: Food Grade
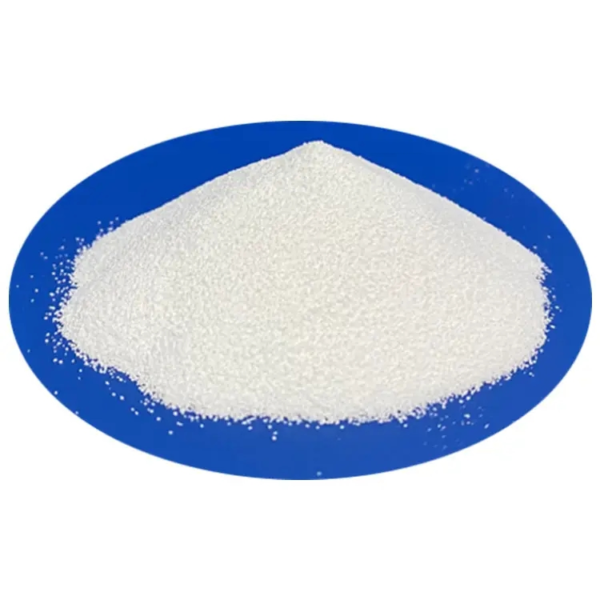
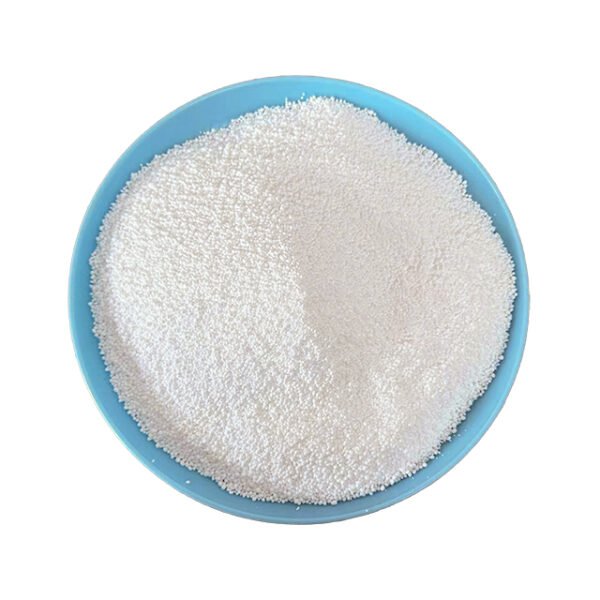
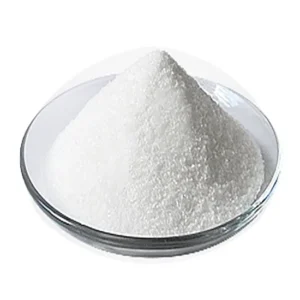
- Physical form: Fine crystalline powder
- Appearance: White to off-white
- Taste profile: High-intensity sweet taste
- Solubility: Suitable for controlled incorporation into formulated food and beverage systems
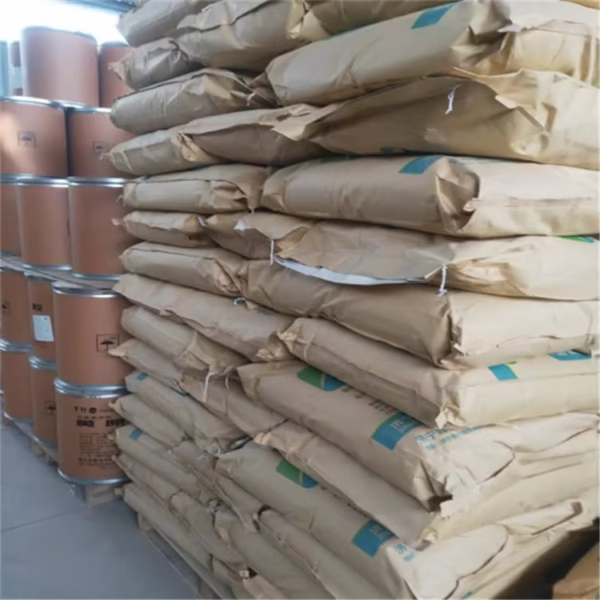
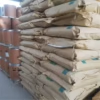
- Packaging: 25kg industrial bag
- Shelf life: Typically 24 months when stored under recommended conditions
- Storage: Keep tightly sealed in a cool, dry environment away from excessive heat, moisture, and direct sunlight
- Origin: Subject to supplier availability and batch documentation
3. Core Industrial Applications
- Food & Beverage: Soft drinks, powdered beverages, desserts, confectionery, chewing gum, and reduced-sugar formulations.
- Pharmaceuticals: Sweetening agent for oral medicines, nutritional products, and other formulations requiring taste masking.
- Tabletop Sweeteners: Used in low-calorie and reduced-sugar sweetener blends.
- Dairy & Dessert Products: Suitable for selected yogurts, instant desserts, and formulated dairy applications.
- Industrial Formulation: Provides high sweetness intensity at low inclusion rates, helping manufacturers manage ingredient usage and formulation costs.
4. Competitive Advantages
- High Purity: 99% specification supports consistent formulation performance.
- Quality Consistency: Suitable for standardized industrial production and repeat procurement.
- Supply Reliability: Bulk packaging supports regular manufacturing and wholesale requirements.
- Logistics Capability: 25kg bags are practical for palletized storage, containerized shipping, and international distribution.
- Price Competitiveness: High sweetness intensity can reduce required inclusion quantities compared with conventional sugar.
- Technical Documentation: Product specifications and quality documentation can be provided subject to supplier and batch availability.
- Strategic Sourcing: Appropriate for food, beverage, pharmaceutical, and ingredient distributors seeking dependable bulk sweetener supply.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Packaging: 25kg bags
- Loading Capacity: Approximately 20–25 MT per 20ft container, subject to packaging configuration, palletization, and applicable container weight limits
- Supply: Bulk and recurring supply available subject to production and shipment schedules
Reviews
There are no reviews yet.