
1. Product Overview
Ascorbic Acid 99% is a high-purity vitamin C ingredient supplied in 25kg bags for food, beverage, pharmaceutical, nutritional, and industrial applications. Its strong antioxidant properties support product stability, formulation performance, and quality preservation across diverse manufacturing processes. The 99% purity specification provides consistent performance for manufacturers requiring dependable, high-grade raw material. As a globally traded commodity, it is strategically important for reliable sourcing of vitamin C across food, health, and industrial supply chains.
2. Key Specifications & Technical Characteristics
- Chemical composition: Ascorbic Acid (Vitamin C), C₆H₈O₆
- Purity: 99% minimum
- Grade: High-purity industrial/food-grade specification, subject to applicable documentation
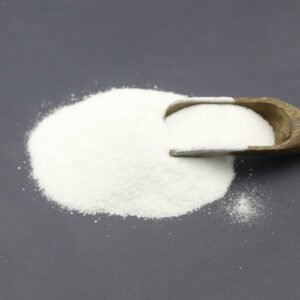
- Physical form: Fine crystalline powder
- Color: White to slightly yellowish-white
- Solubility: Freely soluble in water
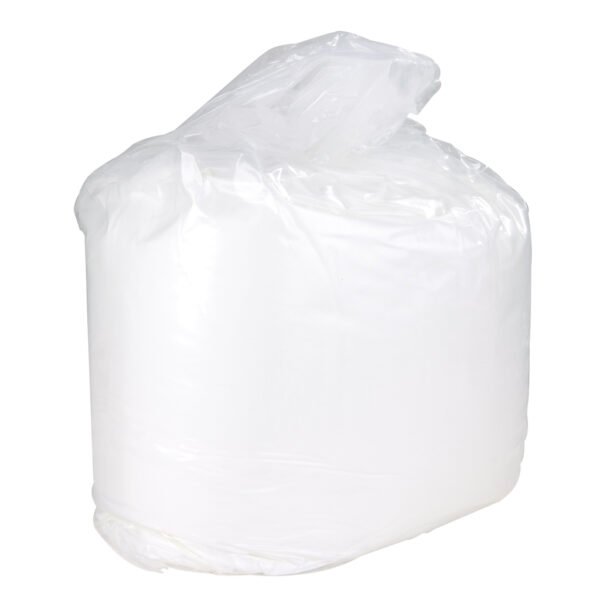
- Packaging: 25kg bag
- Shelf life: Typically 24–36 months when stored under recommended conditions
- Storage: Keep tightly sealed in a cool, dry environment away from heat, moisture, and direct sunlight
- Origin: Available subject to supplier and production batch
- Documentation: COA and relevant technical/specification documentation available upon request
3. Core Industrial Applications
- Food & Beverage: Used as an antioxidant and nutritional ingredient in beverages, processed foods, fruit preparations, and other formulations.
- Pharmaceuticals & Nutraceuticals: Used as an active vitamin ingredient in tablets, powders, capsules, and nutritional formulations.
- Animal Nutrition: Incorporated into feed and premix formulations where vitamin C supplementation is required.
- Food Processing: Supports oxidation control and helps maintain product quality during processing and storage.
- Industrial Formulation: Suitable for manufacturers requiring a consistent high-purity antioxidant raw material.
Its high purity, strong antioxidant functionality, and water solubility make it a versatile choice for manufacturers seeking reliable formulation performance and efficient bulk processing.
4. Competitive Advantages
- Consistent Quality: 99% purity specification supports dependable batch-to-batch formulation performance.
- Supply Reliability: Structured bulk sourcing supports recurring industrial procurement requirements.
- Logistics Capability: 25kg bag packaging facilitates handling, warehousing, container loading, and international distribution.
- Price Competitiveness: Bulk procurement options can support cost-efficient sourcing for commercial-scale users.
- Sustainability: Efficient bulk packaging and consolidated international shipments can help optimize transportation and material handling.
- Technical Documentation: COA and relevant product documentation can support quality assurance, procurement, and regulatory review.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Approximately 20–25 MT per 20ft container, subject to packaging configuration, container payload limits, and final logistics requirements
- Packaging: 25kg bags
- Supply: Bulk international B2B supply

Reviews
There are no reviews yet.