




1. Product Overview
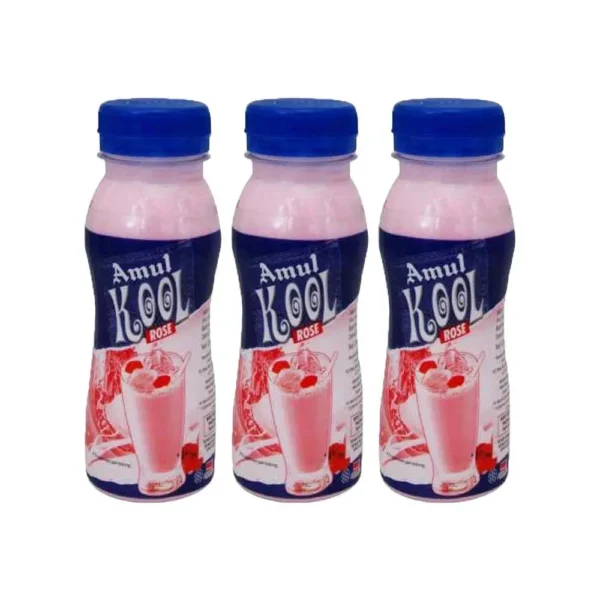
Amul Kool Rose Milk – 200 ml is a ready-to-drink, rose-flavoured milk beverage designed for convenient retail, foodservice, hospitality, and institutional distribution. It combines milk with a distinctive rose flavour profile to provide a convenient chilled or ambient beverage option, subject to the product’s specified storage conditions. Its compact single-serve format supports portion control, merchandising, and high-volume distribution. The product is commercially relevant for wholesalers and distributors seeking established branded beverage products with broad consumer appeal.
2. Key Specifications & Technical Characteristics
- Product Type: Ready-to-drink flavoured milk beverage
- Flavour: Rose
- Net Volume: 200 ml
- Base Material: Milk-based beverage with permitted ingredients and rose flavouring
- Form: Liquid
- Colour: Characteristic rose/pink colour
- Packaging: Individual 200 ml retail-ready packs
- Grade: Consumer food/beverage grade
- Shelf Life: As specified by the manufacturer and printed on the individual packaging
- Origin: India
- Storage: Store according to the manufacturer’s stated storage instructions
- Documentation: Product specifications, batch details, and food-compliance documentation subject to supplier availability
3. Core Industrial Applications
- Wholesale & Distribution: Suitable for beverage distributors supplying supermarkets, convenience stores, and retail outlets.
- Foodservice & Hospitality: Appropriate for hotels, restaurants, cafés, catering operations, and institutional foodservice.
- Retail Beverage Sales: Convenient single-serve format supports direct consumer merchandising and impulse-purchase channels.
- Institutional Supply: Suitable for offices, schools, events, and other high-volume beverage programmes where individually portioned products are preferred.
- Commercial Advantage: Ready-to-drink convenience reduces preparation requirements while the recognizable rose flavour provides product differentiation within flavoured milk categories.
4. Competitive Advantages
- Quality Consistency: Manufactured as a standardized branded beverage for consistent taste and presentation.
- Supply Reliability: Suitable for organized wholesale procurement and distributor-led replenishment.
- Logistics Capability: Compact 200 ml packaging facilitates case packing, palletization, and commercial distribution.
- Market Appeal: Rose flavour offers a distinctive alternative to conventional milk beverages.
- Commercial Efficiency: Ready-to-drink presentation minimizes handling and preparation at the point of sale.
- Strategic Sourcing: Suitable for wholesalers seeking established packaged beverage products for multi-channel distribution.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Subject to packaging configuration, palletization, container specifications, and final shipping requirements
- Supply Format: Bulk wholesale supply for distributors, retailers, foodservice operators, and institutional buyers
Reviews
There are no reviews yet.