
1. Product Overview
Anhydrous Ammonia Industrial Refrigeration Grade is a high-purity, water-free ammonia supplied in cylinders for industrial refrigeration and process cooling applications. It is widely used in cold storage, food processing, chemical manufacturing, and large-scale refrigeration systems due to its strong thermodynamic performance and efficient heat transfer characteristics. Its high refrigeration efficiency supports lower operating costs and dependable temperature control, making it a strategically important refrigerant for demanding industrial operations.
2. Key Specifications & Technical Characteristics
- Chemical composition: Anhydrous ammonia (NH₃)
- Grade: Industrial Refrigeration Grade
- Purity: Typically ≥99.5%, subject to applicable specification and certificate of analysis
- Physical form: Liquefied gas under pressure
- Appearance: Colorless gas/liquid with characteristic ammonia odor
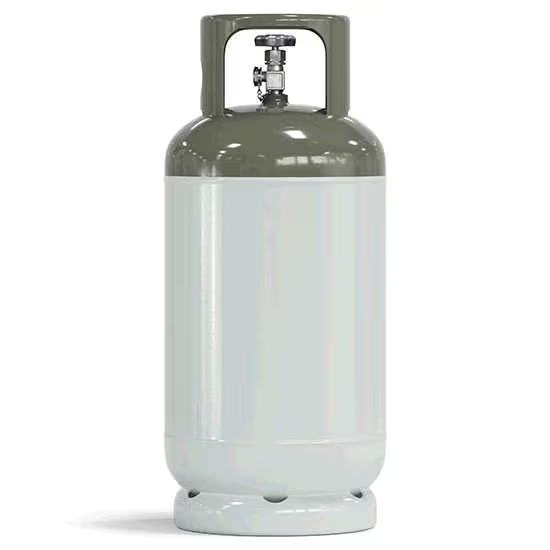
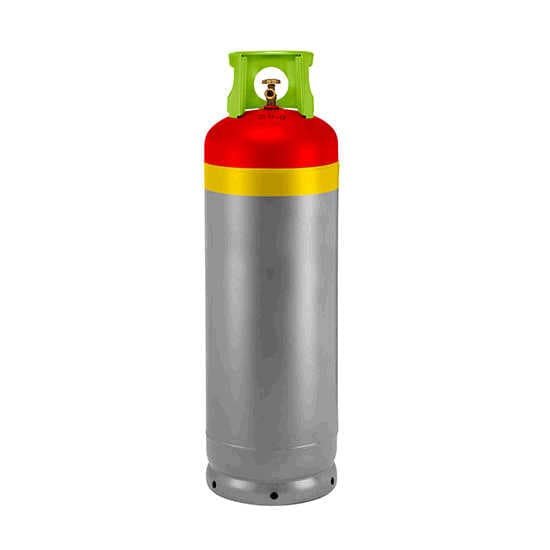
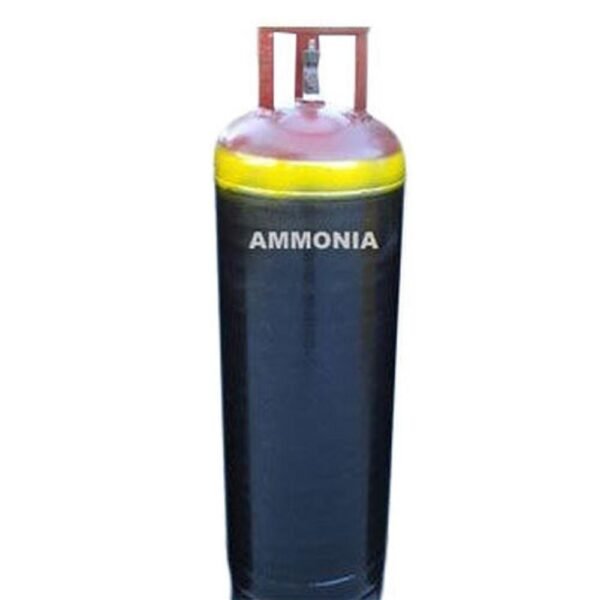
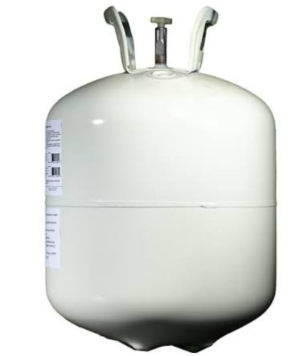
- Packaging: High-pressure certified cylinders; bulk supply options available subject to buyer requirements
- Cylinder sizes: Available in standard industrial capacities according to regional and transport requirements
- Storage: Store in a cool, dry, well-ventilated area away from heat, ignition sources, and incompatible materials
- Documentation: Certificate of Analysis (CoA), Safety Data Sheet (SDS), and relevant compliance documentation available upon request
- Shelf life: Long-term storage is possible when properly contained and maintained under recommended conditions
3. Core Industrial Applications
- Industrial refrigeration: Refrigeration systems for cold storage facilities, warehouses, and distribution centers.
- Food processing: Temperature control and cooling in meat, seafood, dairy, beverage, and other food-processing operations.
- Ice and freezing systems: High-capacity freezing, ice production, and process cooling applications.
- Chemical and manufacturing industries: Process cooling and temperature management where anhydrous ammonia is technically suitable.
- Large-scale refrigeration plants: Particularly effective in centralized systems requiring high refrigeration capacity and energy efficiency.
Ammonia offers excellent thermodynamic efficiency compared with many conventional synthetic refrigerants, supporting high-capacity cooling with efficient system operation.
4. Competitive Advantages
- Quality consistency: Controlled industrial-grade specifications support reliable refrigeration performance and system operation.
- Supply reliability: Suitable for planned bulk procurement and recurring industrial supply programs.
- Logistics capability: Cylinder packaging facilitates controlled handling, transportation, and distribution subject to applicable hazardous-goods regulations.
- Price competitiveness: Efficient refrigeration performance can contribute to favorable total operating economics for large-scale users.
- Sustainability: Ammonia has zero ozone depletion potential and zero global warming potential as a refrigerant, supporting lower-impact refrigeration strategies.
- Technical documentation: SDS, CoA, specifications, and compliance documentation can be provided to support procurement, safety, and regulatory requirements.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20 MT
- Loading Capacity: Up to 20 MT per container, subject to cylinder configuration, applicable transport regulations, and carrier limitations
- Packaging: Certified industrial refrigeration-grade cylinders suitable for controlled commercial distribution
- Supply: Bulk and recurring supply programs available for qualified industrial buyers
- Documentation: Commercial, technical, safety, and compliance documentation available upon request
Reviews
There are no reviews yet.