
1. Product Overview
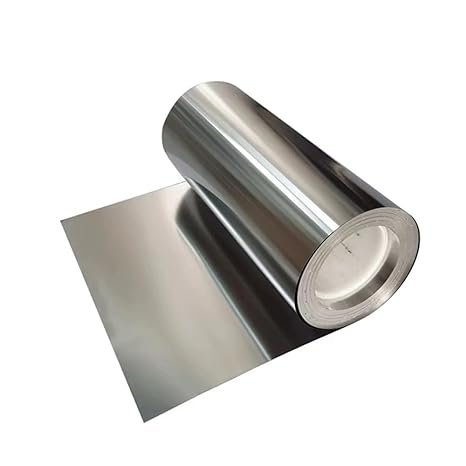
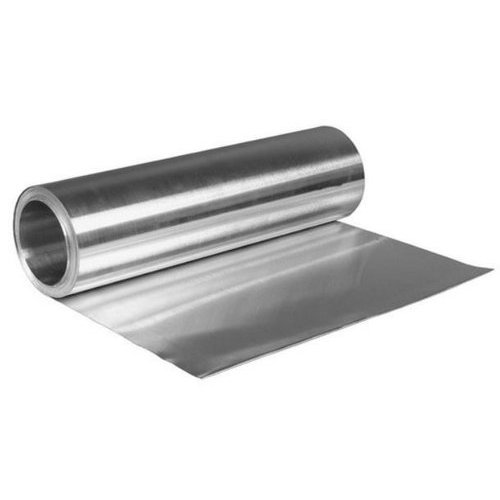
Aluminium Foil is a lightweight, highly versatile aluminium material supplied in thin, flexible sheet form for industrial, commercial, packaging, insulation, and manufacturing applications. Its excellent barrier performance, corrosion resistance, thermal conductivity, and formability make it suitable for protecting products against moisture, light, oxygen, and contamination. The material offers an efficient combination of durability, low weight, and recyclability, supporting cost-effective production across multiple industries. As a globally traded industrial material, aluminium foil remains strategically important for packaging, insulation, electrical, pharmaceutical, food, and consumer-product supply chains.
2. Key Specifications & Technical Characteristics
- Material: Aluminium or aluminium alloy, typically supplied according to application-specific grade requirements
- Composition: Predominantly aluminium with controlled alloying elements where applicable
- Purity: Available in commercial and industrial grades according to buyer specifications
- Form: Thin rolled foil in coils or sheets
- Color: Natural metallic silver
- Surface: Smooth, clean, and uniform; available in mill or application-specific finishes
- Thickness: Customizable according to end-use and technical requirements
- Width: Available in standard or customized widths
- Mechanical Properties: Lightweight, flexible, formable, and tear-resistant according to grade and thickness
- Key Properties: Excellent barrier protection, thermal conductivity, corrosion resistance, reflectivity, and recyclability
- Packaging: Export-grade rolls/coils, pallets, cartons, or customized industrial packaging
- Shelf Life: Long-term when stored in dry, clean conditions and protected from moisture and contamination
3. Core Industrial Applications
- Food & Beverage Packaging: Used for wrapping, lidding, trays, pouches, and barrier packaging to protect contents from light, moisture, oxygen, and contaminants.
- Pharmaceutical Packaging: Used for blister packs, sachets, and protective pharmaceutical packaging where reliable barrier properties are essential.
- Building & Construction: Used in insulation systems, reflective barriers, roofing applications, and thermal protection.
- Electrical & Electronics: Utilized in capacitors, shielding, conductive components, and specialized electrical applications due to its conductivity.
- HVAC & Industrial Insulation: Provides reflective and thermal barrier performance for ducts, pipes, equipment, and insulation systems.
- Consumer & Industrial Manufacturing: Easily formed and processed for various fabricated components, liners, seals, and protective applications.
Its combination of low weight, flexibility, barrier protection, and thermal performance provides practical advantages over heavier or less conductive alternative materials.
4. Competitive Advantages
- Quality Consistency: Controlled thickness, surface quality, dimensional accuracy, and material performance for dependable industrial processing.
- Supply Reliability: Suitable for bulk procurement programs and recurring B2B supply requirements.
- Logistics Capability: Export-oriented packaging and shipment coordination designed to support international delivery.
- Price Competitiveness: Competitive bulk sourcing helps buyers optimize material costs and improve procurement efficiency.
- Sustainability: Aluminium is highly recyclable, supporting circular-material strategies and reduced dependence on virgin resources when recycled content is incorporated.
- Technical Documentation: Product specifications, grade information, packing details, and relevant quality documentation can be provided according to buyer requirements.
- Strategic Sourcing Value: A scalable material solution for manufacturers, distributors, contractors, and industrial buyers seeking dependable international aluminium supply.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20 MT
- Loading Capacity: Typically approximately 20–25 MT per 20-ft container, subject to foil thickness, coil dimensions, packaging configuration, container weight limits, and destination requirements
Reviews
There are no reviews yet.