
1. Product Overview
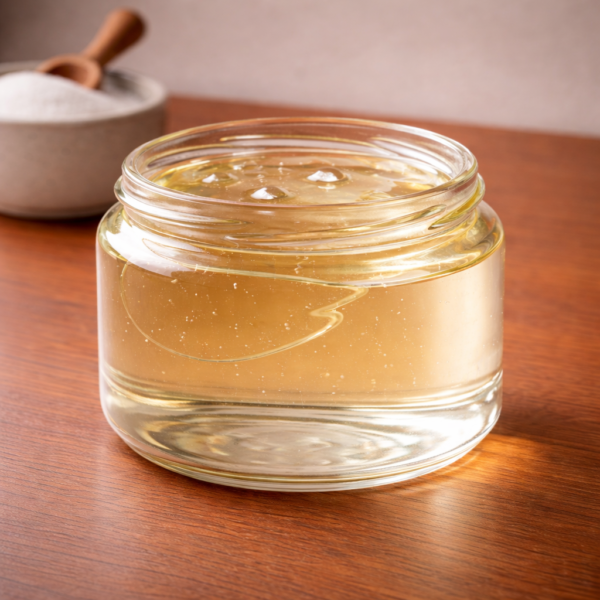
Glucose Syrup is a purified, concentrated aqueous solution of glucose and other saccharides, widely used as a functional sweetener and texturizing ingredient. It is primarily utilized in food, confectionery, bakery, beverage, dairy, and pharmaceutical manufacturing to control sweetness, viscosity, moisture retention, and crystallization. Its consistent performance supports efficient formulation, improved product stability, and dependable large-scale production. As a versatile industrial ingredient, glucose syrup remains strategically important for manufacturers seeking reliable functionality and cost-efficient sweetening solutions.
2. Key Specifications & Technical Characteristics
- Composition: Glucose, maltose, higher saccharides, and water.
- Grade: Food-grade and industrial grades available according to application requirements.
- Appearance: Clear to slightly yellow, viscous liquid.
- Sweetness: Moderate sweetness with strong functional properties.
- Solids Content: Typically supplied in commercially specified DE/solids ranges according to buyer requirements.
- Purity: Consistent quality suitable for industrial food and beverage processing.
- Packaging: Bulk tanker, IBC containers, drums, or other industrial packaging options.
- Shelf Life: Typically 12–24 months when stored under recommended conditions.
- Storage: Store in clean, dry conditions and protect from contamination and extreme temperatures.
3. Core Industrial Applications
- Confectionery: Controls crystallization, improves texture, and provides smooth consistency in candies, toffees, caramels, and fillings.
- Bakery: Enhances moisture retention, browning, texture, and product shelf stability.
- Beverages: Provides controlled sweetness and body in formulated drinks and syrups.
- Dairy & Desserts: Supports texture, solids balance, and consistency in ice cream and dessert products.
- Food Processing: Functions as a sweetener, humectant, bulking agent, and processing aid.
- Pharmaceuticals: Used as a carbohydrate-based excipient and sweetening component in selected formulations.
Compared with crystalline sweeteners alone, glucose syrup offers superior viscosity control, crystallization management, and formulation flexibility, helping manufacturers achieve consistent product characteristics at commercial scale.
4. Competitive Advantages
- Quality Consistency: Controlled specifications support repeatable manufacturing performance.
- Supply Reliability: Structured bulk sourcing supports continuous industrial production requirements.
- Logistics Capability: Bulk and containerized packaging options facilitate efficient international distribution.
- Price Competitiveness: Suitable for high-volume procurement and cost-conscious industrial formulations.
- Sustainability: Efficient bulk packaging and optimized shipment volumes can help reduce packaging and handling requirements.
- Technical Documentation: Product specifications, quality documentation, and relevant certificates can be provided according to order and market requirements.
- Strategic Sourcing Value: A versatile ingredient that combines functional performance, scalable supply, and procurement efficiency.
5. Commercial & Supply Information
- MOQ: BULK 20 MT
- Loading Capacity: Up to 20 MT per container, subject to packaging configuration, container limitations, and destination requirements.
- Supply: Bulk commercial quantities available for international B2B procurement.
Reviews
There are no reviews yet.