
1. Product Overview
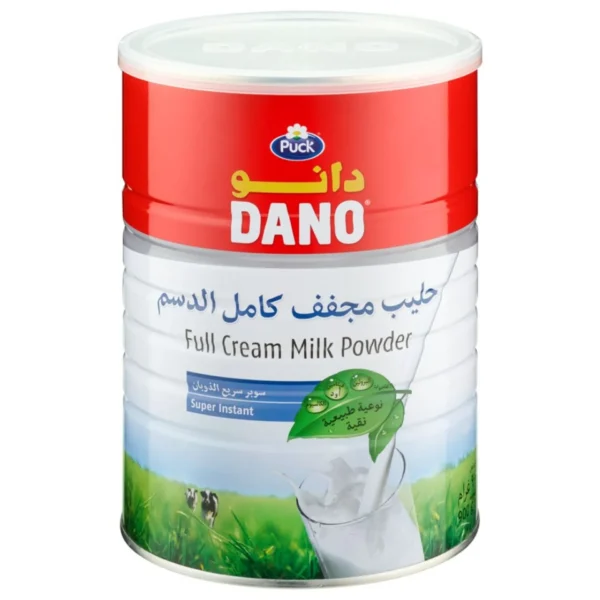
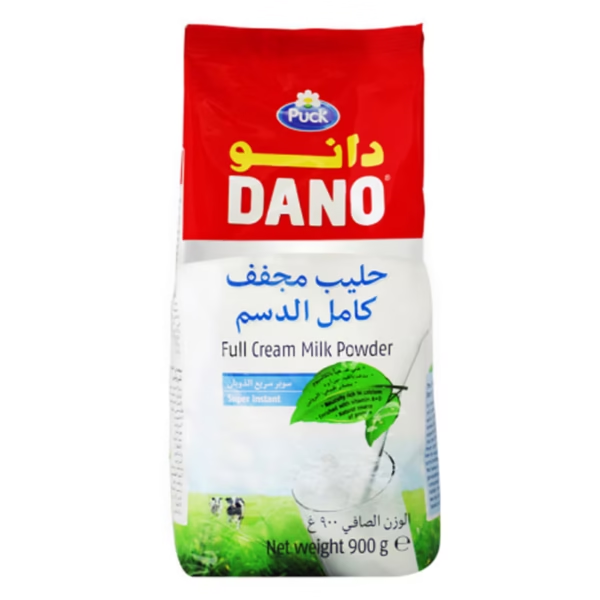
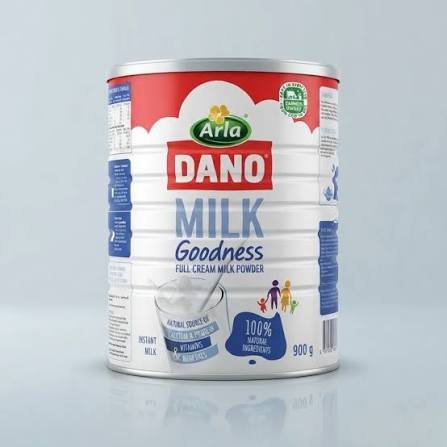
Dano Full Cream Milk Powder — 900g is a premium full-cream dairy powder produced from high-quality milk, offering rich dairy flavor, nutritional value, and convenient long-term storage. It is designed for beverage preparation, food manufacturing, bakery, confectionery, catering, and institutional applications requiring consistent milk solids and creamy taste. Its powder format provides efficient handling, storage, transportation, and reconstitution compared with liquid milk. For commercial buyers, it represents a practical sourcing solution where product consistency, shelf stability, and supply efficiency are essential.
2. Key Specifications & Technical Characteristics
- Product Type: Full Cream Milk Powder
- Primary Composition: Whole milk solids, including milk fat, milk proteins, lactose, and milk minerals
- Grade: Food Grade
- Form: Free-flowing milk powder
- Color: Cream to light creamy-white
- Flavor & Aroma: Characteristic fresh, creamy milk flavor and aroma
- Fat Content: Typically approximately 26% minimum, subject to product specification
- Protein: Naturally occurring dairy protein
- Solubility: Designed for convenient reconstitution in water
- Packaging: 900g retail-format packaging; bulk commercial packaging available subject to supply requirements
- Shelf Life: Typically up to 18–24 months when unopened and stored under recommended conditions
- Storage: Store in a cool, dry environment away from moisture, heat, and direct sunlight
- Origin: Subject to current supplier availability and batch documentation
3. Core Industrial Applications
- Dairy & Beverage Manufacturing: Used to produce reconstituted milk, milk-based beverages, and dairy formulations.
- Bakery & Confectionery: Provides milk solids, creamy flavor, color, and nutritional value in bread, biscuits, cakes, chocolate, and confectionery products.
- Food Processing: Suitable for sauces, desserts, instant mixes, cereals, and other formulated food products.
- Hospitality & Catering: Practical for hotels, restaurants, institutional kitchens, and food-service operations requiring dependable milk supply.
- Industrial Food Formulation: Its concentrated powder format enables efficient storage, transportation, dosing, and inventory management compared with liquid milk.
4. Competitive Advantages
- Quality Consistency: Standardized milk powder format supports consistent formulation and product performance across production batches.
- Supply Reliability: Suitable for structured wholesale procurement and repeat commercial sourcing.
- Logistics Efficiency: Powdered format significantly reduces the handling and transportation challenges associated with liquid milk.
- Commercial Value: Extended shelf life and concentrated milk solids can reduce storage complexity and supply frequency.
- Versatility: Suitable across beverage, bakery, confectionery, food-service, and broader food-processing applications.
- Documentation: Product specifications, batch information, certificates, and other commercial documentation can be provided subject to supplier availability.
- Strategic Sourcing: A shelf-stable dairy ingredient that supports dependable production planning and international B2B procurement.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Approximately 20–25 MT per 20-foot container, subject to packaging configuration, container payload limits, and final loading specifications
Reviews
There are no reviews yet.