
1. Product Overview
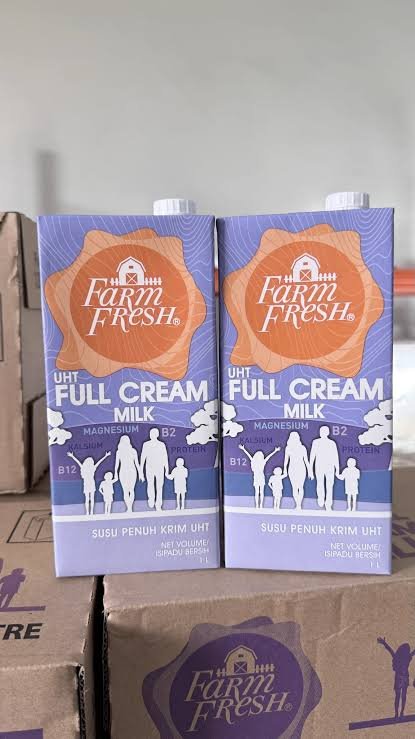
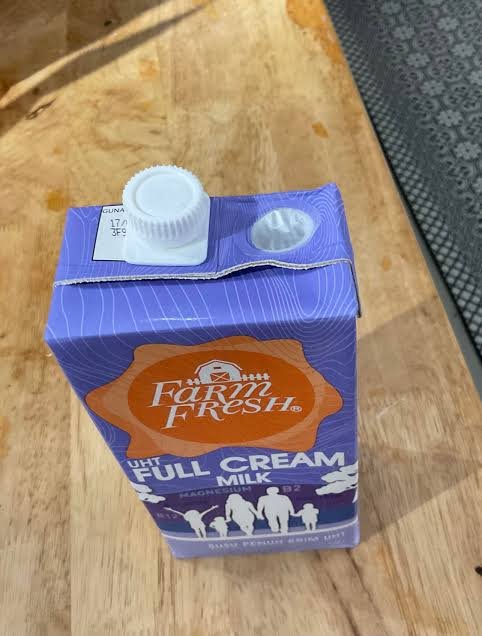
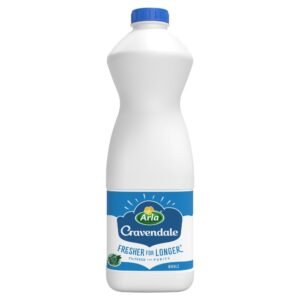
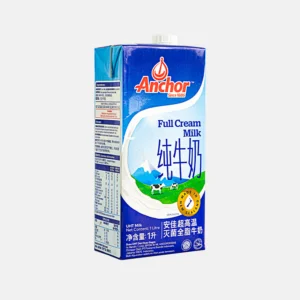
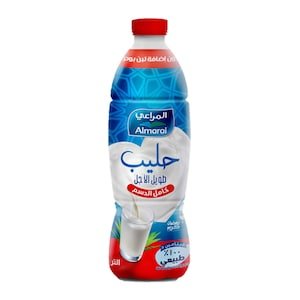
Farm Fresh Full Cream Milk — 1L is a rich, creamy dairy milk formulated to deliver consistent nutritional value, taste, and functionality across foodservice, retail, hospitality, and food-processing applications. Its full-fat profile makes it suitable for direct consumption as well as beverages, bakery, confectionery, desserts, sauces, and other dairy-based formulations. The product provides dependable quality and convenient 1L packaging for efficient handling, distribution, and inventory management. As a high-demand everyday dairy commodity, it represents a commercially attractive sourcing option for wholesalers, distributors, retailers, and institutional buyers.
2. Key Specifications & Technical Characteristics
- Product Type: Full Cream Milk
- Composition: Cow’s milk; naturally occurring milk fat, milk proteins, lactose, minerals, and water
- Fat Content: Typically approximately 3–4% milk fat, subject to product specification
- Grade: Food Grade
- Physical Form: Homogeneous liquid
- Colour: White to creamy white
- Texture: Smooth, creamy, and uniform
- Taste & Aroma: Fresh, characteristic dairy flavour and aroma
- Packaging: 1L retail-ready packs; outer carton configurations available according to supply specification
- Shelf Life: Subject to processing method, packaging, storage conditions, and manufacturer specification
- Storage: Store under the temperature conditions specified on the product packaging
- Origin: Available subject to sourcing and supplier specification
- Documentation: Product specifications, certificates, and quality documentation available upon request
3. Core Industrial Applications
- Food & Beverage Manufacturing: Used as an ingredient in dairy beverages, milk-based drinks, desserts, sauces, and prepared foods.
- Bakery & Confectionery: Provides milk solids, creaminess, flavour, and functional properties in breads, cakes, pastries, custards, and confectionery products.
- Hospitality & Foodservice: Suitable for hotels, restaurants, cafés, catering companies, and institutional kitchens.
- Retail & Wholesale Distribution: Convenient 1L packaging supports direct consumer sales and efficient wholesale distribution.
- Dairy-Based Formulations: Full-fat milk delivers a richer mouthfeel and nutritional profile compared with reduced-fat alternatives.
Its combination of nutritional value, familiar consumer acceptance, convenient packaging, and broad application versatility supports efficient procurement across multiple market segments.
4. Competitive Advantages
- Consistent Quality: Standardized full-cream milk specification supports dependable taste, texture, and performance.
- Reliable Supply: Suitable for structured wholesale procurement and recurring commercial requirements.
- Flexible Logistics: 1L retail-ready units simplify handling, warehousing, distribution, and inventory management.
- Market Demand: A high-consumption staple with broad applicability across retail, hospitality, foodservice, and food manufacturing.
- Commercial Competitiveness: Bulk sourcing can support competitive landed costs for distributors and institutional buyers.
- Efficient Distribution: Standardized packaging facilitates palletization, transport, stock management, and downstream resale.
- Quality Documentation: Product specifications and relevant quality documentation can be provided to support commercial and procurement requirements.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20 MT
- Loading Capacity: Approximately 20–24 MT per 40ft container, subject to final packaging configuration, palletization, product specification, and shipping requirements
- Supply Format: Bulk wholesale supply
Reviews
There are no reviews yet.