
1. Product Overview
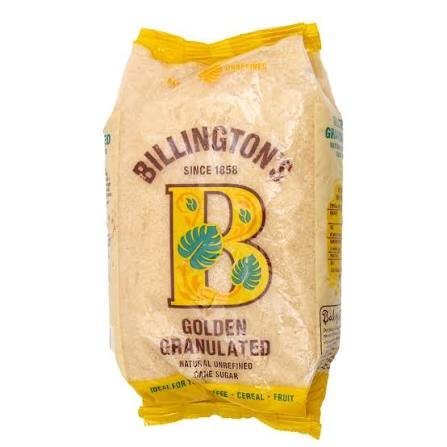
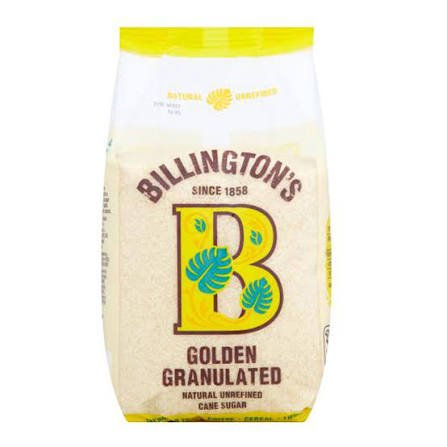
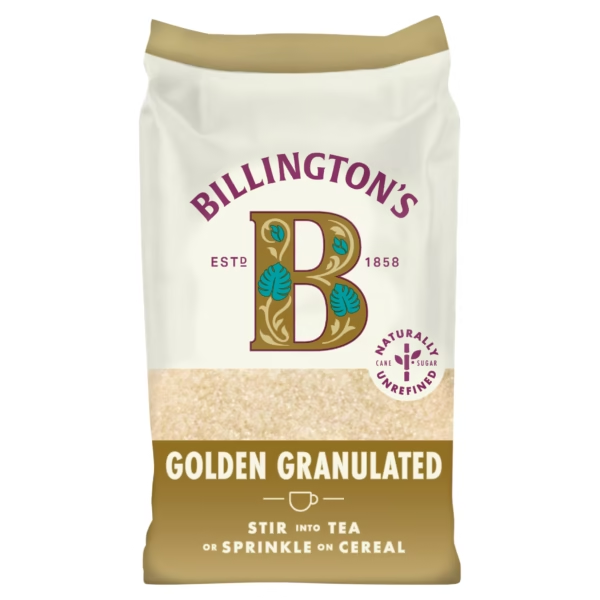
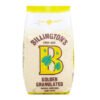
Billington’s Granulated Sugar — 1kg is a premium granulated cane sugar designed for consistent performance across food, beverage, retail, and commercial applications. Its clean sweetness and reliable granulated form make it suitable for baking, confectionery, beverage preparation, food processing, and general sweetening requirements. The product provides dependable quality and ease of handling for buyers seeking an established branded sugar solution. As a widely used staple ingredient, granulated sugar remains strategically important for foodservice, retail, manufacturing, and international wholesale supply chains.
2. Key Specifications & Technical Characteristics
- Product: Billington’s Granulated Sugar
- Primary Component: Sucrose derived from sugar cane
- Grade: Food Grade
- Form: Granulated crystalline sugar
- Colour: Natural golden/brown cane-sugar appearance
- Taste: Clean, naturally sweet sugar profile
- Purity: Food-grade sucrose suitable for human consumption
- Particle Characteristics: Free-flowing granulated crystals suitable for general food processing and preparation
- Packaging: 1kg retail pack
- Shelf Life: Typically up to 24 months when stored under recommended conditions
- Storage: Store in a cool, dry environment away from moisture, heat, and contamination
- Origin: Subject to specific production and supply batch
3. Core Industrial Applications
- Food Manufacturing: Used as a sweetening and formulation ingredient in bakery, confectionery, desserts, sauces, and prepared foods.
- Beverage Production: Suitable for sweetening hot and cold beverages, syrups, mixes, and other drink formulations.
- Bakery & Confectionery: Provides consistent sweetness and supports a wide range of baking and confectionery processes.
- Foodservice & Hospitality: Practical for restaurants, cafés, catering operations, hotels, and institutional kitchens.
- Retail & Wholesale: The 1kg format is suitable for retail distribution and commercial resale.
Its consistent granulated structure supports easy measuring, handling, blending, and dispensing, helping commercial users maintain predictable formulation and production results.
4. Competitive Advantages
- Quality Consistency: Reliable granulated format and food-grade quality for repeat commercial use.
- Established Brand: Billington’s is a recognised sugar brand, supporting buyer confidence and marketability.
- Supply Reliability: Suitable for structured wholesale procurement and repeat purchasing programmes.
- Logistics Capability: Standardised 1kg packaging facilitates handling, storage, palletisation, and distribution.
- Commercial Competitiveness: Supports efficient procurement for retailers, foodservice operators, distributors, and commercial users.
- Versatile Application: Suitable across food manufacturing, beverage preparation, bakery, confectionery, hospitality, and retail channels.
- Documentation: Product and commercial documentation can be provided subject to supplier and shipment requirements.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Approximately 20–24 MT per standard container, subject to packaging configuration, palletisation, and applicable container weight limits
Reviews
There are no reviews yet.