
- Product Overview
Sodium Carbonate (Na₂CO₃), commonly known as soda ash, is a versatile inorganic chemical widely used across major industrial and manufacturing sectors. It serves as a key raw material in glass production, detergents, chemicals, water treatment, pulp and paper, and metallurgical processes. Its strong alkalinity, reliable performance, and broad industrial utility make it an essential input for high-volume manufacturing. Consistent quality and scalable bulk supply support efficient procurement and dependable production planning. - Key Specifications & Technical Characteristics
- Chemical Composition: Sodium Carbonate (Na₂CO₃)
- Typical Purity: ≥99.0% for industrial-grade supply
- Grade: Industrial Grade; other grades available subject to specification
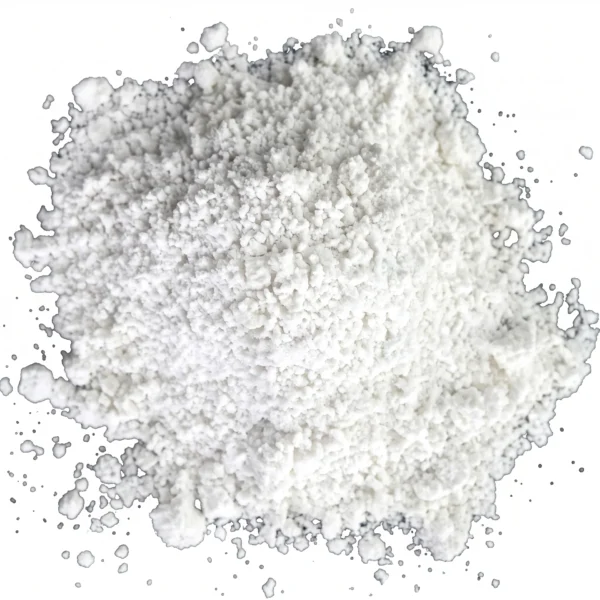
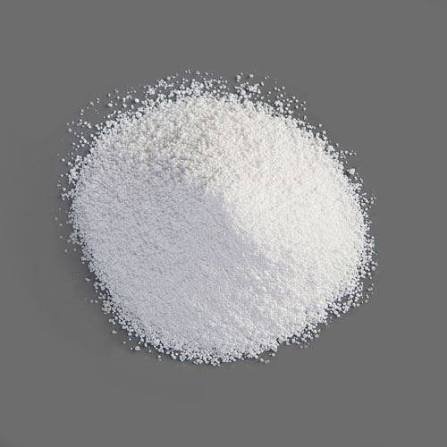
- Physical Form: Free-flowing crystalline powder or granular solid
- Colour: White
- Solubility: Readily soluble in water
- Alkalinity: Strong alkaline chemical properties
- Particle Size: Available in light or dense grades according to application requirements
- Packaging Options: 25 kg bags, 50 kg bags, jumbo bags, and bulk loading
- Shelf Life: Typically 24 months when stored correctly
- Storage: Keep sealed in a cool, dry, well-ventilated environment away from moisture
- Origin: Available from established international manufacturing and supply sources
- Core Industrial Applications
- Glass Manufacturing: Essential fluxing agent for reducing melting temperatures and improving production efficiency.
- Detergents & Cleaning Products: Used as an alkalinity builder, water softener, and cleaning-performance enhancer.
- Chemical Manufacturing: Feedstock for producing sodium-based chemicals, silicates, phosphates, and other industrial compounds.
- Water Treatment: Used for pH adjustment and alkalinity control in industrial and municipal water-treatment processes.
- Pulp & Paper: Supports chemical processing and pH control during manufacturing.
- Metallurgy & Mining: Used in selected mineral-processing and metallurgical operations where controlled alkalinity is required.
- Advantages Over Alternatives: Combines high industrial versatility, effective alkalinity, scalable availability, and cost-efficient performance for high-volume applications.
- Competitive Advantages
- Quality Consistency: Controlled chemical composition and dependable industrial-grade performance.
- Supply Reliability: Suitable for recurring bulk procurement and long-term industrial supply programs.
- Logistics Capability: Available in bulk and container-compatible packaging formats to support international distribution.
- Price Competitiveness: Cost-effective raw material for large-scale manufacturing and processing operations.
- Operational Efficiency: Strong alkalinity and multifunctional performance help optimize industrial processes and material consumption.
- Sustainability: Efficient industrial processing and broad application versatility support optimized resource utilization.
- Technical Documentation: Product specifications, certificates of analysis, safety documentation, and technical information can be provided subject to order requirements.
- Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20 MT
- Loading Capacity: Approximately 20–25 MT per 20-foot container, depending on product density, packaging configuration, and applicable shipping requirements



Reviews
There are no reviews yet.